Complete engineering, fabrication, installation, and commissioning. Comprehensive technical conversion metrics, utilities specifications, and project economics for Biodiesel, Bioethanol, and Compressed Biogas (CBG) & Oil Neutralization installations.
Select technology and input capacity to calculate outputs, utility loads, and CAPEX instantly.
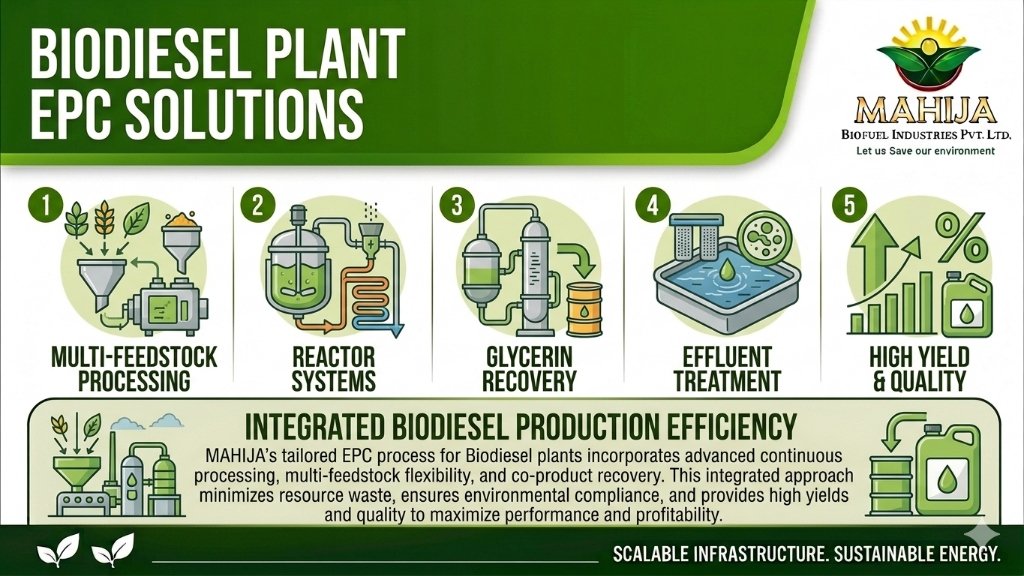
Complete turnkey biodiesel production plants utilizing continuous and semi-continuous multi-feedstock transesterification technology. Engineered for maximum methyl ester yield (>98%) with integrated continuous methanol recovery and crude glycerol separation.
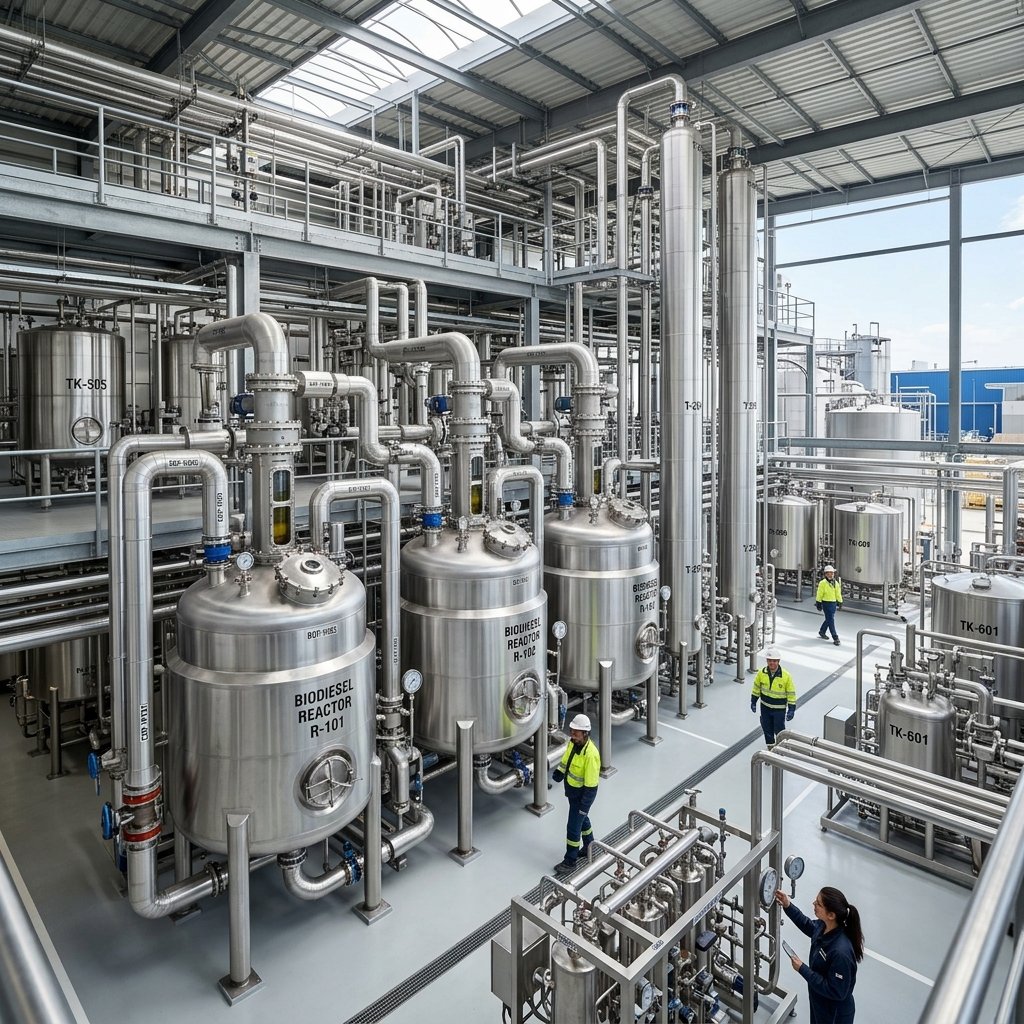
From feasibility analysis and equipment fabrication to site commissioning and OMC off-take.
Our Biodiesel Manufacturing Plants are delivered on a complete turnkey basis — from initial site survey and civil engineering to equipment fabrication, automated controls installation, trial commissioning, and comprehensive operator training.
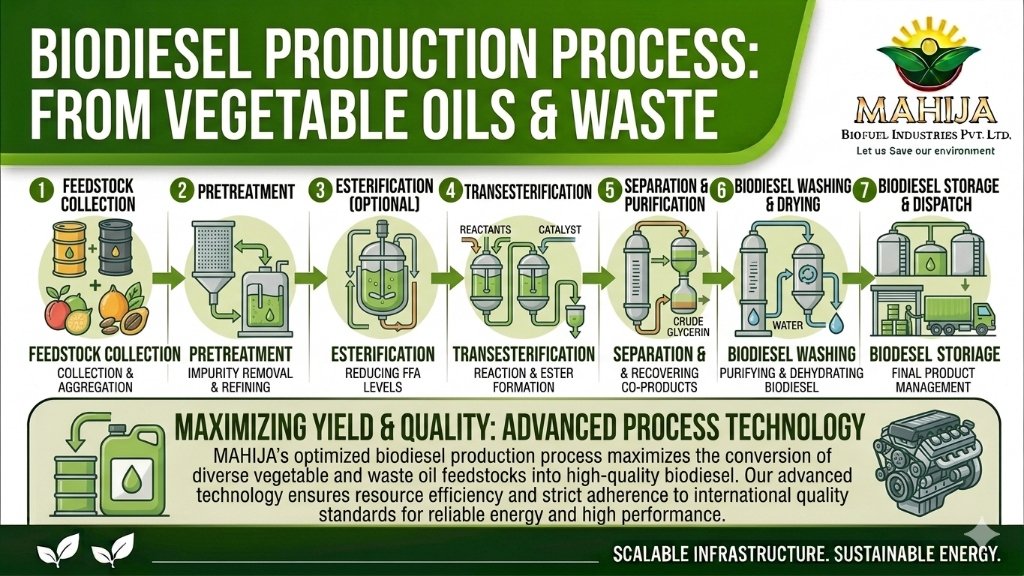
The plant utilizes a flexible two-stage transesterification process with acid esterification pre-treatment for high-FFA feedstocks (handling up to 95% FFA oils seamlessly). An integrated fractional methanol recovery column recycles unreacted alcohol to cut operating expenses, while by-product crude glycerol is concentrated for high commercial recovery.
Multi-feedstock design ensures operational profitability regardless of single-crop seasonal swings:
Capacity selection, feedstock availability assessment, financial viability studies, bankable DPR.
Process Flow Diagrams (PFD), P&ID development, 3D equipment layouts, civil engineering.
Reactors, fractional distillation columns, methanol recovery units, storage tank farms.
On-site piping, instrumentation, electrical wiring, trial production runs, performance audits.
Standard Operating Procedures (SOPs), safety protocols, in-depth technical staff training.
Access to nationwide UCO procurement network, acid oil suppliers, and tallow channels.
Lab setup guidance, GC testing protocols, BIS IS 15607 / ASTM D6751 certification.
Connecting with OMC buyers (IOCL, BPCL, HPCL) under national blending tenders.
Get a comprehensive proposal with capacity sizing, plant layout, ROI model, and turnkey timeline.
Request Technical Proposal Call +917016074249| Particulars | 10 KLPD | 20 KLPD | 30 KLPD | 40 KLPD | 50 KLPD |
|---|---|---|---|---|---|
| Production Capacity | 10 KLPD | 20 KLPD | 30 KLPD | 40 KLPD | 50 KLPD |
| Feedstock | UCO, PFAD, Acid Oil, MFA, High FFA Oils (Up to 95% FFA with Pre-Esterification) | ||||
| Technology | Continuous & Semi-Continuous PLC / SCADA Automated | ||||
| Land Requirement | 1 Acre | 1.5 Acre | 2 Acre | 2.5 Acre | 3 Acre |
| Built-Up Area | 12,000 Sq.ft | 18,000 Sq.ft | 25,000 Sq.ft | 32,000 Sq.ft | 40,000 Sq.ft |
| Connected Power Load | 100 KW | 100 KW | 100 KW | 250 KW | 300 KW |
| Boiler Requirement | 1 TPH | 2 TPH | 3 TPH | 4 TPH | 5 TPH |
| Water Requirement | 10 - 15 KLD | 20 - 25 KLD | 30 - 35 KLD | 40 - 45 KLD | 50 - 60 KLD |
| Manpower Requirement | 10 - 12 | 15 - 18 | 20 - 25 | 25 - 35 | 40 - 45 |
| Plant Operation | 24 Hours Continuous / Semi-Continuous Operation | ||||
| Capacity | Estimated Investment (CAPEX)* | Typical Payback Period* |
|---|---|---|
| 10 KLPD | ₹ 5 Crore Onwards | 3 - 4 Years |
| 20 KLPD | ₹ 9 Crore Onwards | 3 - 4 Years |
| 30 KLPD | ₹ 13 Crore Onwards | 2.5 - 4 Years |
| 40 KLPD | ₹ 17 Crore Onwards | 2.5 - 3.5 Years |
| 50 KLPD | ₹ 21 Crore Onwards | 2.5 - 3.5 Years |
*Note: Indicative CAPEX relates to standard equipment, piping, and controls package. Land, statutory approvals, and civil structures vary by location.
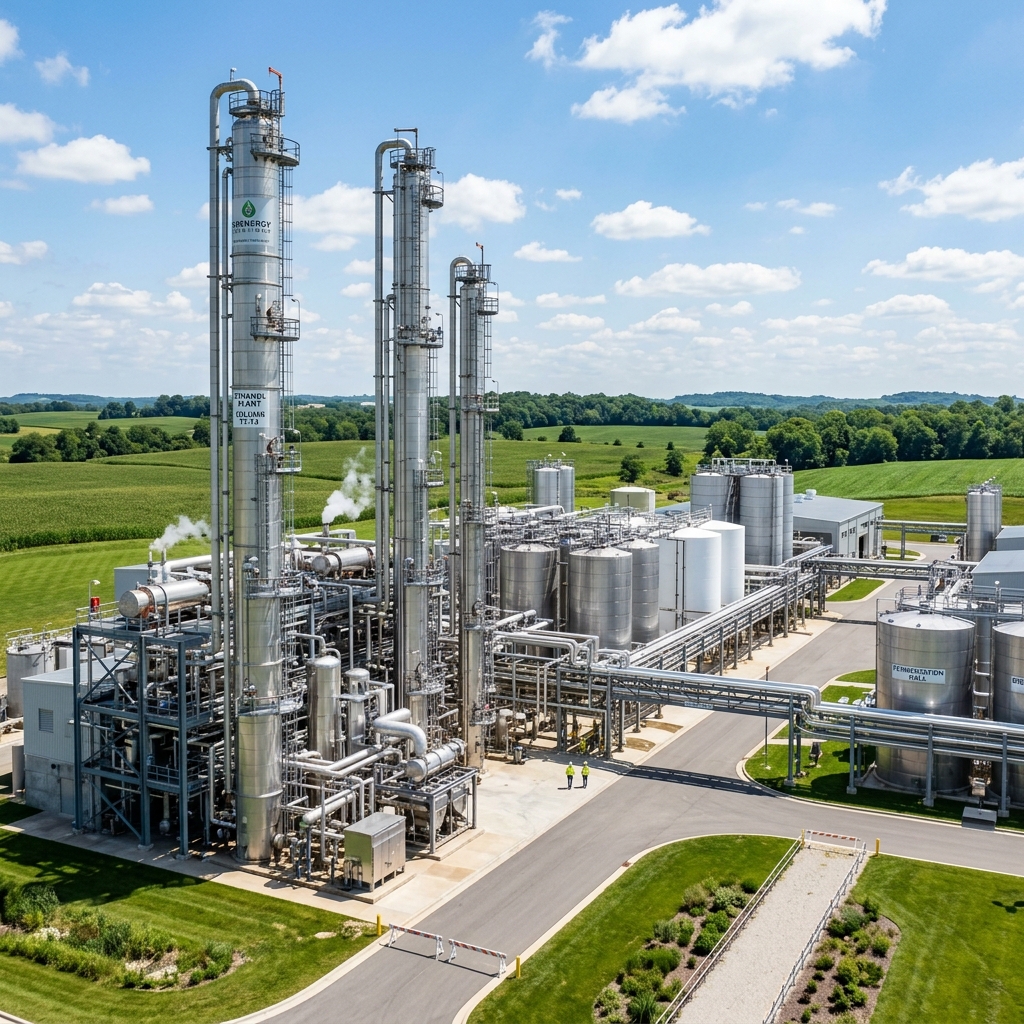
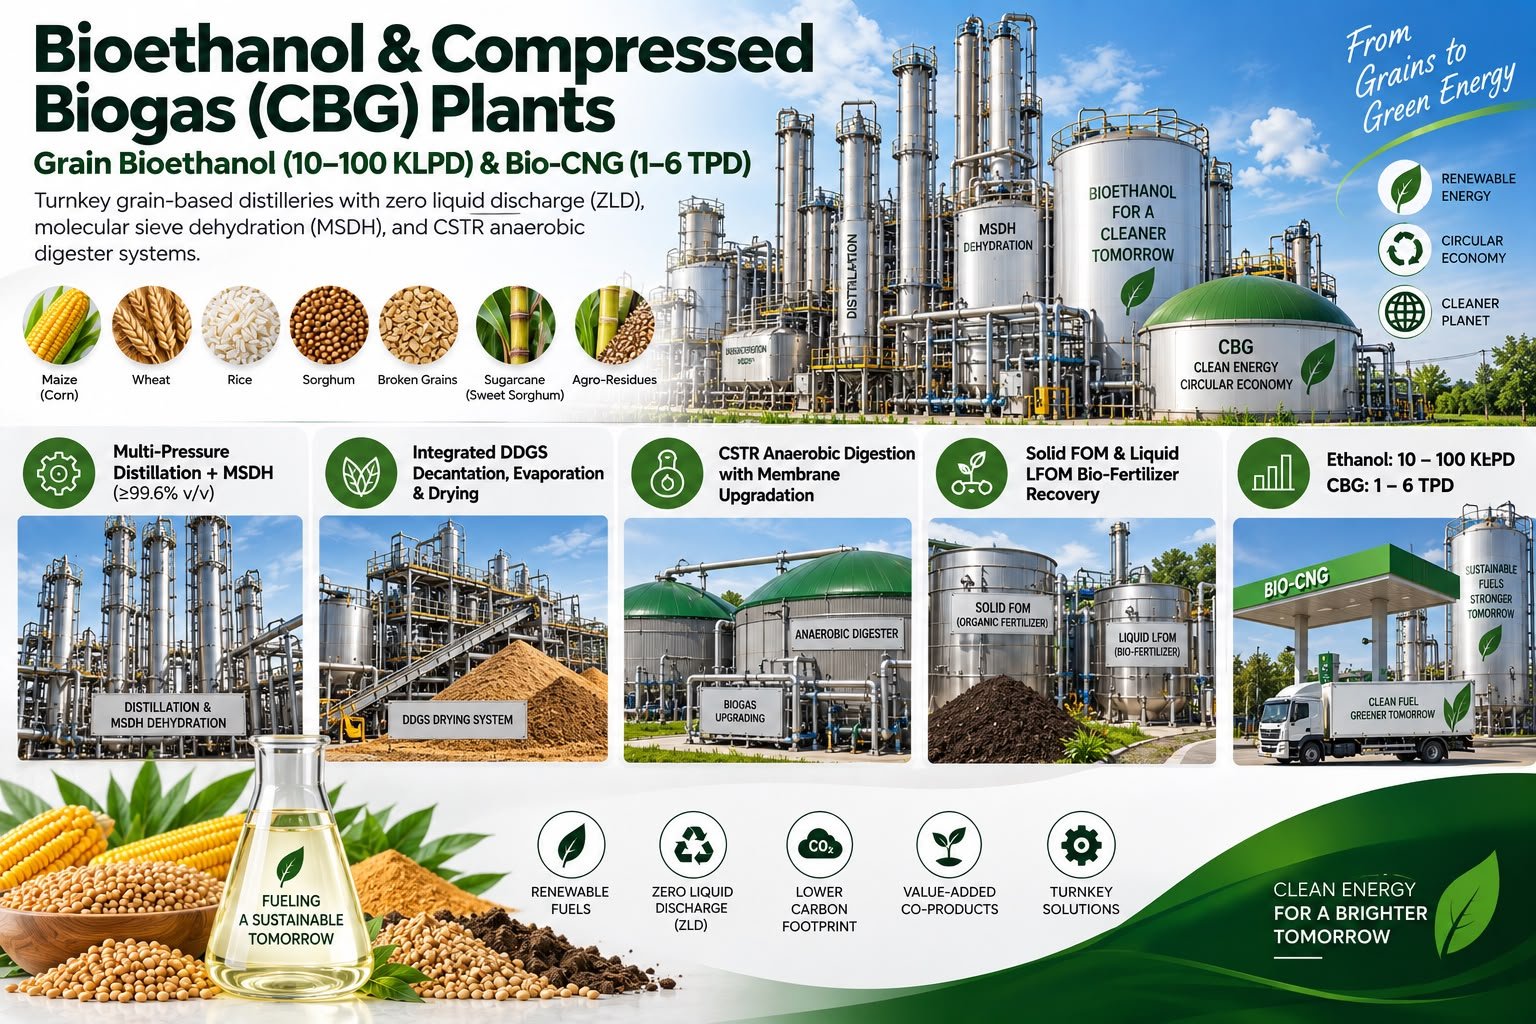
High-efficiency multi-feedstock grain-based and biomass bioethanol plants engineered for maximum volumetric yield with minimum water (Zero Liquid Discharge - ZLD) and low steam consumption.
Fermentation, Molecular Sieve Dehydration (MSDH ≥99.8%), and DDGS Animal Feed recovery.
MAHIJA’s Ethanol Plant solutions are custom-engineered for complete compliance with India’s National Biofuel Policy and Oil Marketing Company (OMC) 20% ethanol blending targets (E20).
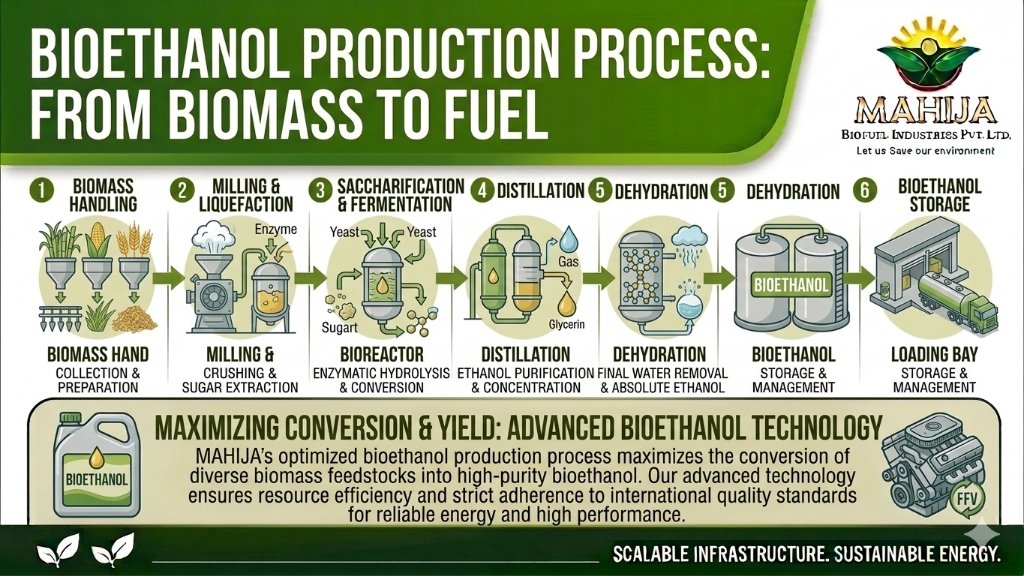
The facility incorporates a continuous liquefaction and saccharification line followed by high-performance yeast fermentation delivering fermentation efficiencies exceeding 92%. Multi-column vacuum distillation coupled with a twin-bed Molecular Sieve Dehydration (MSDH) unit produces anhydrous fuel-grade ethanol with ≥99.8% purity, while decanter centrifuges and integrated dryers recover high-value DDGS protein feed.
Plant configuration allows seamless switching between grain and sugar-based feedstocks:
Receive complete engineering DPR, grain consumption matrix, utility sizing, and turn-key delivery roadmap.
Request Technical Proposal Call +917016074249| Plant Capacity | Corn / Jowar Feedstock (60% Starch) | Broken Rice Feedstock (72% Starch) | ||
|---|---|---|---|---|
| Ethanol Output | Grain Feed (MT/Day) | Ethanol Output | Rice Feed (MT/Day) | |
| 10 KLPD | 10,000 L/Day | 26.5 MT | 10,000 L/Day | 23.0 MT |
| 20 KLPD | 20,000 L/Day | 53.0 MT | 20,000 L/Day | 47.0 MT |
| 30 KLPD | 30,000 L/Day | 80.0 MT | 30,000 L/Day | 70.0 MT |
| 40 KLPD | 40,000 L/Day | 106.0 MT | 40,000 L/Day | 94.0 MT |
| 50 KLPD | 50,000 L/Day | 132.0 MT | 50,000 L/Day | 117.0 MT |
| Capacity | Investment CAPEX | Land Required | Power Connected | Steam Boiler | Water (KLD) | Manpower | Typical Payback |
|---|---|---|---|---|---|---|---|
| 10 KLPD | ₹ 12 - 15 Cr | 2 - 3 Acres | 400 KW | 6 TPH | 120 - 150 | 20 - 25 | 4 - 6 Years |
| 20 KLPD | ₹ 20 - 25 Cr | 3 - 4 Acres | 650 KW | 10 TPH | 250 - 300 | 30 - 35 | 4 - 6 Years |
| 30 KLPD | ₹ 30 - 35 Cr | 4 - 5 Acres | 900 KW | 15 TPH | 350 - 450 | 40 - 50 | 3.5 - 5 Years |
| 40 KLPD | ₹ 40 - 50 Cr | 5 - 6 Acres | 1,200 KW | 20 TPH | 500 - 600 | 55 - 65 | 3 - 5 Years |
| 50 KLPD | ₹ 50 - 65 Cr | 6 - 8 Acres | 1,500 KW | 25 TPH | 650 - 800 | 70 - 80 | 3 - 4.5 Years |
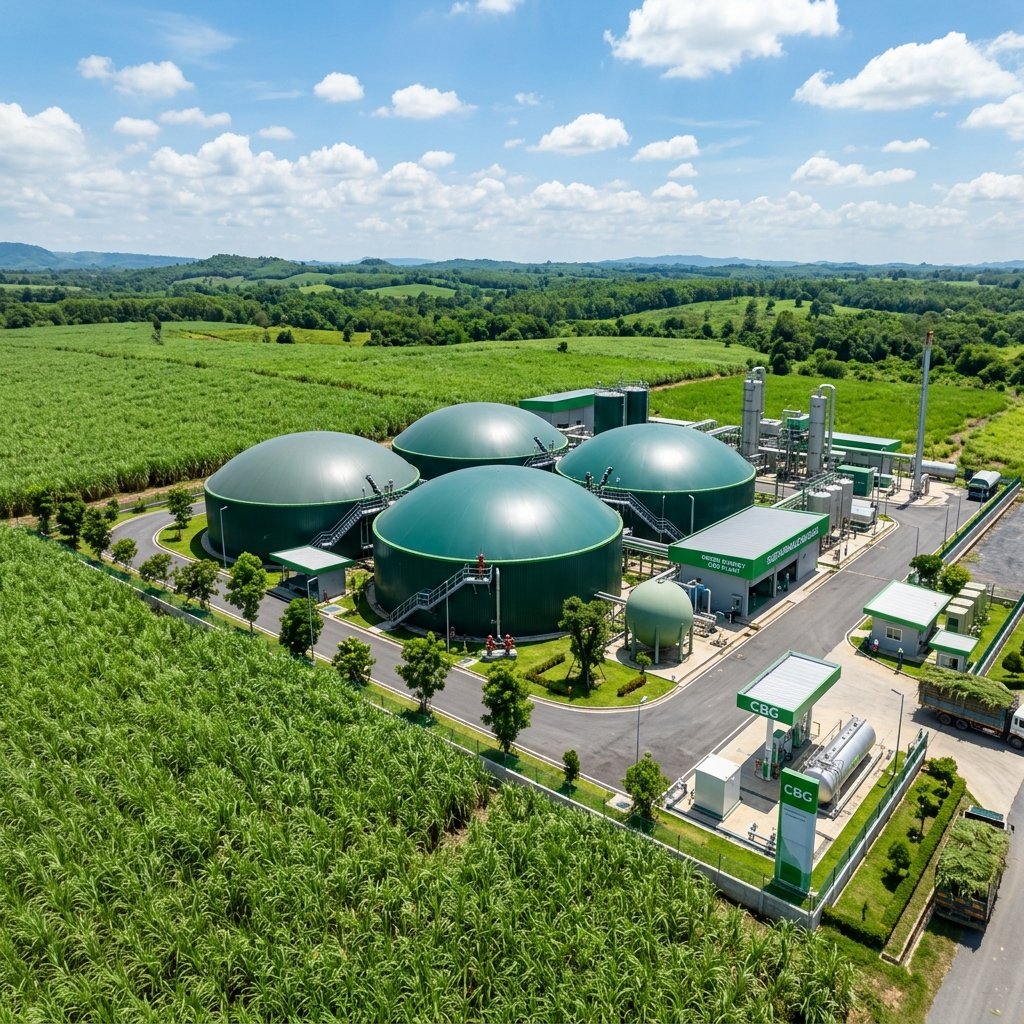
Turnkey renewable green energy and vegetable oil refining engineering. High-capacity Anaerobic Digestion Compressed Biogas (CBG / Bio-CNG) plants from Napier grass & agri-waste alongside dynamic high-shear continuous vegetable oil neutralization systems.
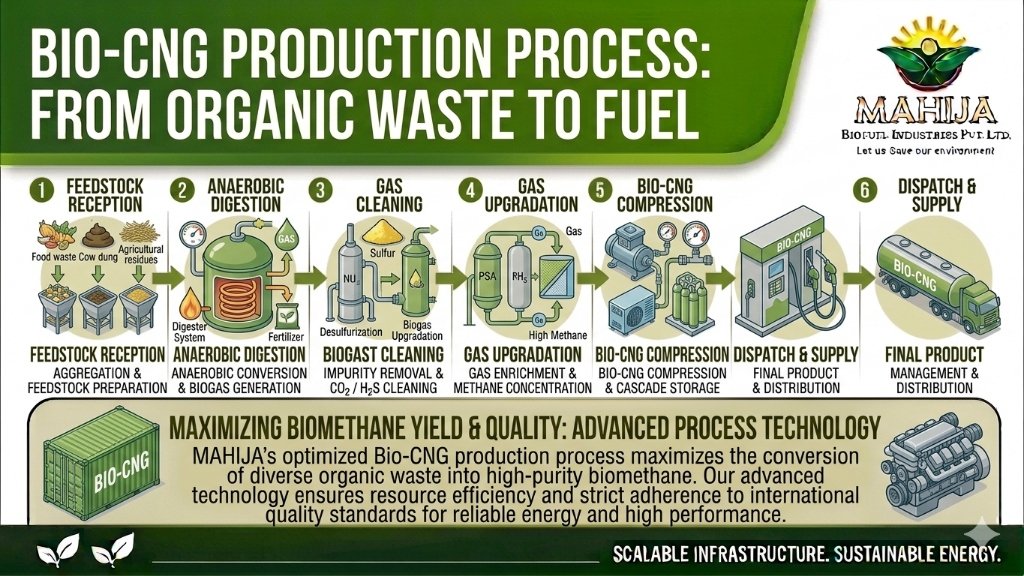
Anaerobic CSTR Digesters, PSA / Membrane Purification, 250-bar Compression & Organic Fertilizers.
Compressed Biogas (CBG): Our turnkey CBG plants utilize advanced Continuous Stirred Tank Reactor (CSTR) anaerobic digestion to process high-yielding energy crops like Napier grass, cattle dung, sugar mill press mud, and organic wastes into vehicle-grade Bio-CNG compliant with IS 16087 standards and the Government of India’s SATAT initiative.
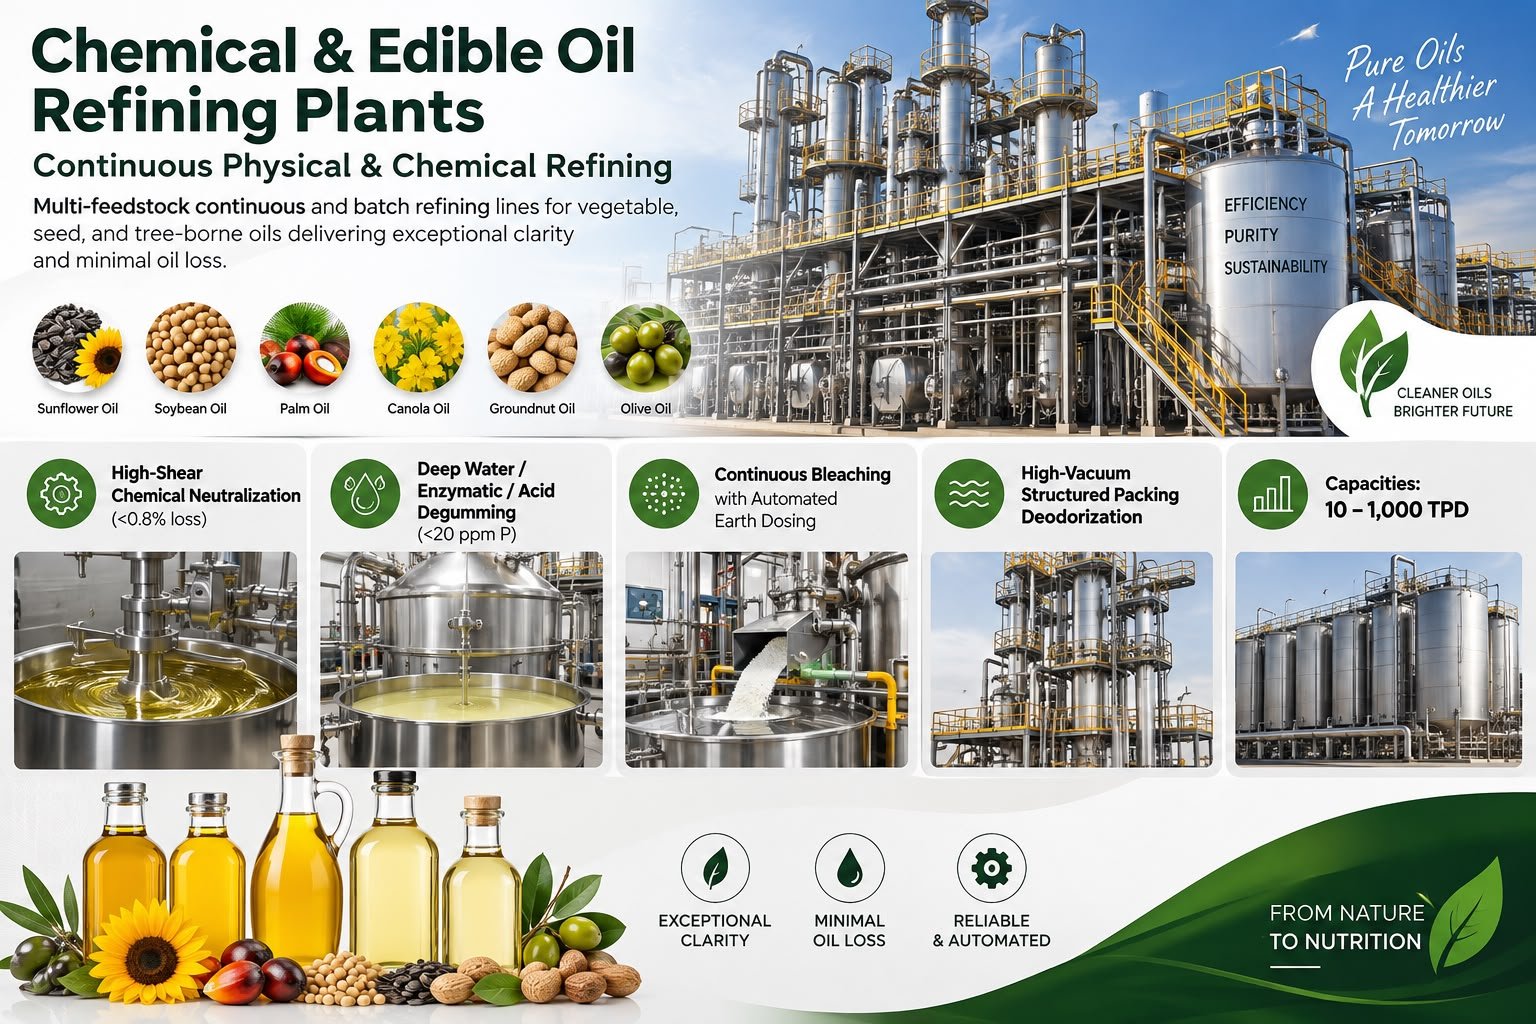
Continuous Oil Neutralization: For crude edible & industrial vegetable oils, MAHIJA delivers continuous neutralization units equipped with dynamic high-shear mixers and disc-stack centrifuges for complete free fatty acid (FFA) saponification with minimal neutral oil entrainment.
Anaerobic digestion produces premium organic bio-fertilizers rich in organic carbon and humus, serving as a lucrative supplementary revenue stream:
Get our comprehensive project report with biomass yields, gas purification sizing, and financial ROI.
Request Technical Proposal Call +917016074249| CBG Capacity | Napier Grass Feed | Cattle Dung Feed | Biogas Generated | CBG Output (kg/Day) | Land Requirement | Project CAPEX | Power Connected | Typical Payback |
|---|---|---|---|---|---|---|---|---|
| 1 TPD | 25 MT/Day | 3 MT/Day | 2,600 - 2,900 m³ | 950 - 1,100 | 1 Acre | ₹ 4 - 5 Cr | 80 - 100 KW | 2 - 3 Years |
| 3 TPD | 75 MT/Day | 10 MT/Day | 7,875 - 8,625 m³ | 2,900 - 3,200 | 2 - 3 Acres | ₹ 11 - 12 Cr | 246 KW | |
| 5 TPD | 125 MT/Day | 18 MT/Day | 13,000 - 14,000 m³ | 4,800 - 5,300 | 4 - 5 Acres | ₹ 17 - 19 Cr | 425 - 450 KW | |
| 6 TPD | 150 MT/Day | 25 MT/Day | 15,750 - 17,250 m³ | 5,800 - 6,400 | 5 - 6 Acres | ₹ 21 - 22 Cr | 532 KW |
| CBG Capacity | FOM Solid Organic Manure (TPD) | LFOM Liquid Bio-Fertilizer (KLPD) |
|---|---|---|
| 1 TPD | 5 - 7 TPD | 15 - 20 KLPD |
| 3 TPD | 15 - 20 TPD | 45 - 50 KLPD |
| 5 TPD | 25 - 28 TPD | 75 - 80 KLPD |
| 6 TPD | 30 TPD | 90 - 95 KLPD |
Standalone or integrated acid degumming units for the removal of hydratable and non-hydratable phosphatides (gums) from crude vegetable oils using food-grade phosphoric acid dosing and high-speed centrifugal separation.
Acid degumming converts non-hydratable phosphatides (NHP) into hydratable form for complete centrifugal removal. Uses precision food-grade phosphoric acid dosing (0.1–0.2% on oil) at 60–70°C to reduce total phosphorus below 20 ppm, ensuring downstream refining or biodiesel transesterification proceeds without catalyst fouling.
The separated lecithin-rich gums can be processed and dried as high-value commercial lecithin by-products.
MAHIJA operates ISO-certified and DSIR-approved manufacturing facilities to deliver turnkey plants for extraction, edible oil refining, oleochemicals, bioethanol, and biodiesel. We design, fabricate, and commission high-efficiency processing plants that meet strict international quality and safety standards across global markets.
Complete turnkey solvent extraction plants engineered for maximum oil recovery with minimum solvent loss and lowest utility consumption.
Multi-feedstock continuous and batch refining lines for vegetable, seed, and tree-borne oils delivering exceptional clarity and minimal oil loss.
Advanced high-pressure thermal splitting and distillation technologies converting natural fats and oils into high-purity fatty acids and refined glycerin.
Specialized plants for tailoring fat properties and fatty acid compositions to produce trans-free specialty fats, olein, stearin, and structured lipids.
Engineered systems for the production of high-margin value-added derivatives from refining gums, fats, and confectionery lipid bases.
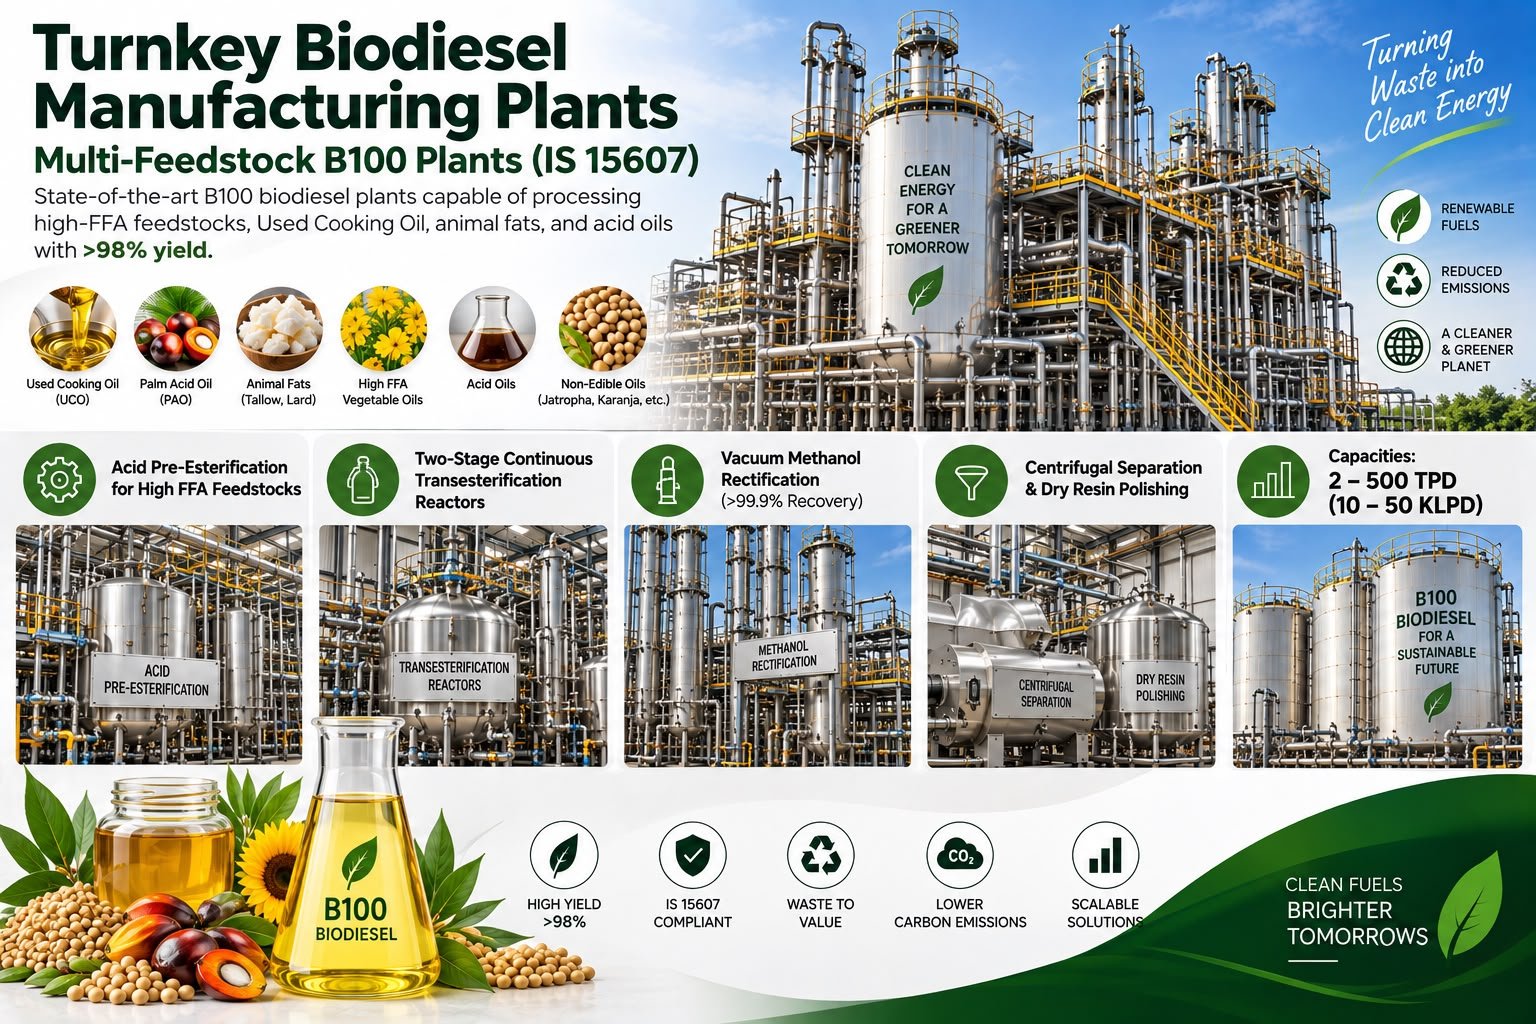
State-of-the-art B100 biodiesel plants capable of processing high-FFA feedstocks, Used Cooking Oil, animal fats, and acid oils with >98% yield.
Turnkey grain-based distilleries with zero liquid discharge (ZLD), molecular sieve dehydration (MSDH), and CSTR anaerobic digester systems.
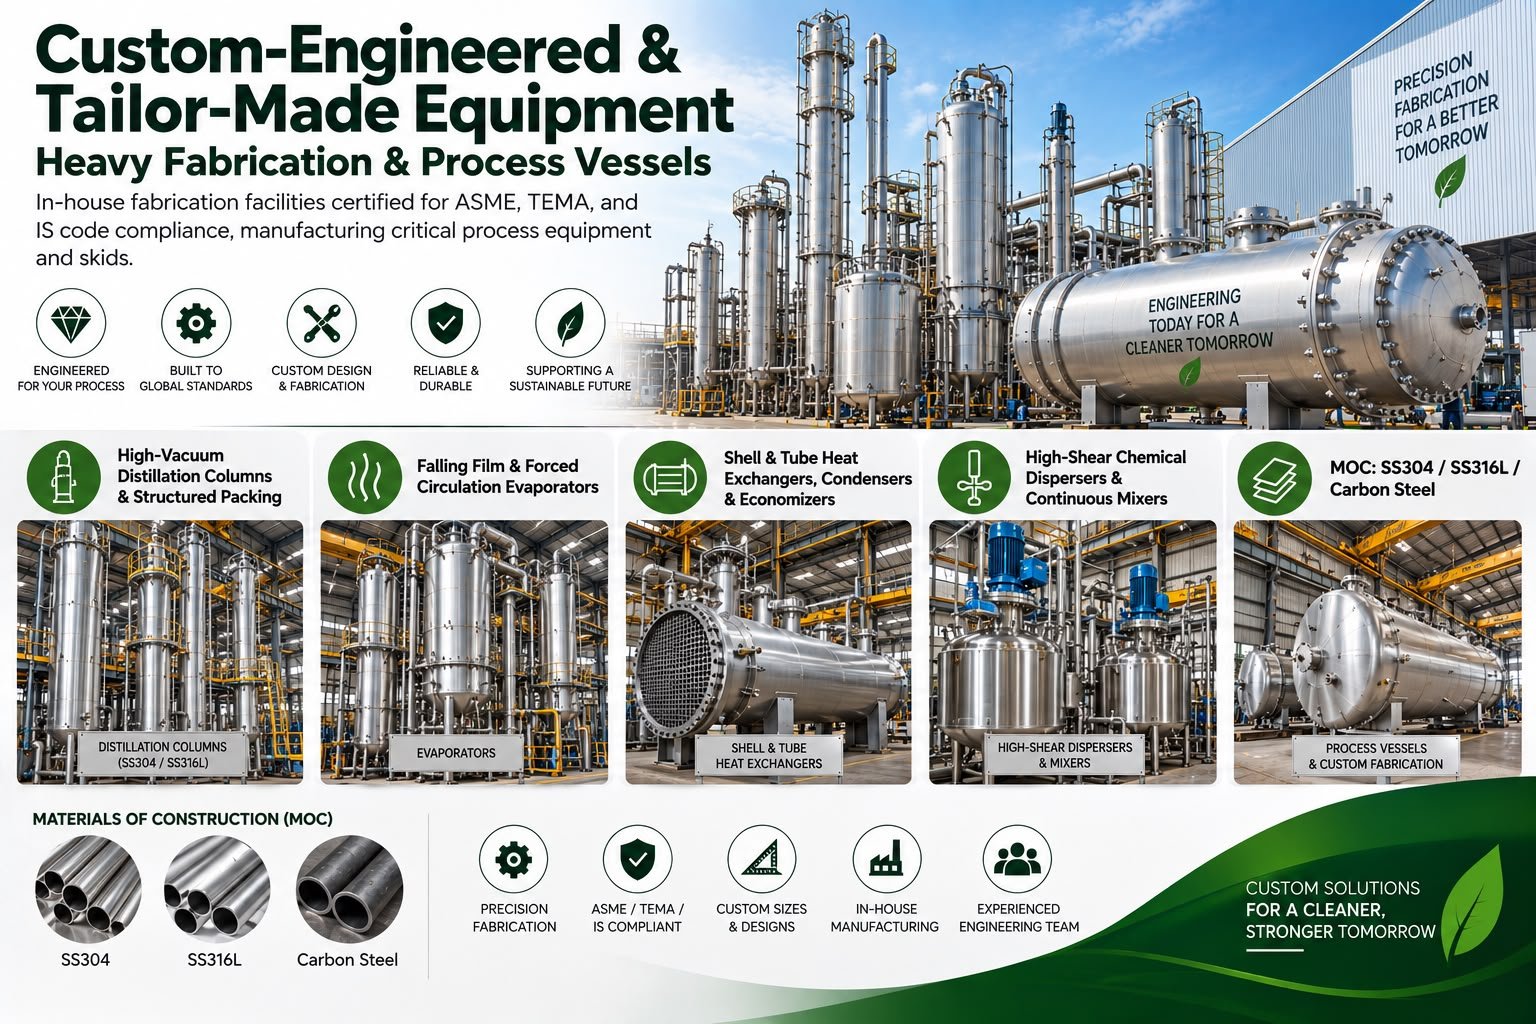
In-house fabrication facilities certified for ASME, TEMA, and IS code compliance, manufacturing critical process equipment and skids.
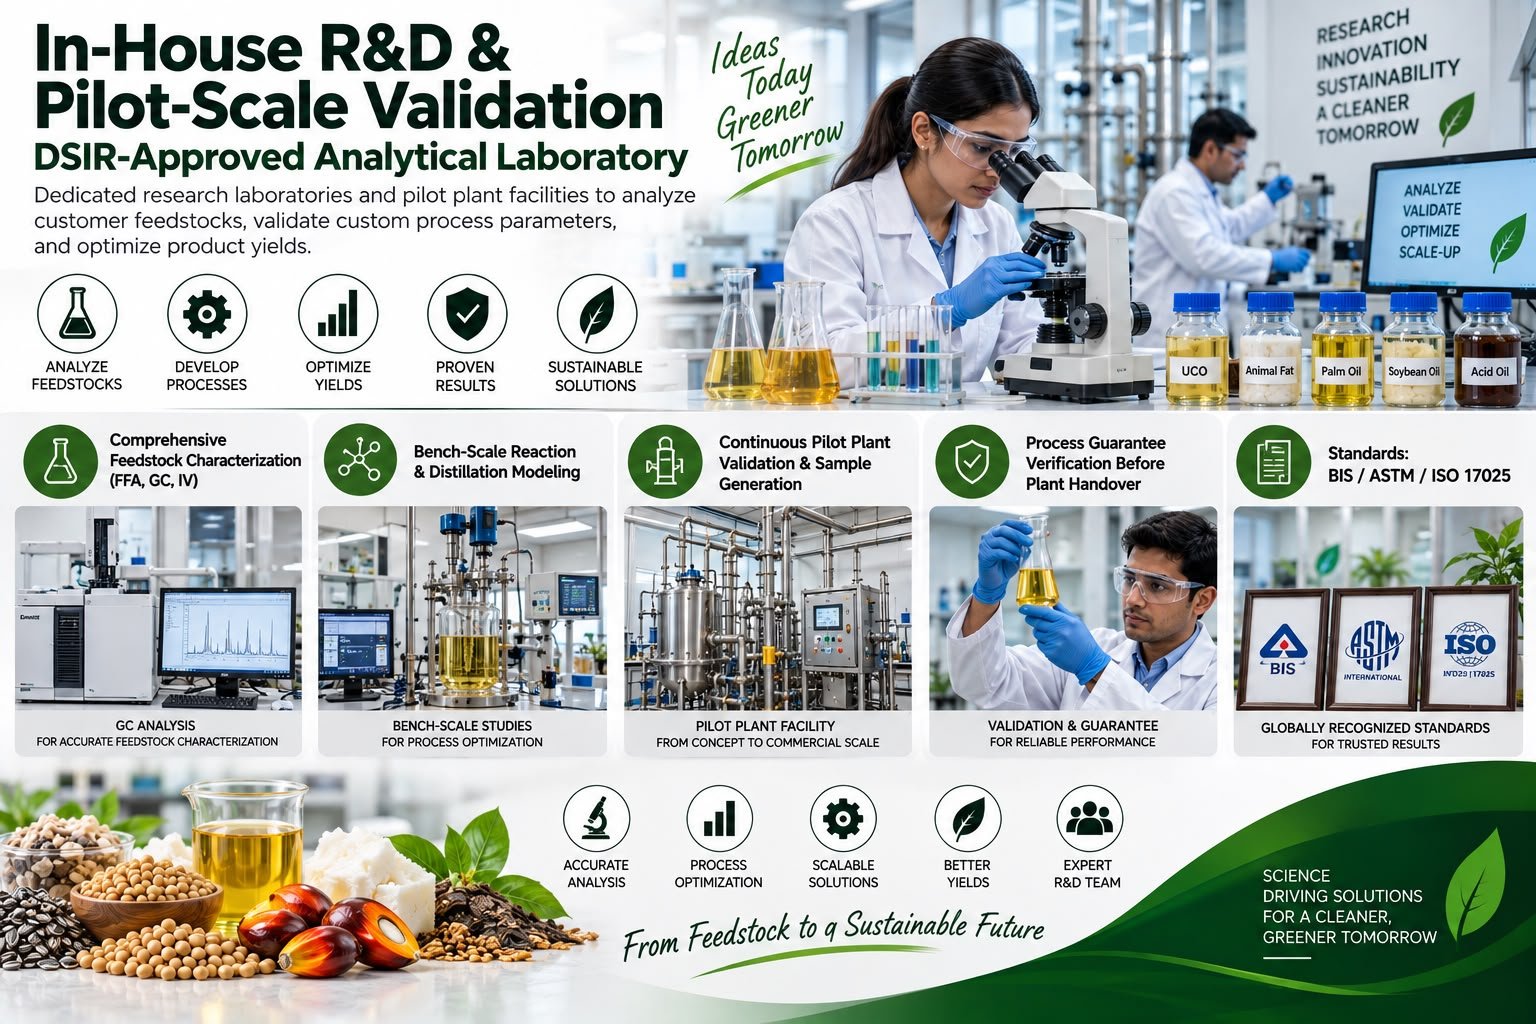
Dedicated research laboratories and pilot plant facilities to analyze customer feedstocks, validate custom process parameters, and optimize product yields.
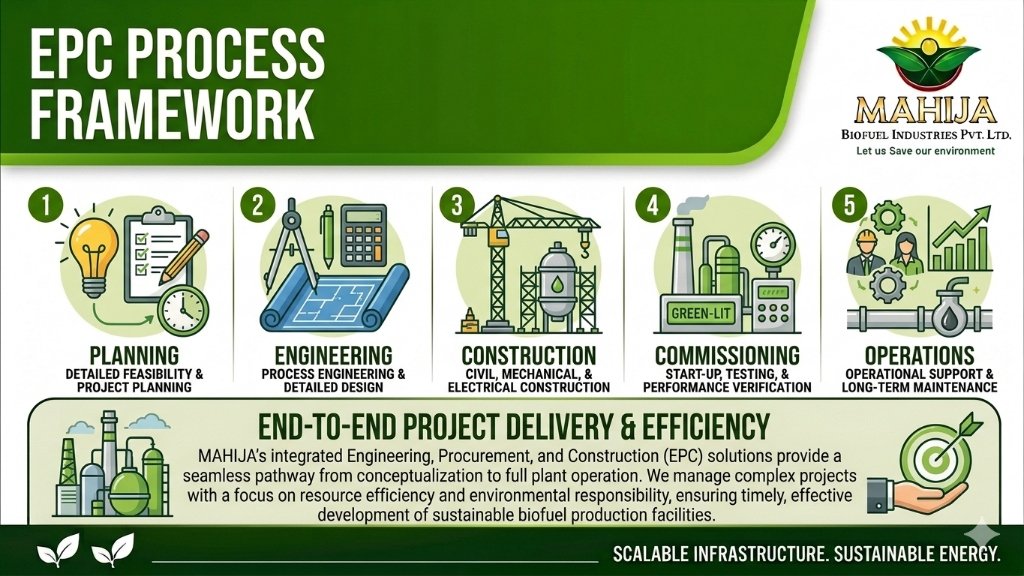
From detailed feasibility analysis and conceptual engineering to fabrication, erection, commissioning, and long-term operational support.
With over 15+ years of chemical engineering experience and ISO 9001:2015 certified workshops, we ensure your plant delivers guaranteed yields, lowest utility consumption, and rapid return on investment.