Process & Technology Infographic
Full technical schematic, unit operations, and process architecture.
Comprehensive Plant Engineering & Technology Architecture
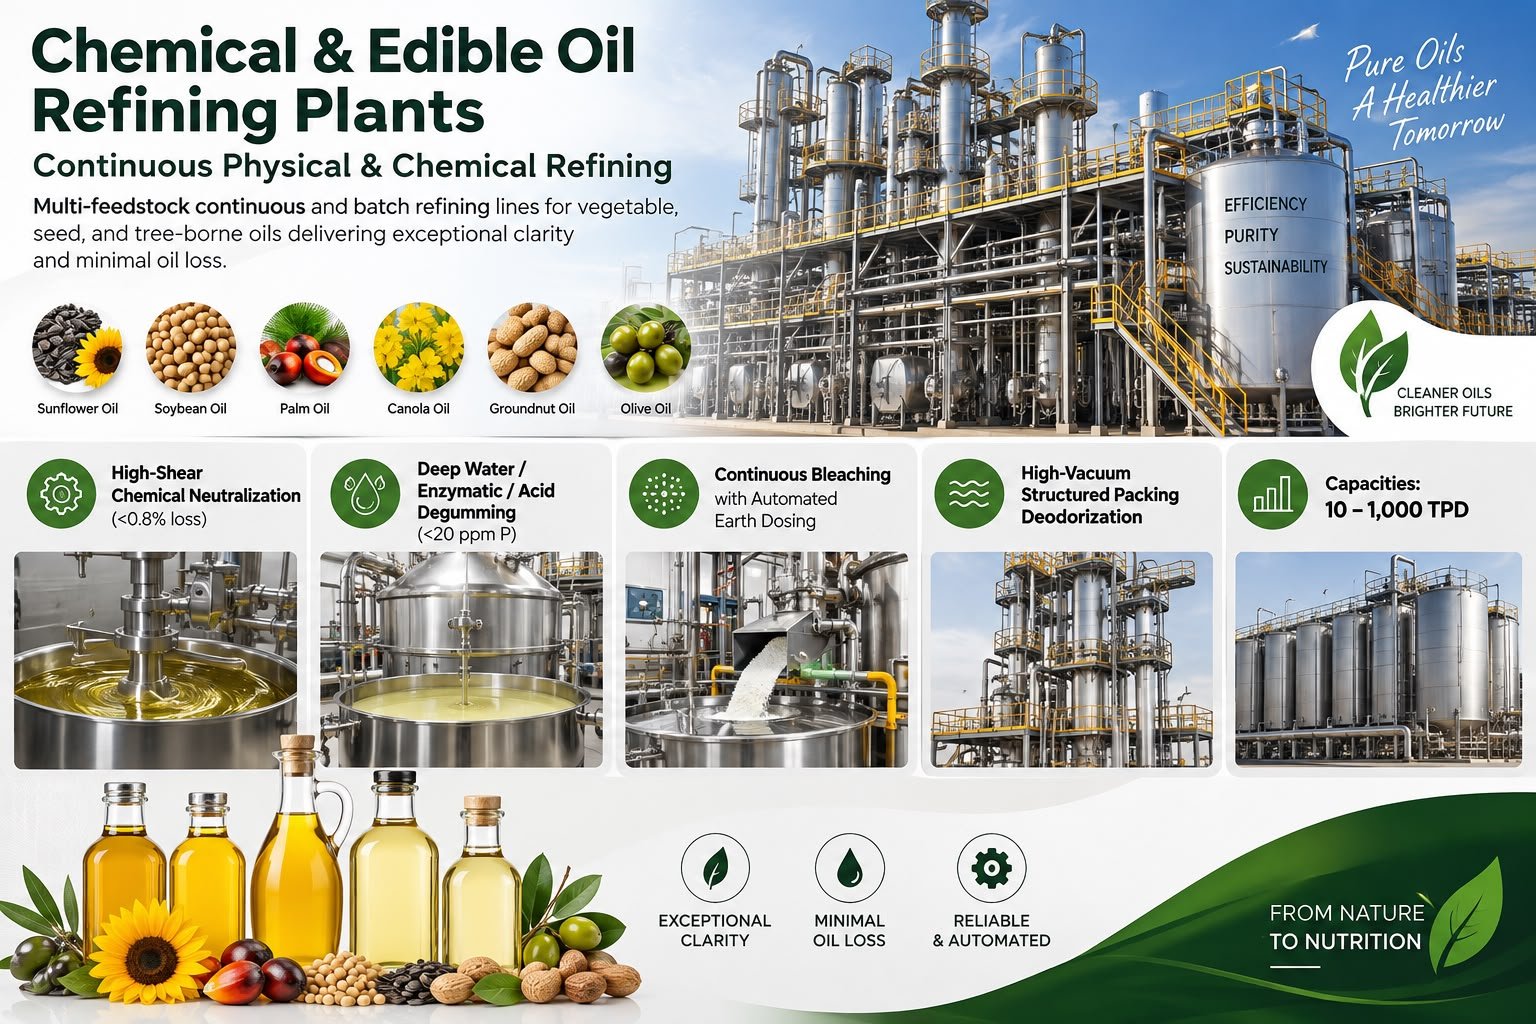
Our physical and chemical edible oil refining facilities are engineered to process both low and high-FFA crude vegetable oils. Featuring high-efficiency acid/enzymatic degumming, self-cleaning disc-stack centrifuges, continuous vacuum bleaching with hermetic leaf filters, and structured packing deodorizers with dual-temperature stripping, MAHIJA refining plants produce refined oils meeting the highest national and international food standards (FSSAI, Codex, ASTM).
Key Process Stages & Methodology
Integrated continuous engineering flow from raw feedstock preparation to final finished product output.
Acid & Enzymatic Degumming
High-shear conditioning with phosphoric/citric acid followed by enzyme reaction to transform non-hydratable phospholipids into hydratable gums.
Continuous Neutralization & Washing
Precise caustic dosing and multi-stage disc centrifuge separation with minimum neutral oil saponification.
Vacuum Bleaching & Pressure Leaf Filtration
Continuous counter-current bleaching vessel with automated earth/silica dosing and dual alternating leaf filters.
High-Vacuum Deodorization & Deacidification
Structured packing columns operating under 1.5–3.0 mbar vacuum for stripping free fatty acids and volatile odorants.
Heat Recovery & Polishing
Multi-pass economizers reclaiming >85% of thermal energy followed by sub-micron polishing filtration.
Engineered System Capabilities
Design Specifications & Performance Guarantees
| Parameter / Metric | Engineering Benchmark & Value |
|---|---|
| Capacity Range | 10 to 1,000 TPD |
| Refining Loss | < 1.1 × FFA (Physical) / < 1.25 × FFA (Chemical) |
| Final FFA Content | < 0.05% Max |
| Moisture & Volatiles | < 0.03% Max |
| Color (Lovibond 5¼" Cell) | < 1.0 – 2.0 Red (Feedstock dependent) |
| Deodorizer Vacuum | 1.5 – 3.0 mbar with 4-stage steam ejector + chillers |
| Thermal Economy | > 85% heat recovery via internal regenerative heat exchangers |
Compatible Feedstocks & Industrial Outputs
Inquire Sizing & Feasibility
Get custom mass-energy balance, civil layout, and DPR estimates.
Explore All 9 Turnkey Engineering Facilities
Solvent Extraction Systems & Technology
Complete turnkey solvent extraction plants engineered for maximum oil recovery with minimum solvent loss and lowest utility consumption.
Chemical & Edible Oil Refining Plants
Multi-feedstock continuous and batch refining lines for vegetable, seed, and tree-borne oils delivering exceptional clarity and minimal oil loss.
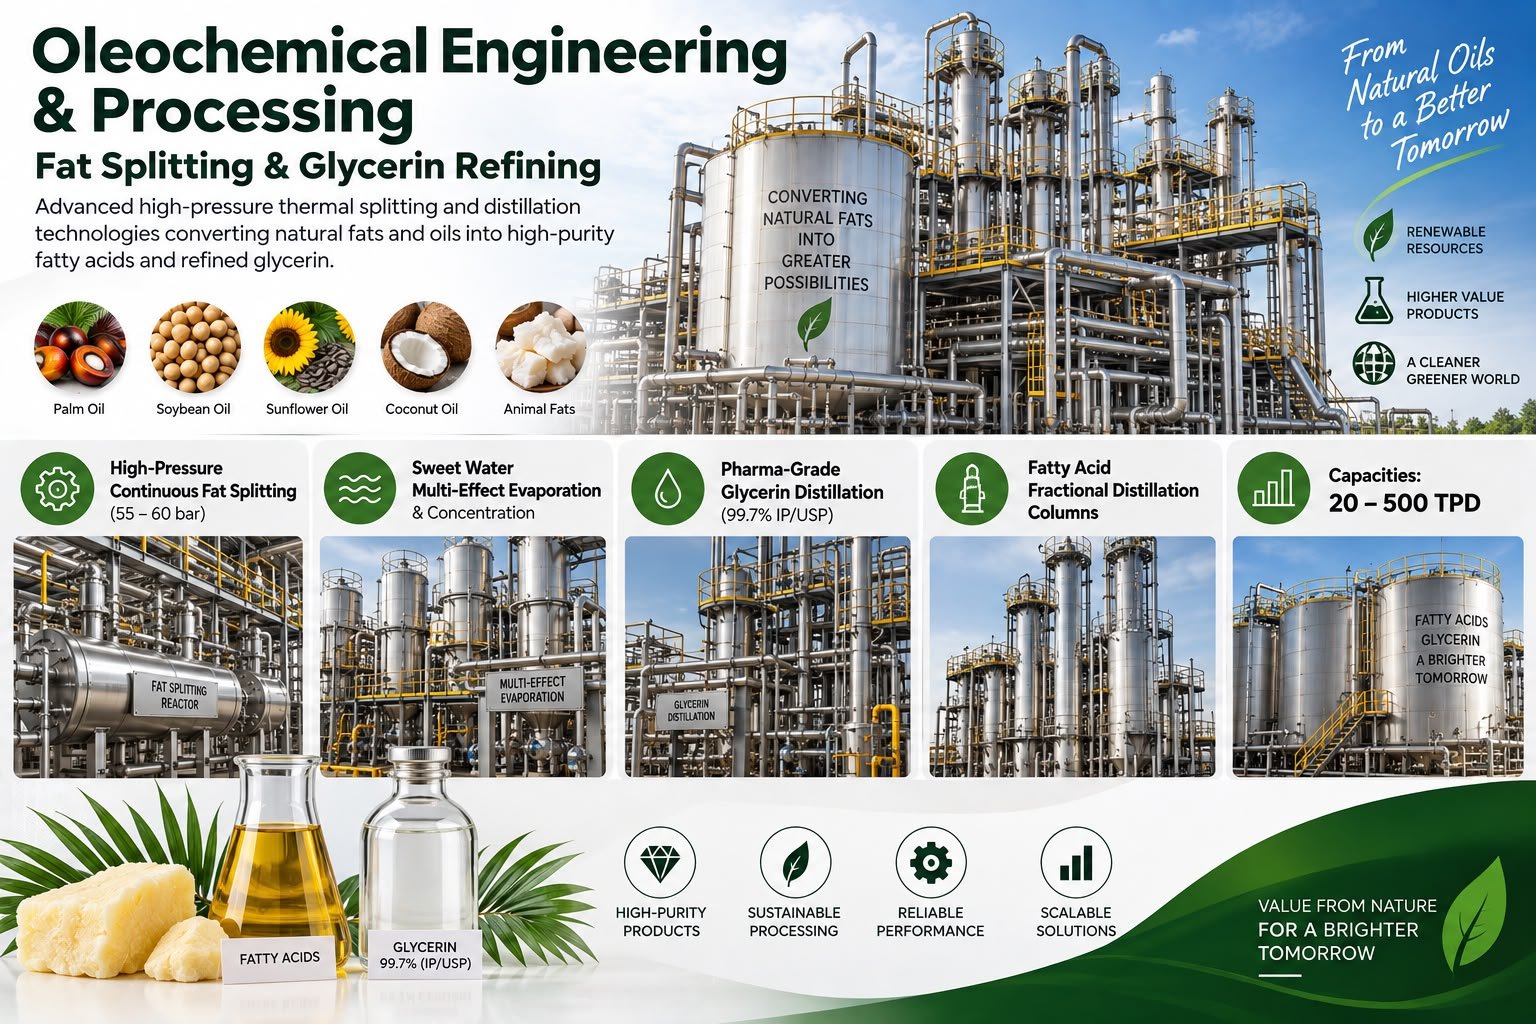
Oleochemical Engineering & Processing
Advanced high-pressure thermal splitting and distillation technologies converting natural fats and oils into high-purity fatty acids and refined glycerin.
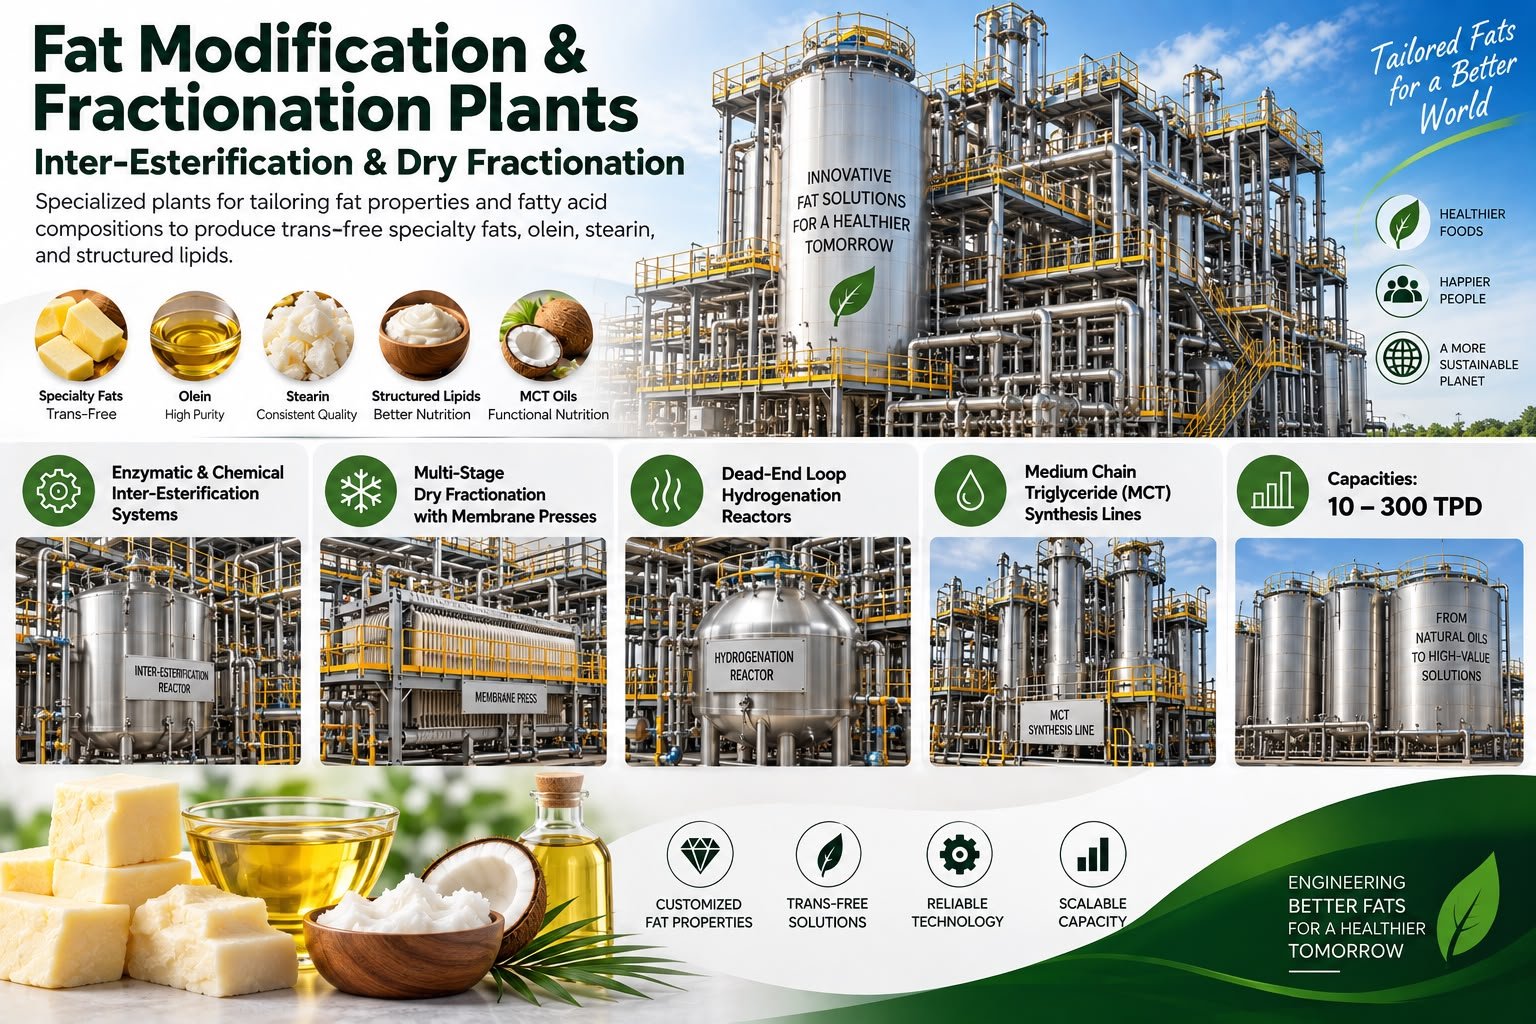
Fat Modification & Fractionation Plants
Specialized plants for tailoring fat properties and fatty acid compositions to produce trans-free specialty fats, olein, stearin, and structured lipids.
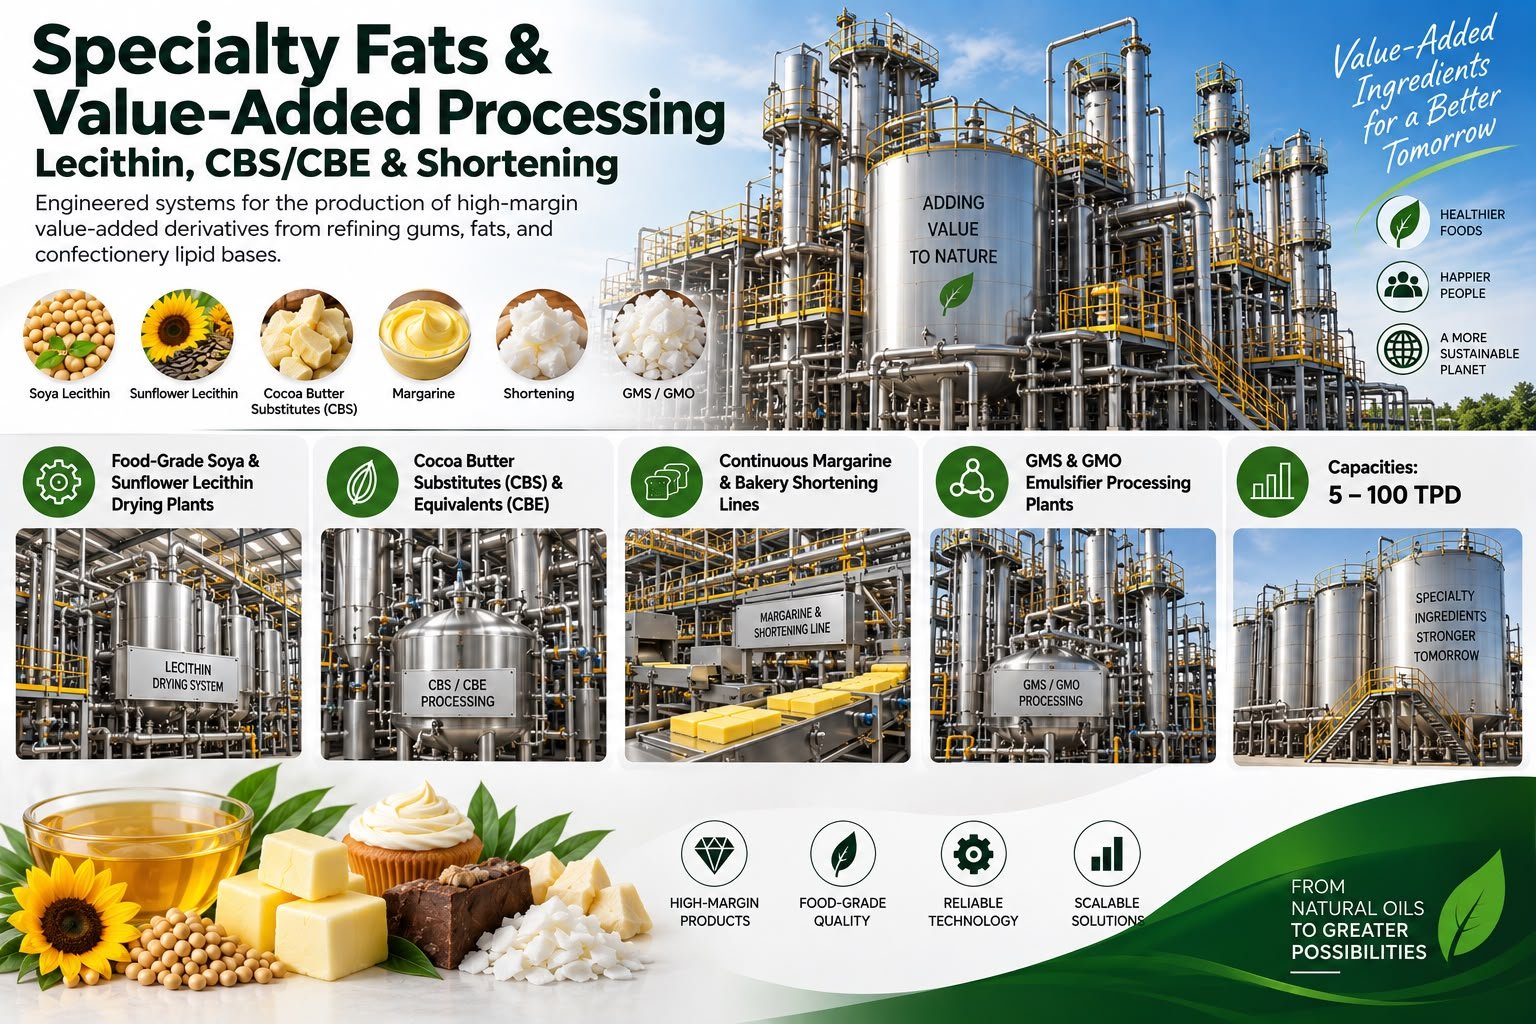
Specialty Fats & Value-Added Processing
Engineered systems for the production of high-margin value-added derivatives from refining gums, fats, and confectionery lipid bases.
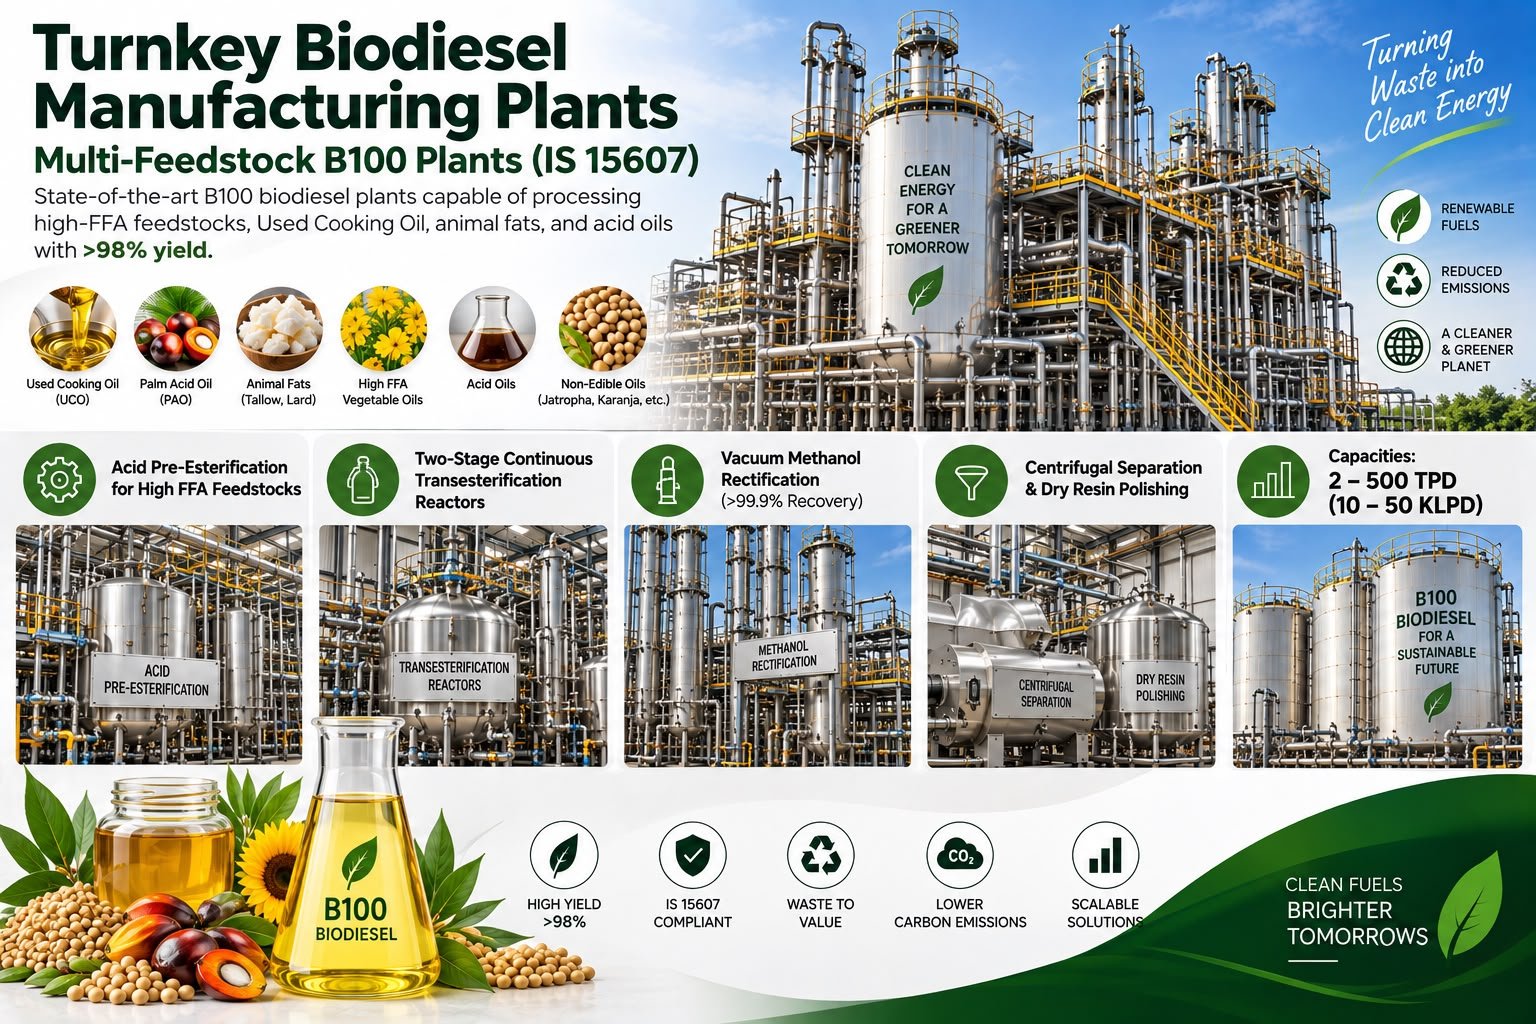
Turnkey Biodiesel Manufacturing Plants
State-of-the-art B100 biodiesel plants capable of processing high-FFA feedstocks, Used Cooking Oil, animal fats, and acid oils with >98% yield.
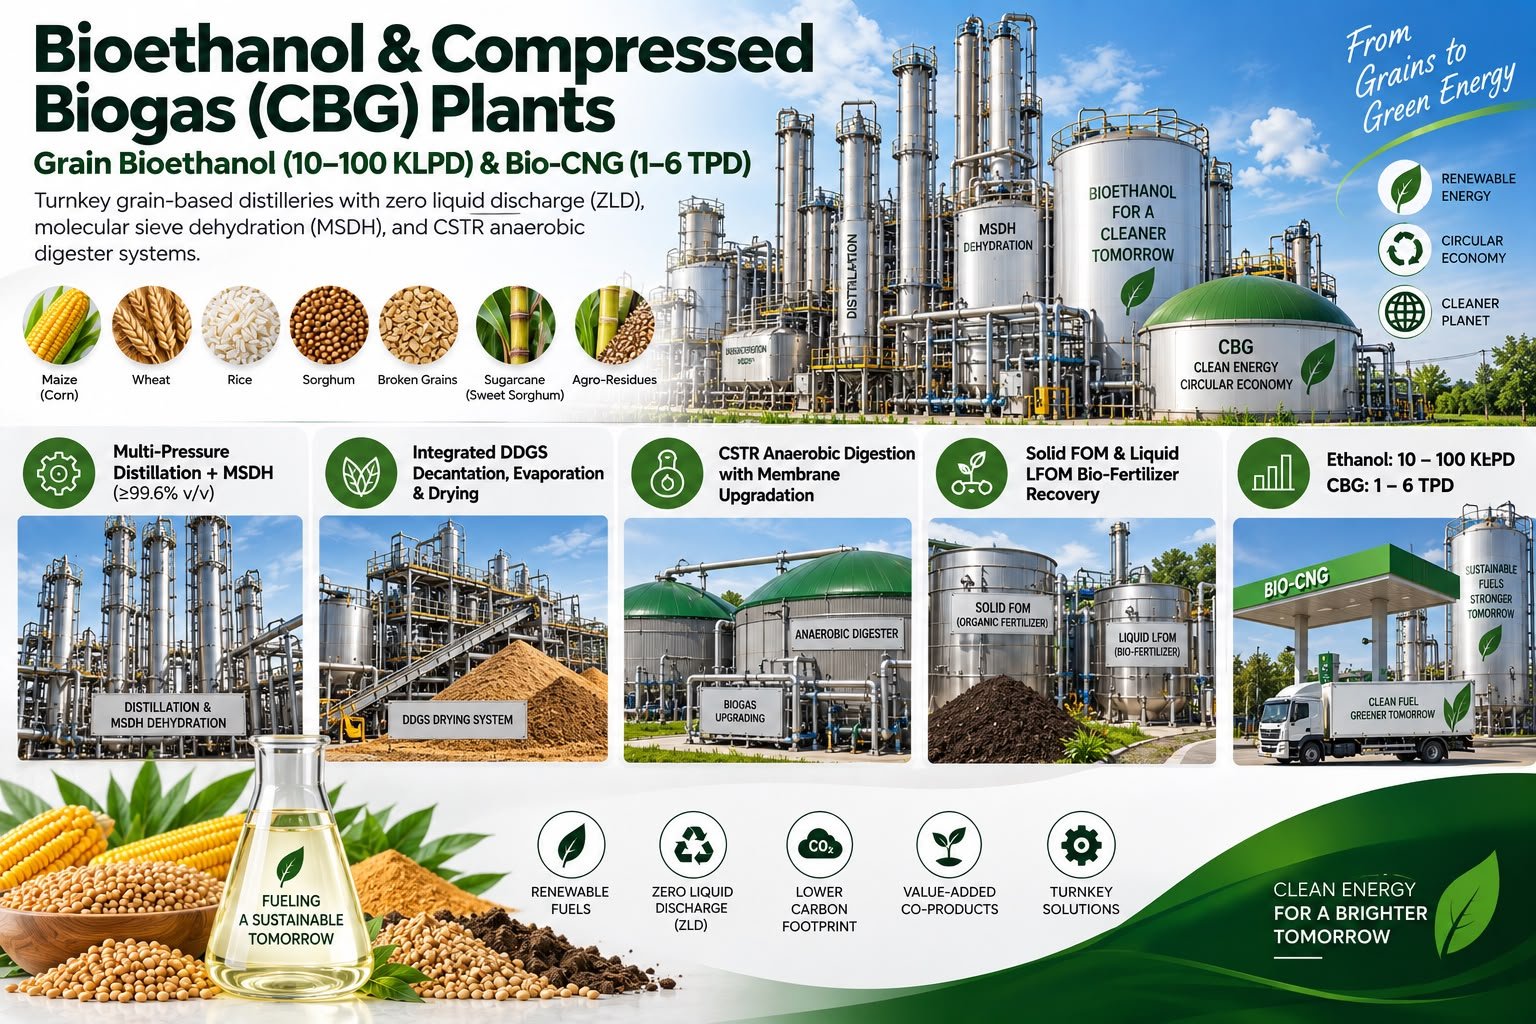
Bioethanol & Compressed Biogas (CBG) Plants
Turnkey grain-based distilleries with zero liquid discharge (ZLD), molecular sieve dehydration (MSDH), and CSTR anaerobic digester systems.
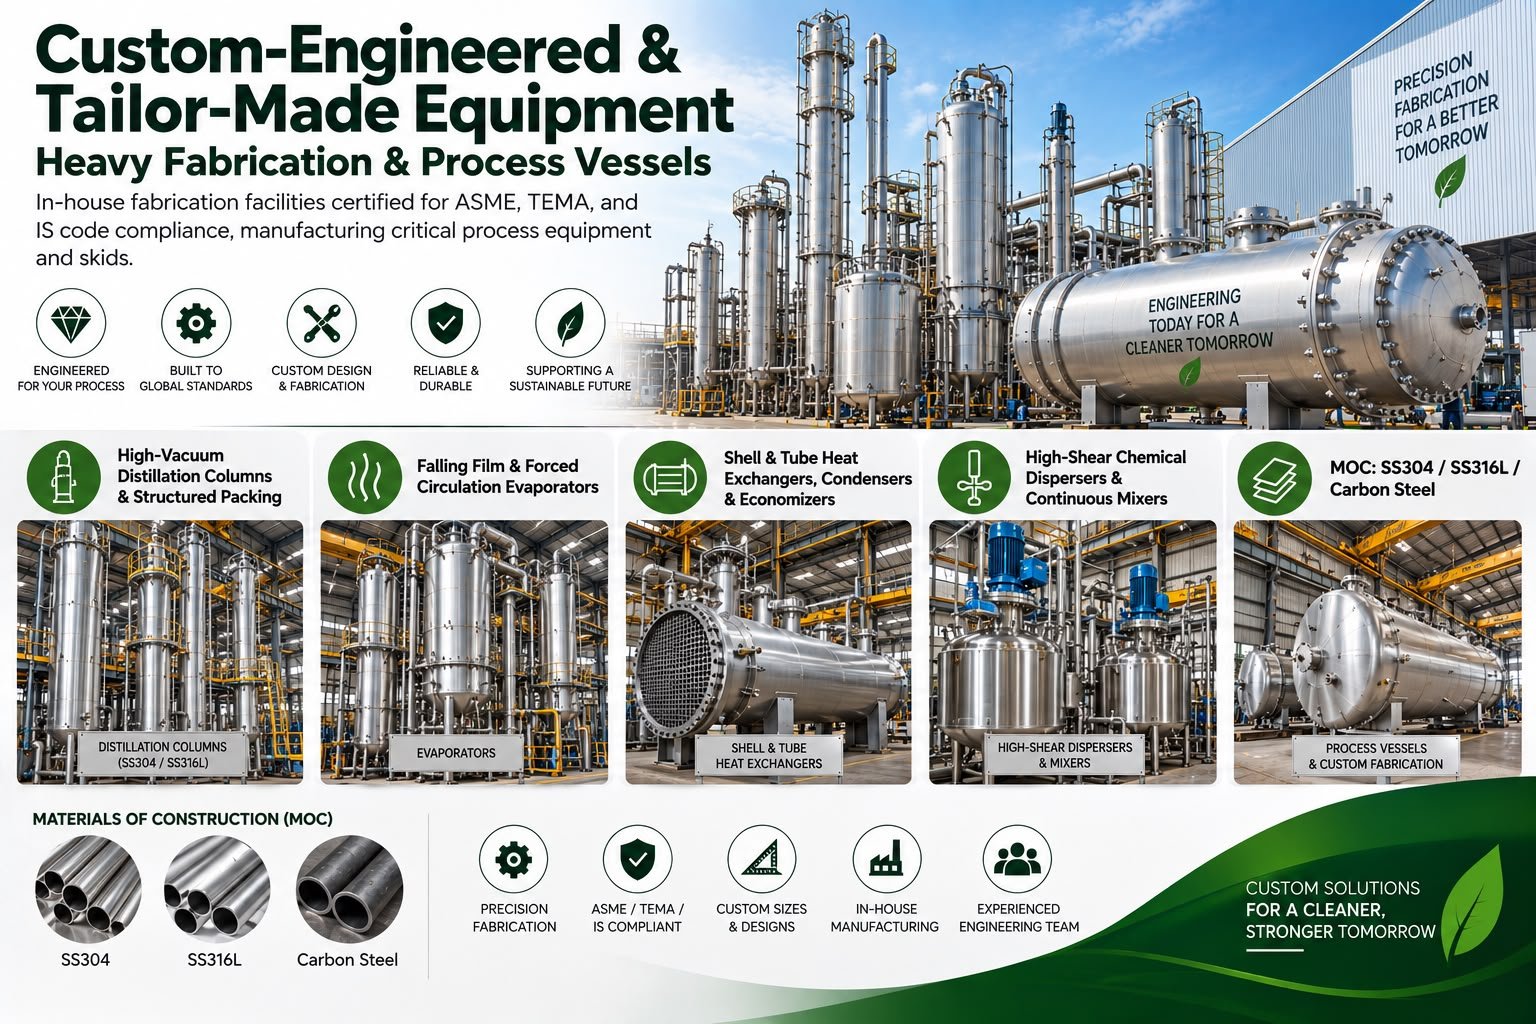
Custom-Engineered & Tailor-Made Equipment
In-house fabrication facilities certified for ASME, TEMA, and IS code compliance, manufacturing critical process equipment and skids.
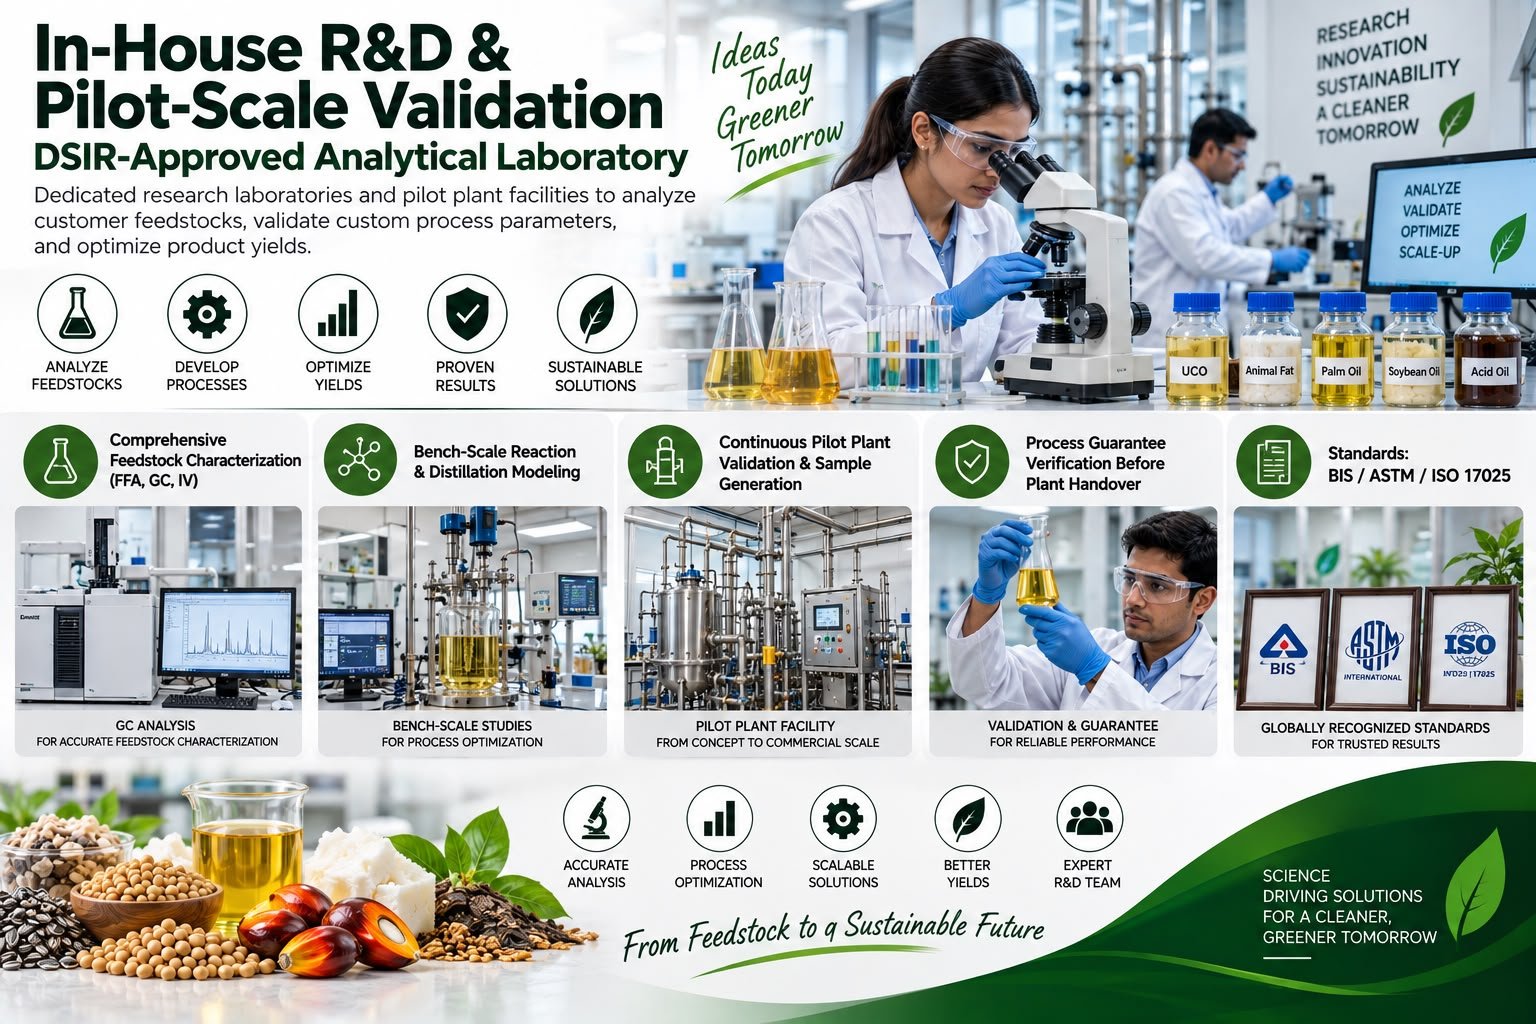
In-House R&D & Pilot-Scale Validation
Dedicated research laboratories and pilot plant facilities to analyze customer feedstocks, validate custom process parameters, and optimize product yields.