Process & Technology Infographic
Full technical schematic, unit operations, and process architecture.
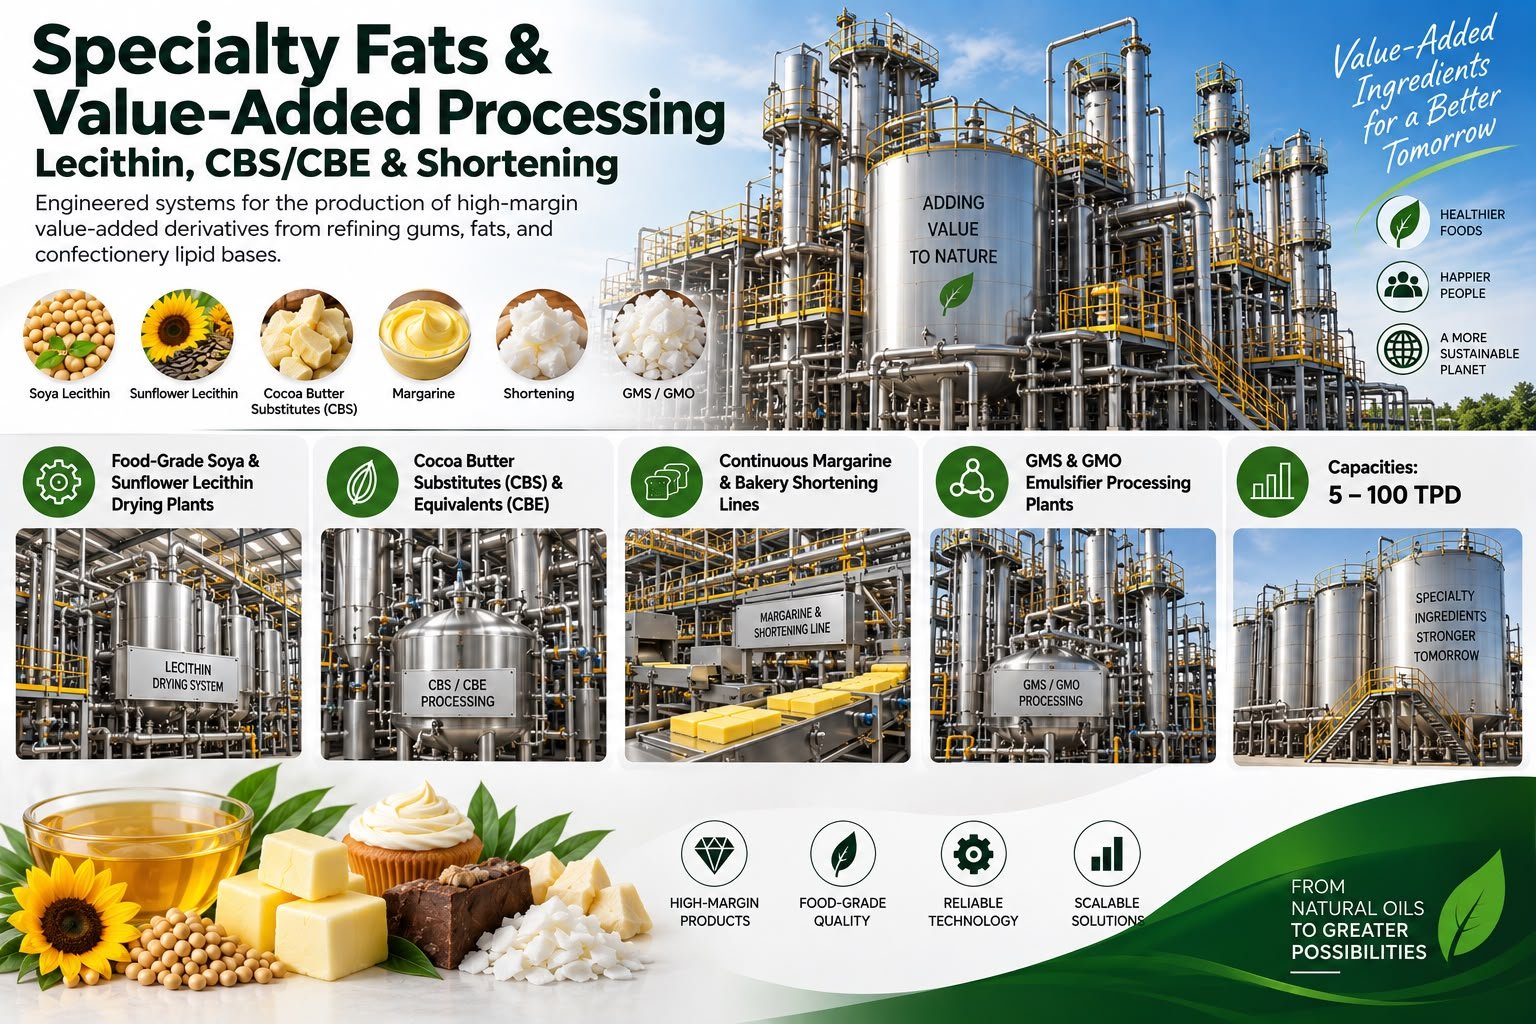
Comprehensive Plant Engineering & Technology Architecture
Turnkey downstream processing lines to transform refining co-products and vegetable fats into high-value specialty lipids: Food & pharma grade Lecithin dryers, CBS/CBE confectionery fats, continuous scraped surface heat exchanger (SSHE) margarine crystallization lines, and Glycerol Monostearate (GMS) plants.
Key Process Stages & Methodology
Integrated continuous engineering flow from raw feedstock preparation to final finished product output.
Lecithin Gum Drying & Bleaching
Continuous thin-film evaporators dehydrating wet gums below 0.5% moisture under vacuum.
Crystallization & Texturization (Votators)
High-pressure scraped surface heat exchangers and pin rotor crystallizers for pastry shortenings.
GMS & Emulsifier Esterification
Vacuum esterification and molecular distillation producing 90%+ mono-ester content.
Engineered System Capabilities
Design Specifications & Performance Guarantees
| Parameter / Metric | Engineering Benchmark & Value |
|---|---|
| Capacity Range | 5 to 100 TPD |
| Lecithin Acetone Insolubles | ≥ 62.0% (Food/Feed Grade) |
| Moisture in Lecithin | ≤ 0.50% Max |
| SSHE Refrigeration Media | Ammonia (NH3) / Glycol / Freon |
Compatible Feedstocks & Industrial Outputs
Inquire Sizing & Feasibility
Get custom mass-energy balance, civil layout, and DPR estimates.
Explore All 9 Turnkey Engineering Facilities
Solvent Extraction Systems & Technology
Complete turnkey solvent extraction plants engineered for maximum oil recovery with minimum solvent loss and lowest utility consumption.
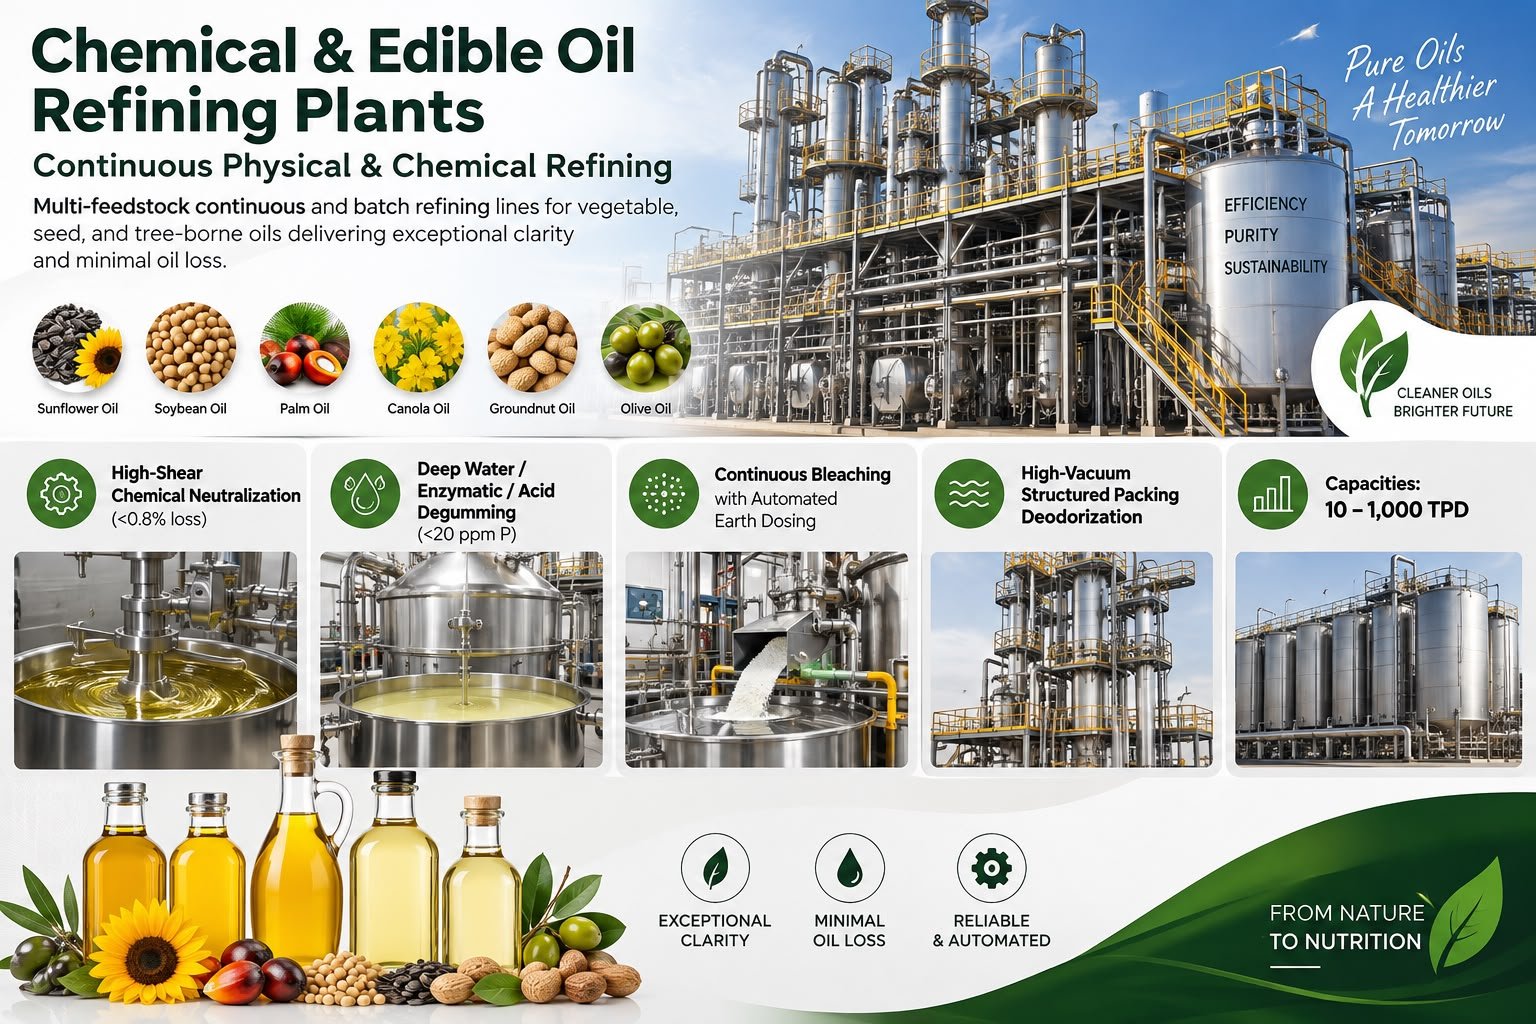
Chemical & Edible Oil Refining Plants
Multi-feedstock continuous and batch refining lines for vegetable, seed, and tree-borne oils delivering exceptional clarity and minimal oil loss.
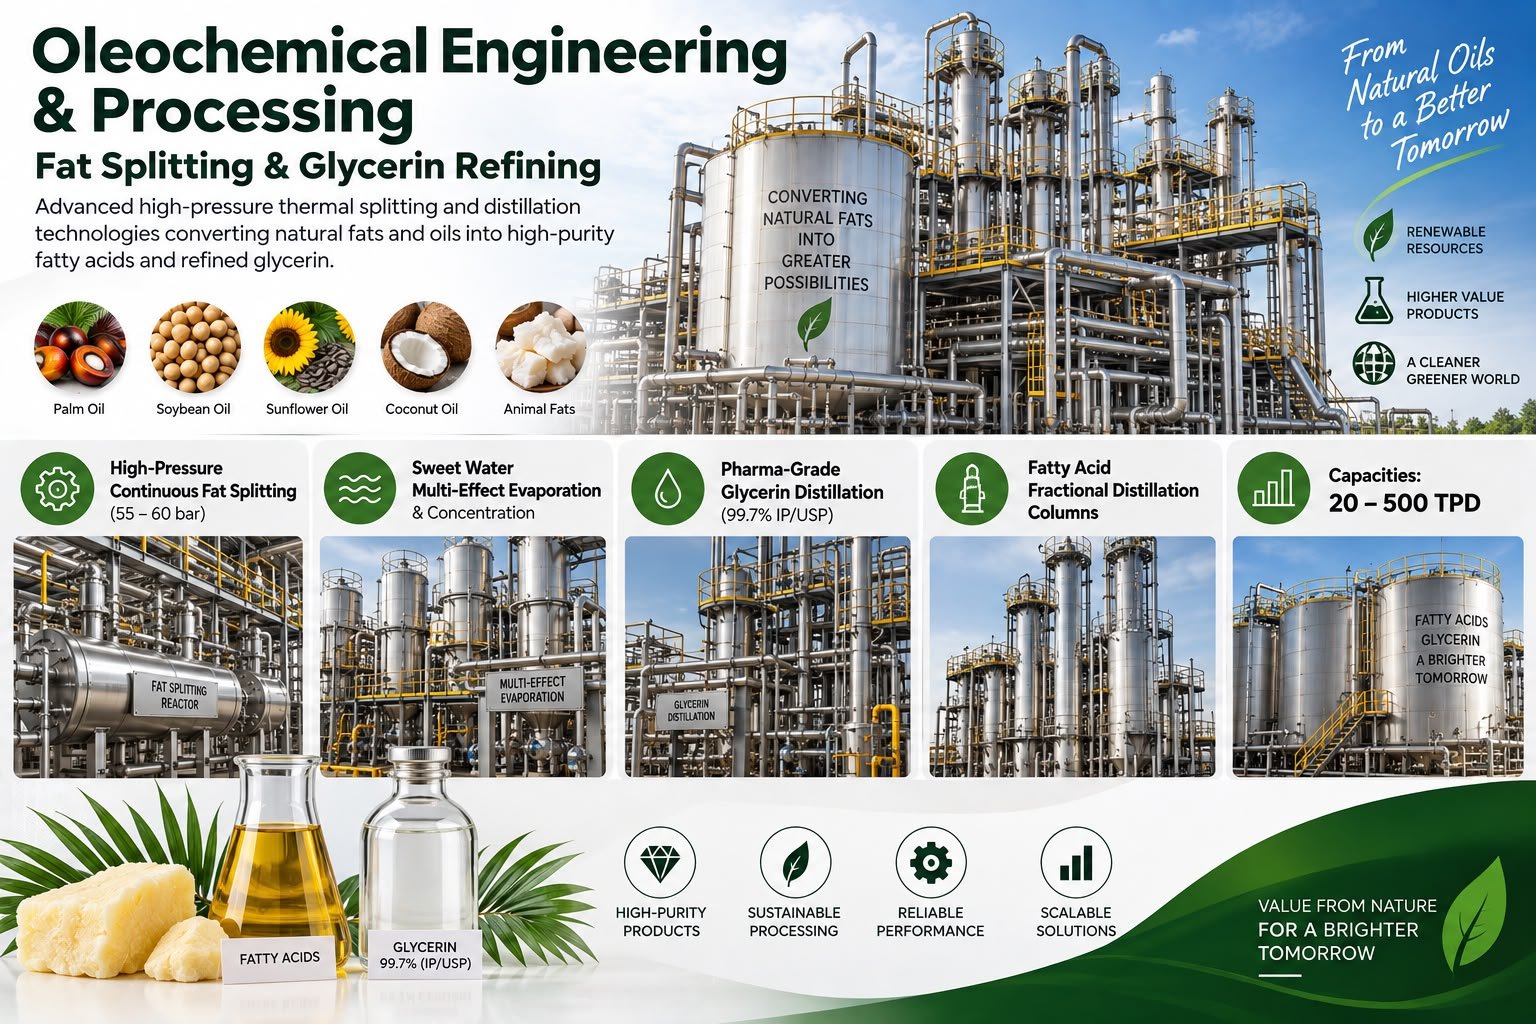
Oleochemical Engineering & Processing
Advanced high-pressure thermal splitting and distillation technologies converting natural fats and oils into high-purity fatty acids and refined glycerin.
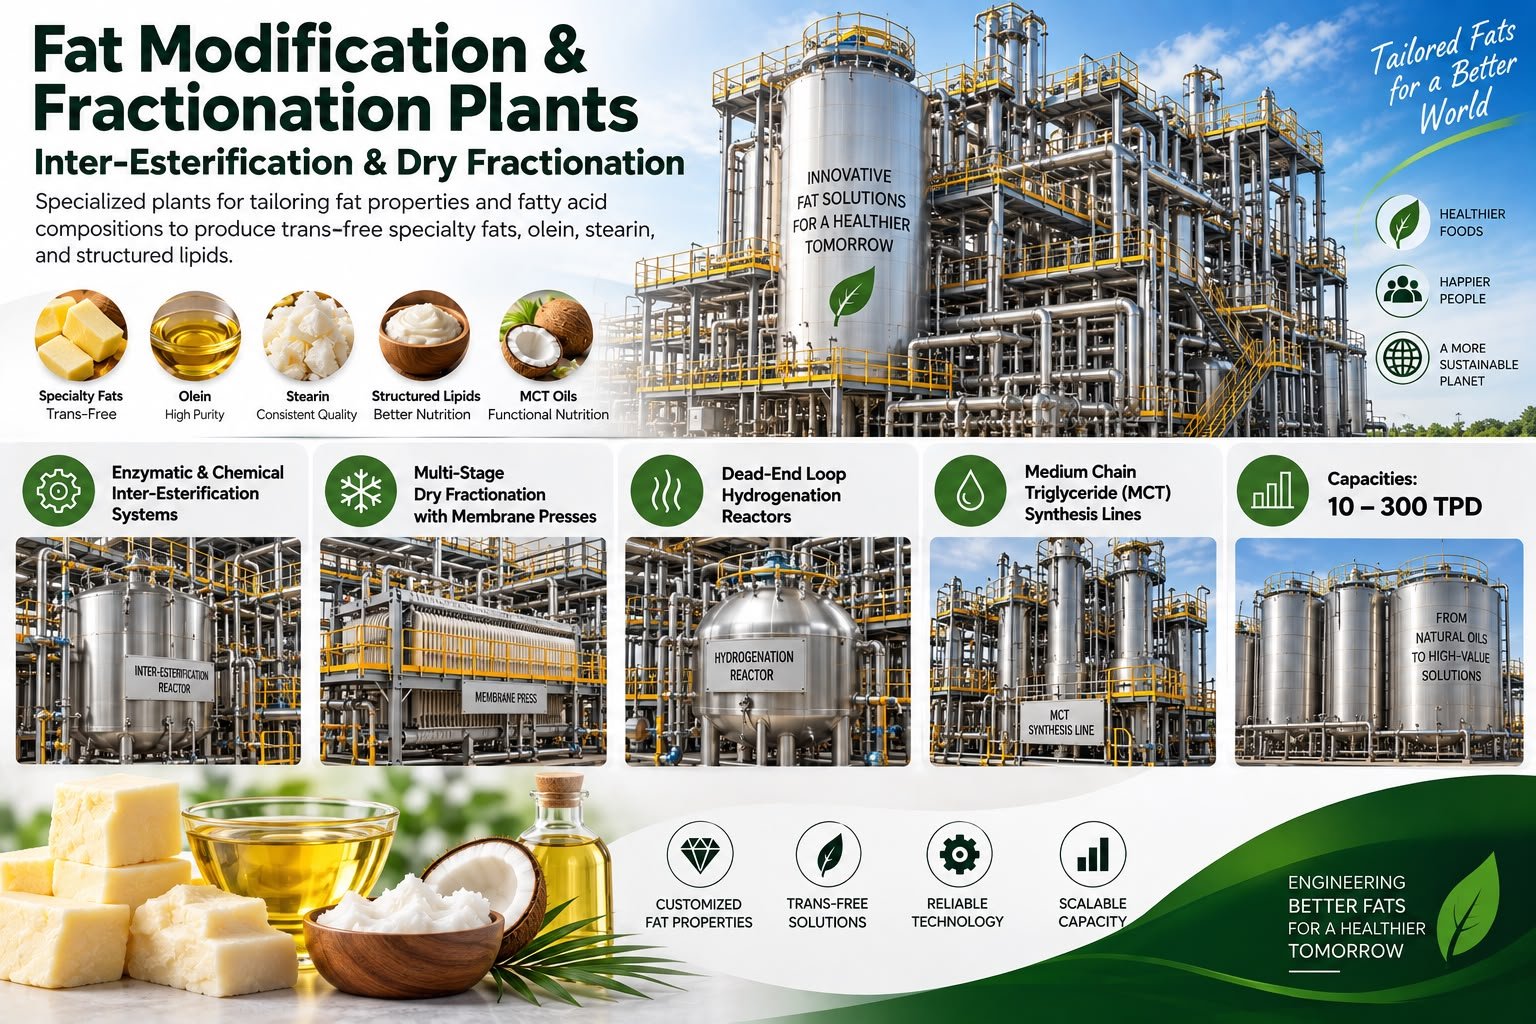
Fat Modification & Fractionation Plants
Specialized plants for tailoring fat properties and fatty acid compositions to produce trans-free specialty fats, olein, stearin, and structured lipids.
Specialty Fats & Value-Added Processing
Engineered systems for the production of high-margin value-added derivatives from refining gums, fats, and confectionery lipid bases.
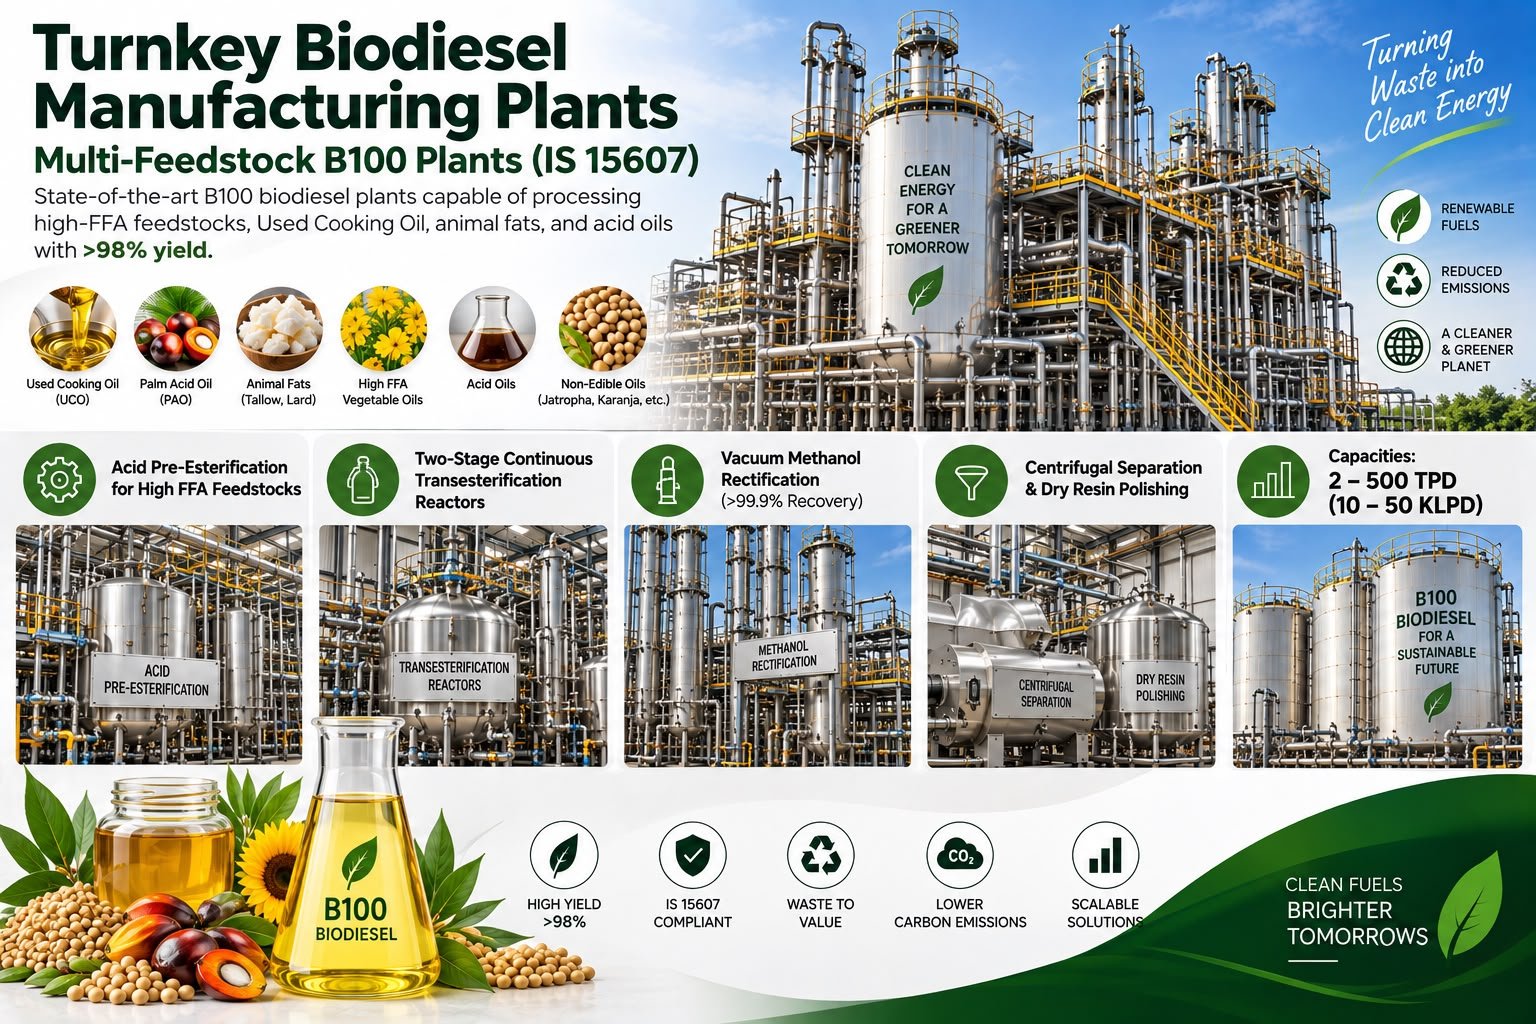
Turnkey Biodiesel Manufacturing Plants
State-of-the-art B100 biodiesel plants capable of processing high-FFA feedstocks, Used Cooking Oil, animal fats, and acid oils with >98% yield.
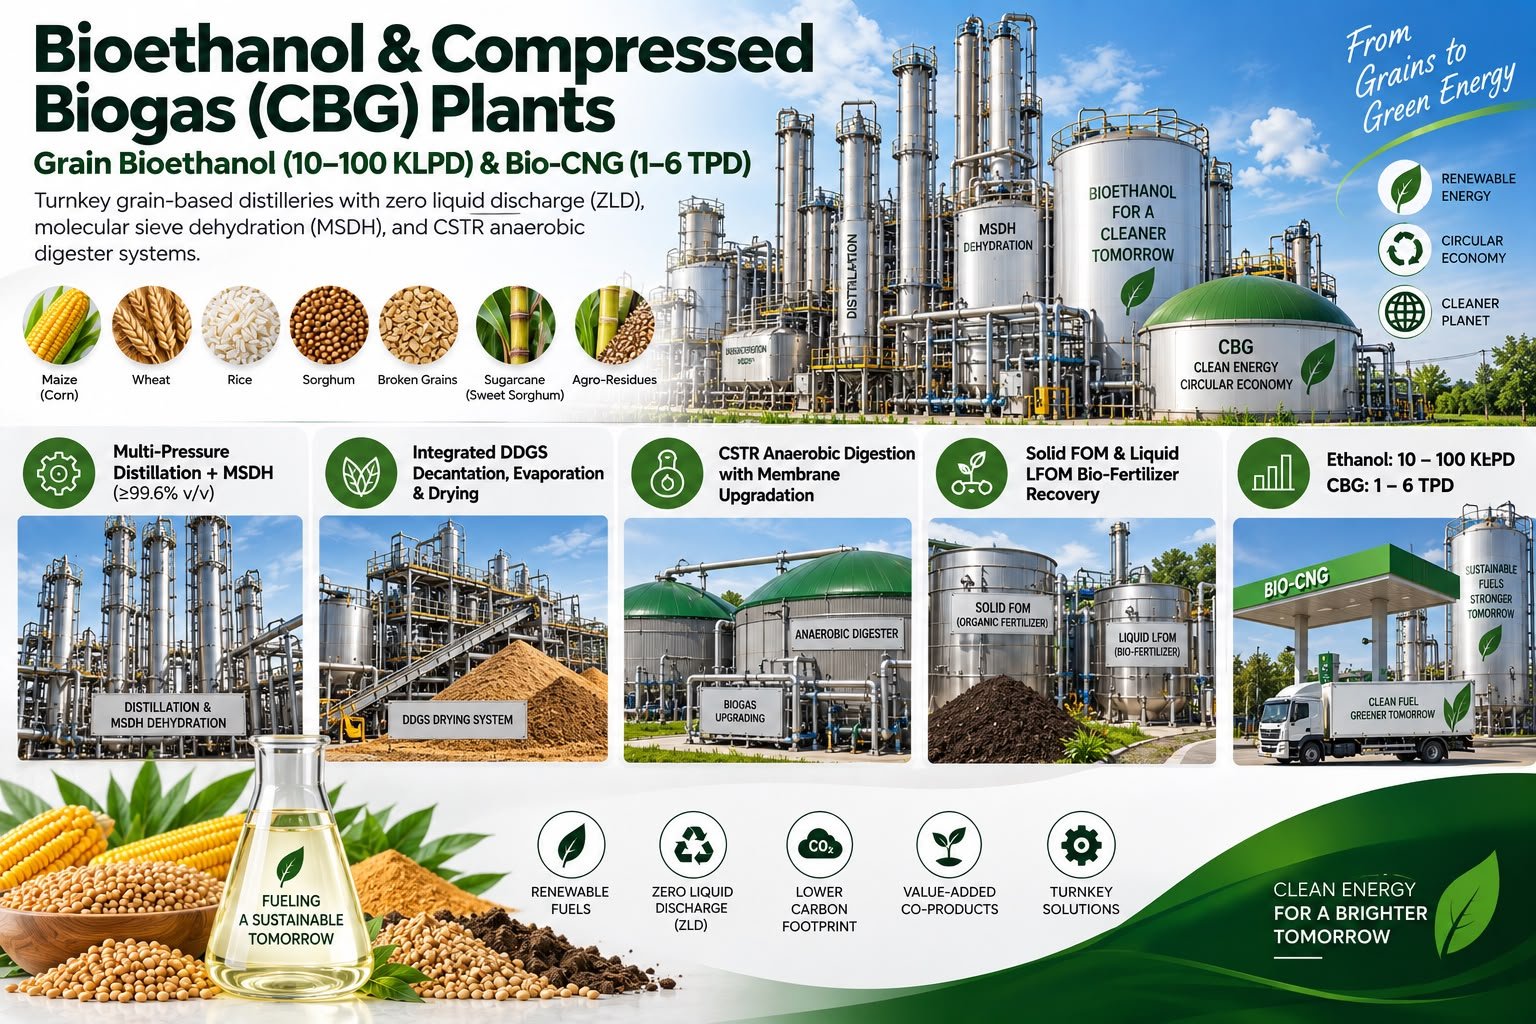
Bioethanol & Compressed Biogas (CBG) Plants
Turnkey grain-based distilleries with zero liquid discharge (ZLD), molecular sieve dehydration (MSDH), and CSTR anaerobic digester systems.
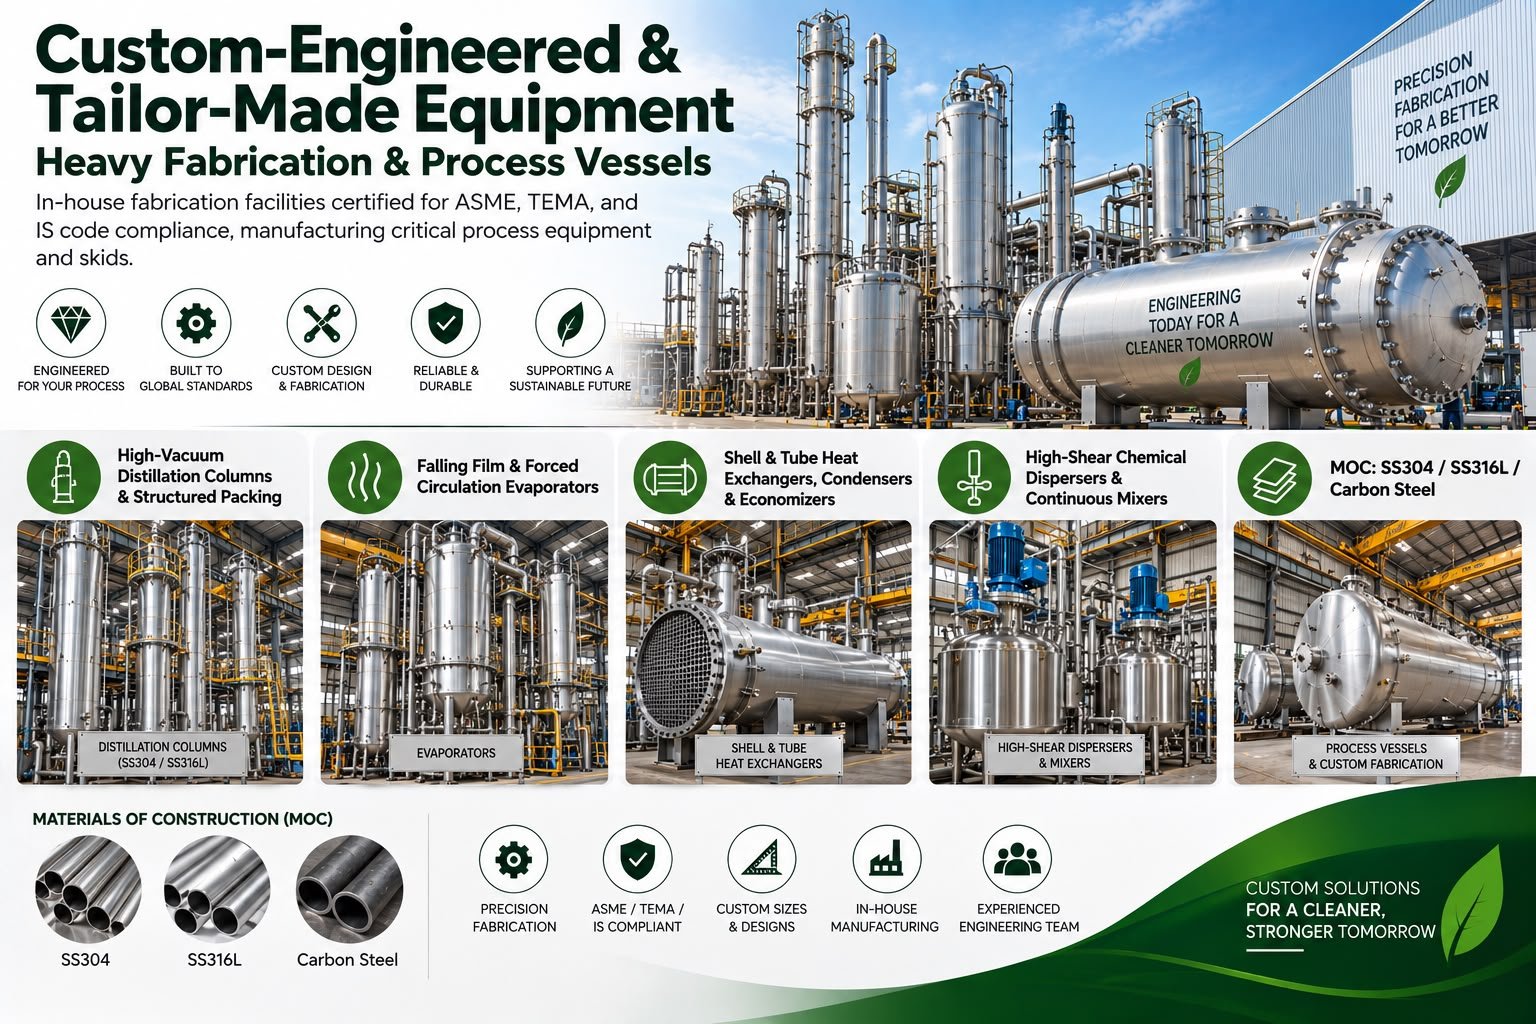
Custom-Engineered & Tailor-Made Equipment
In-house fabrication facilities certified for ASME, TEMA, and IS code compliance, manufacturing critical process equipment and skids.
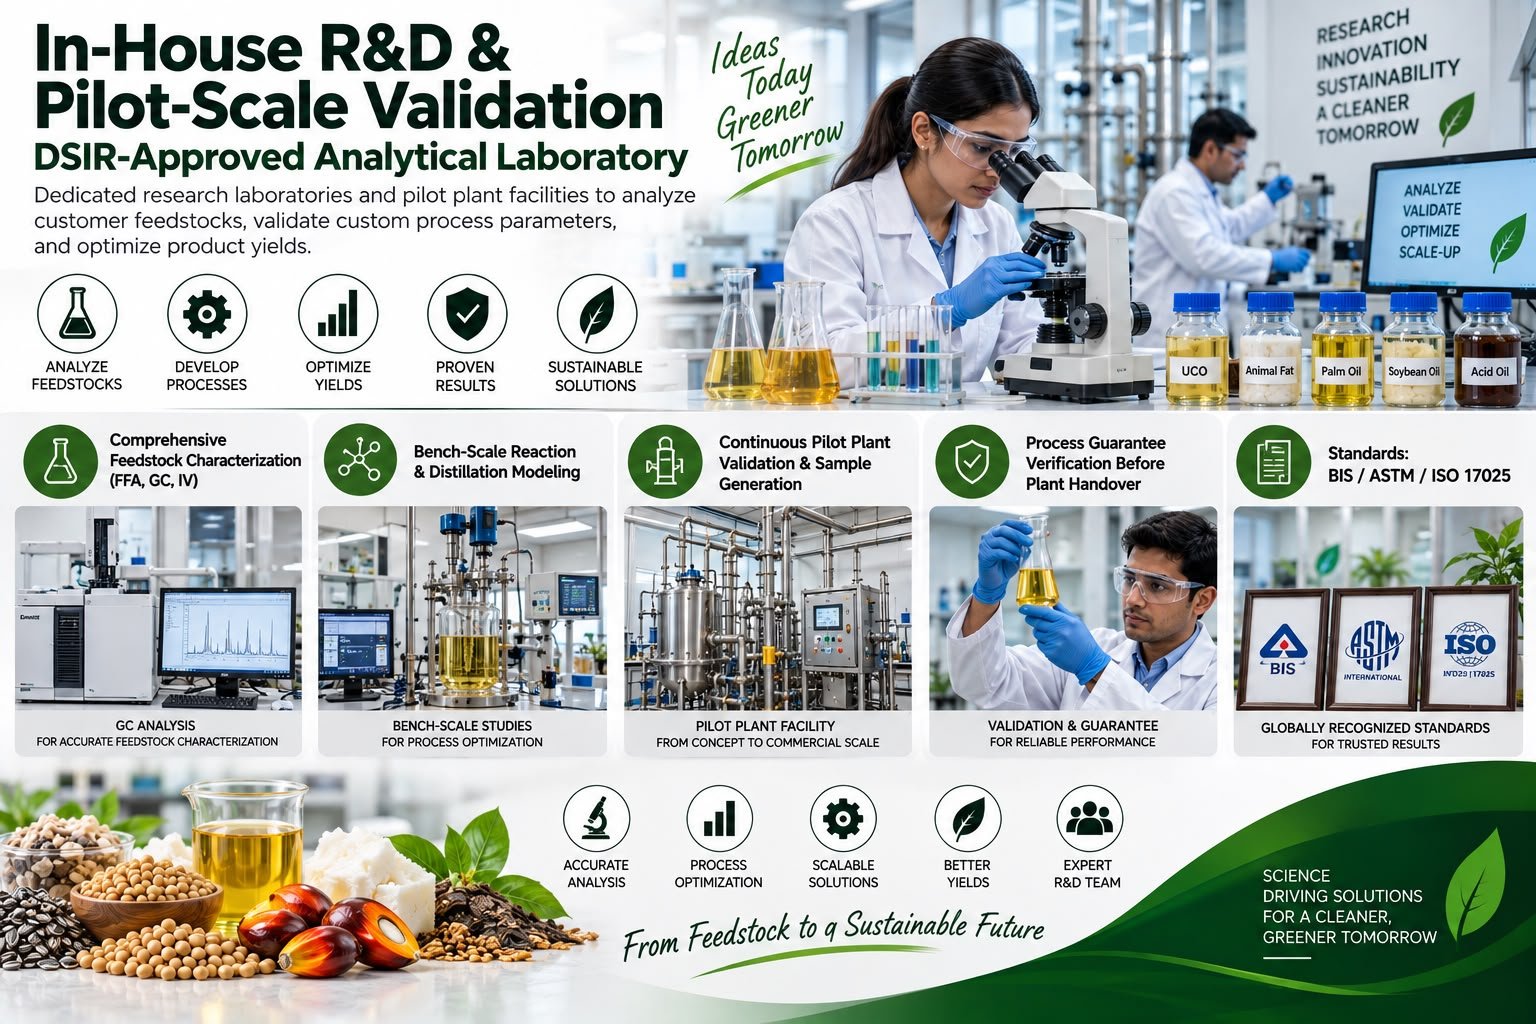
In-House R&D & Pilot-Scale Validation
Dedicated research laboratories and pilot plant facilities to analyze customer feedstocks, validate custom process parameters, and optimize product yields.