Process & Technology Infographic
Full technical schematic, unit operations, and process architecture.
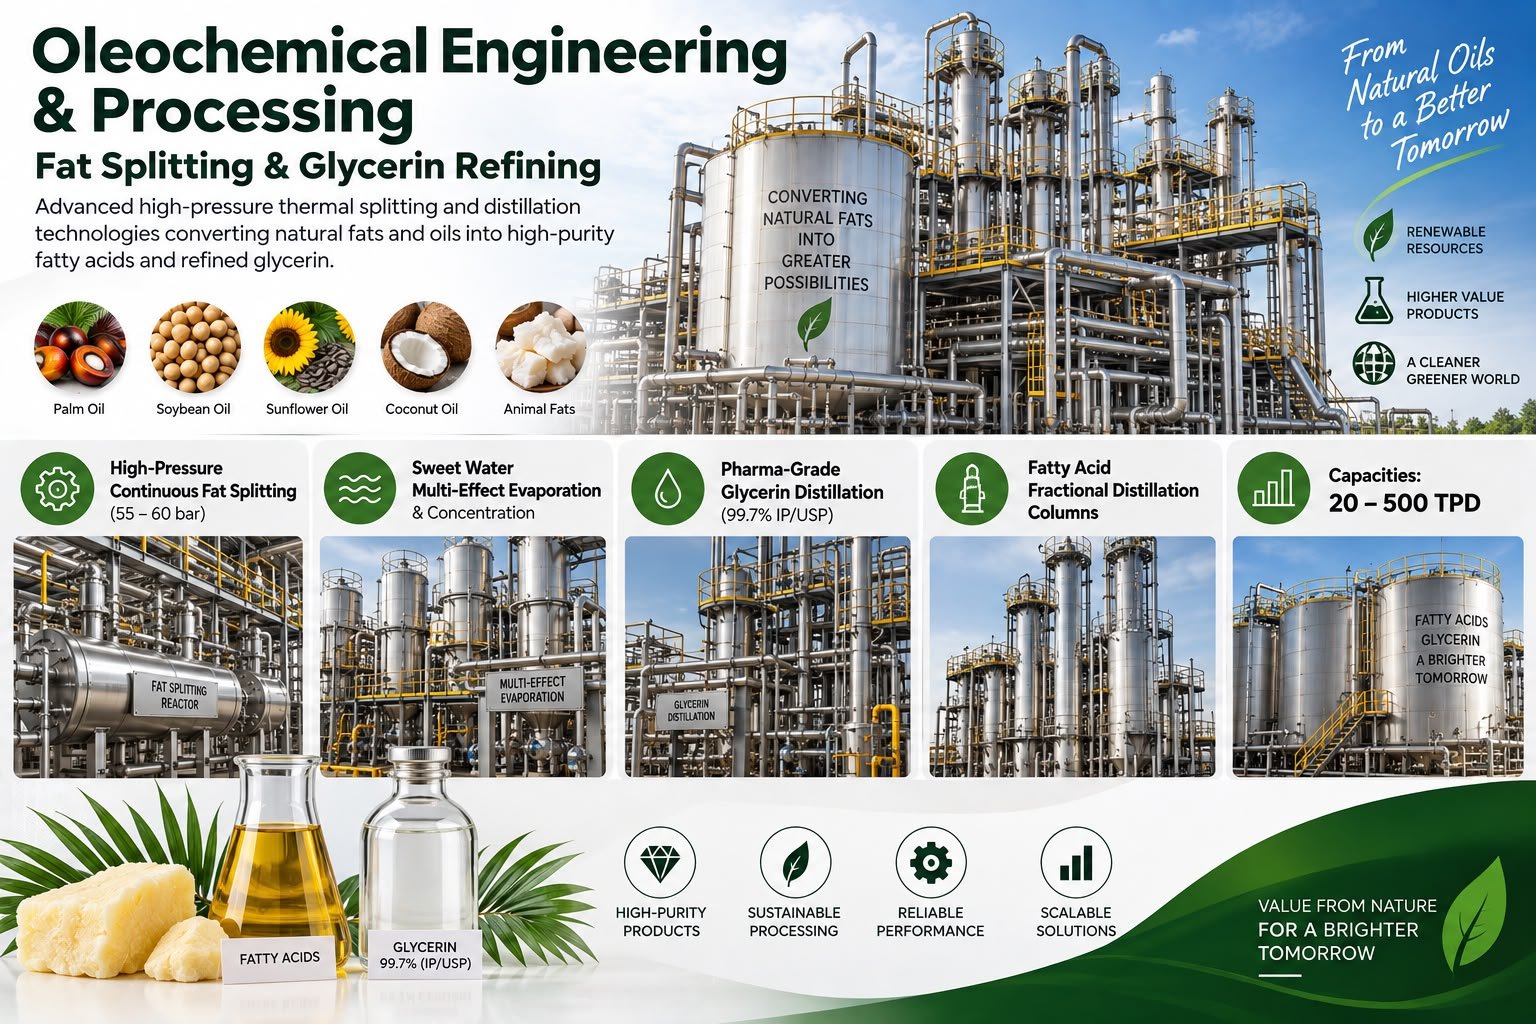
Comprehensive Plant Engineering & Technology Architecture
MAHIJA engineers turnkey oleochemical complexes for fat splitting, fatty acid fractionation, and pharmaceutical glycerin refining. Utilizing high-pressure Colgate-Emery splitting towers operating at 55–60 bar and 250–260°C without catalysts, our systems achieve split yields >99.2%. Sweet water is concentrated in falling film evaporators and refined into 99.7% pure USP/IP/BP pharma grade glycerin with full kosher and halal compliance.
Key Process Stages & Methodology
Integrated continuous engineering flow from raw feedstock preparation to final finished product output.
High-Pressure Fat Splitting Tower
Continuous counter-current splitting column operating at 55–60 bar without chemical catalyst.
Sweet Water Multi-Effect Evaporation
Triple/quadruple falling-film evaporators concentrating sweet water from 12% to 88% crude glycerin.
Crude Fatty Acid Vacuum Distillation
Structured packing distillation column with external reboilers separating pitch from light and heavy fatty acids.
Pharma-Grade Glycerine Distillation
Multi-stage vacuum distillation and activated carbon deodorization achieving 99.7% purity.
Engineered System Capabilities
Design Specifications & Performance Guarantees
| Parameter / Metric | Engineering Benchmark & Value |
|---|---|
| Capacity Range | 20 to 500 TPD |
| Splitting Degree | ≥ 99.2% Splitting Yield |
| Glycerine Purity | ≥ 99.7% IP / USP / BP Grade |
| Fatty Acid Recovery | ≥ 98.5% of theoretical yield |
| Column Metallurgy | SS316L, 317L, and high-nickel alloys for corrosive fatty acid service |
Compatible Feedstocks & Industrial Outputs
Inquire Sizing & Feasibility
Get custom mass-energy balance, civil layout, and DPR estimates.
Explore All 9 Turnkey Engineering Facilities
Solvent Extraction Systems & Technology
Complete turnkey solvent extraction plants engineered for maximum oil recovery with minimum solvent loss and lowest utility consumption.
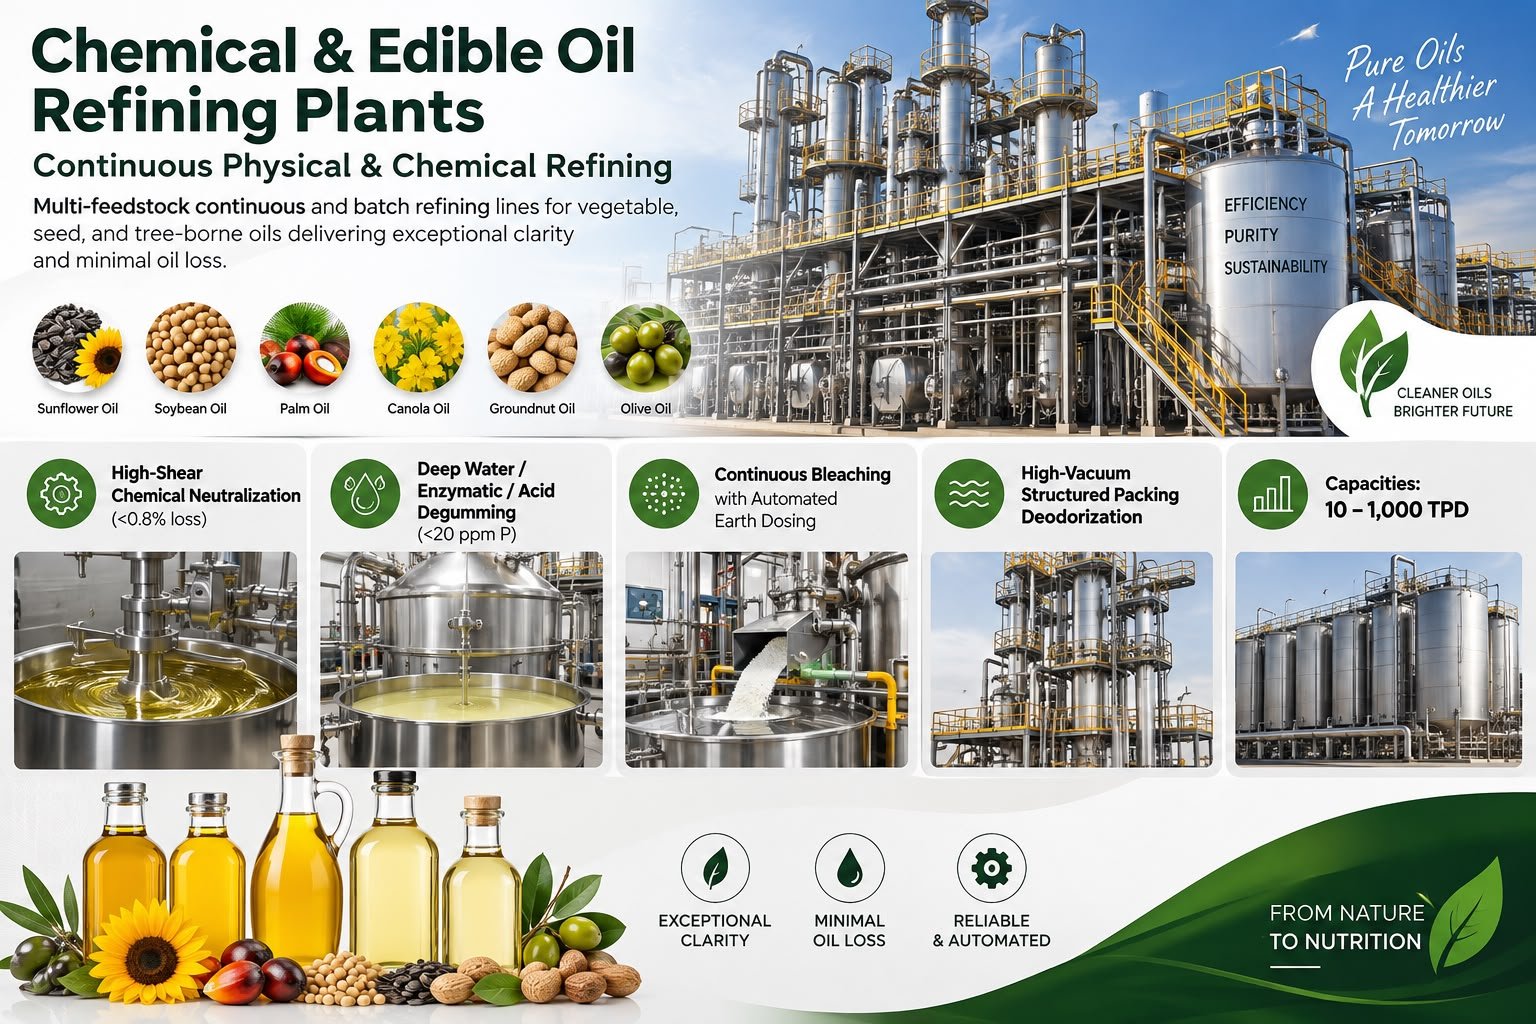
Chemical & Edible Oil Refining Plants
Multi-feedstock continuous and batch refining lines for vegetable, seed, and tree-borne oils delivering exceptional clarity and minimal oil loss.
Oleochemical Engineering & Processing
Advanced high-pressure thermal splitting and distillation technologies converting natural fats and oils into high-purity fatty acids and refined glycerin.
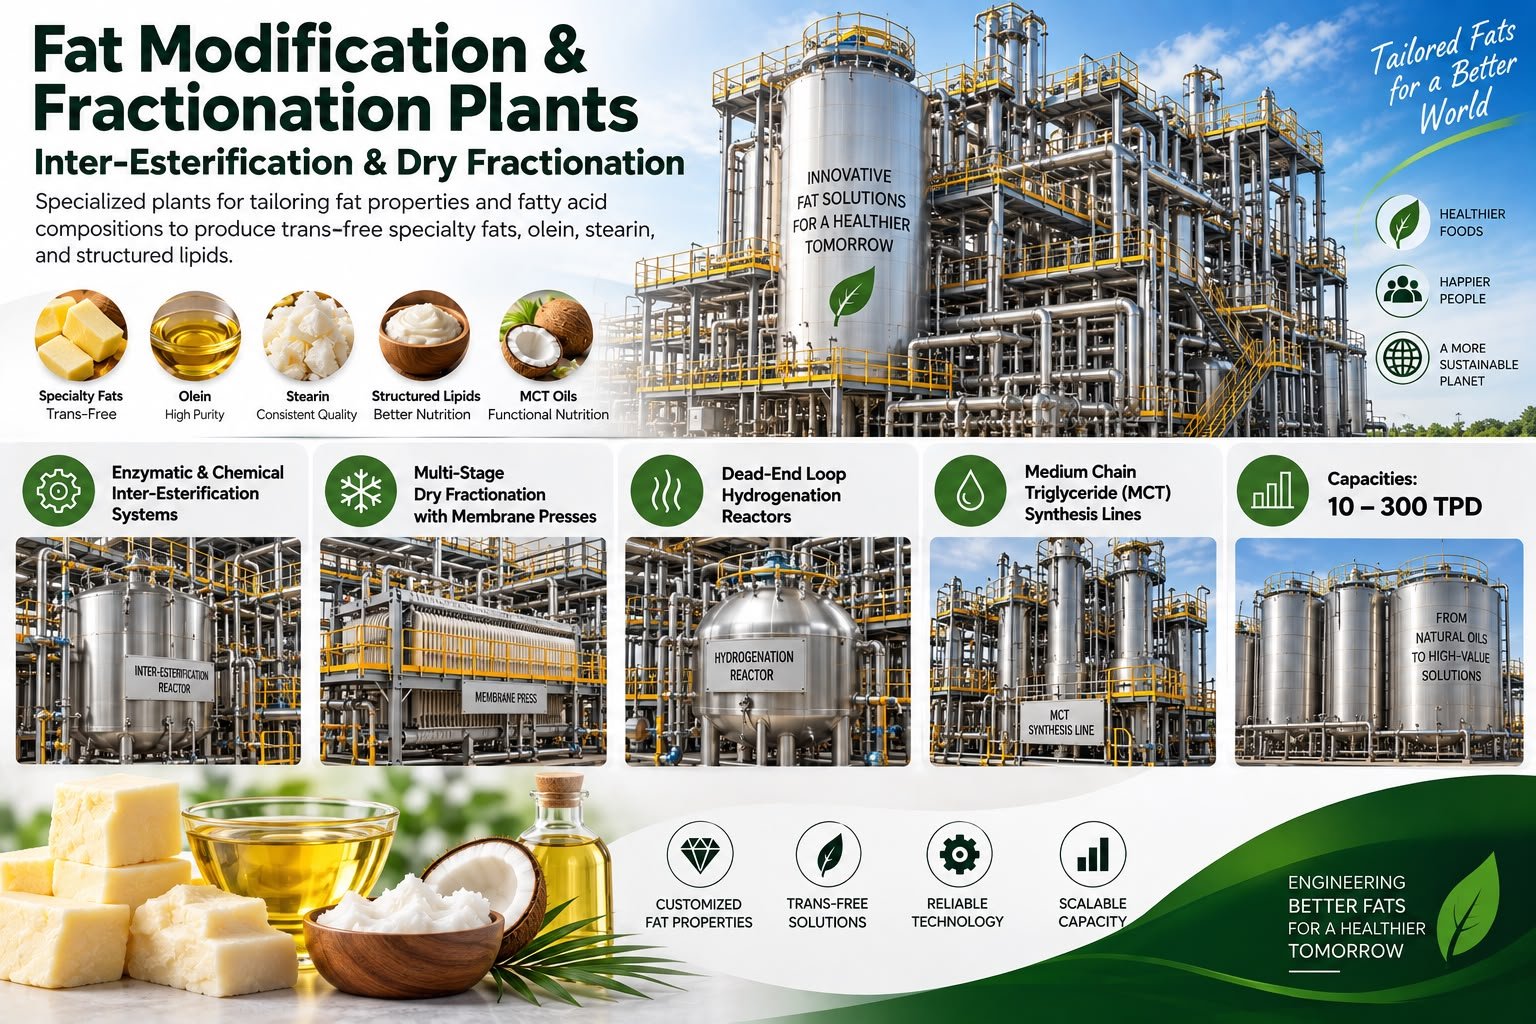
Fat Modification & Fractionation Plants
Specialized plants for tailoring fat properties and fatty acid compositions to produce trans-free specialty fats, olein, stearin, and structured lipids.
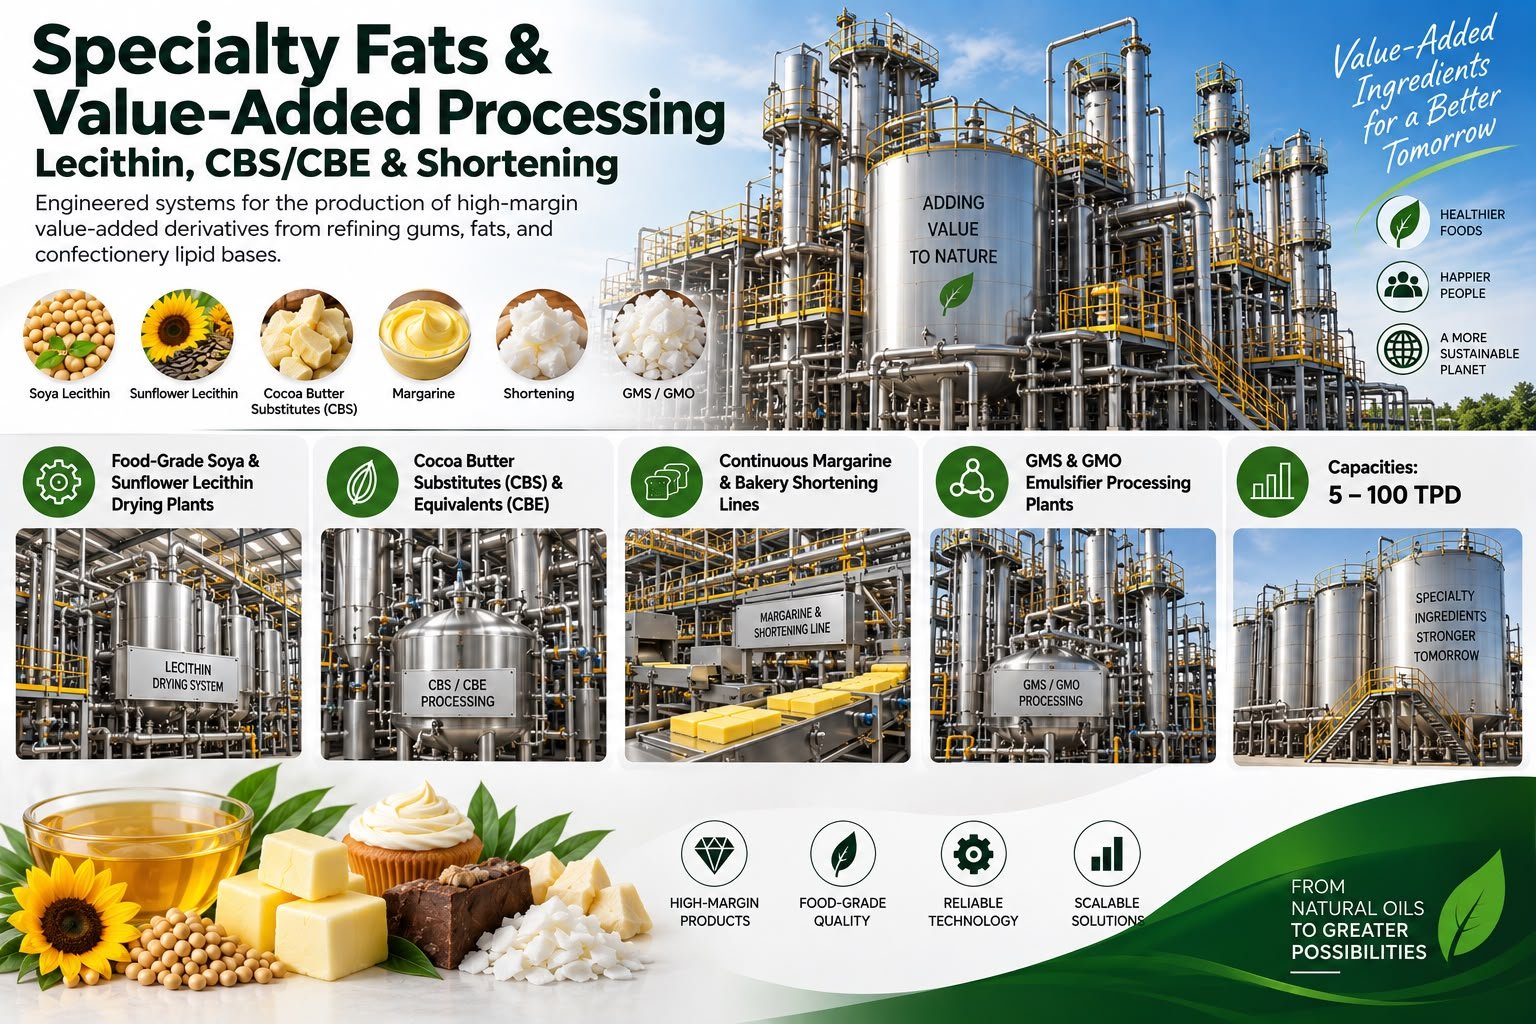
Specialty Fats & Value-Added Processing
Engineered systems for the production of high-margin value-added derivatives from refining gums, fats, and confectionery lipid bases.
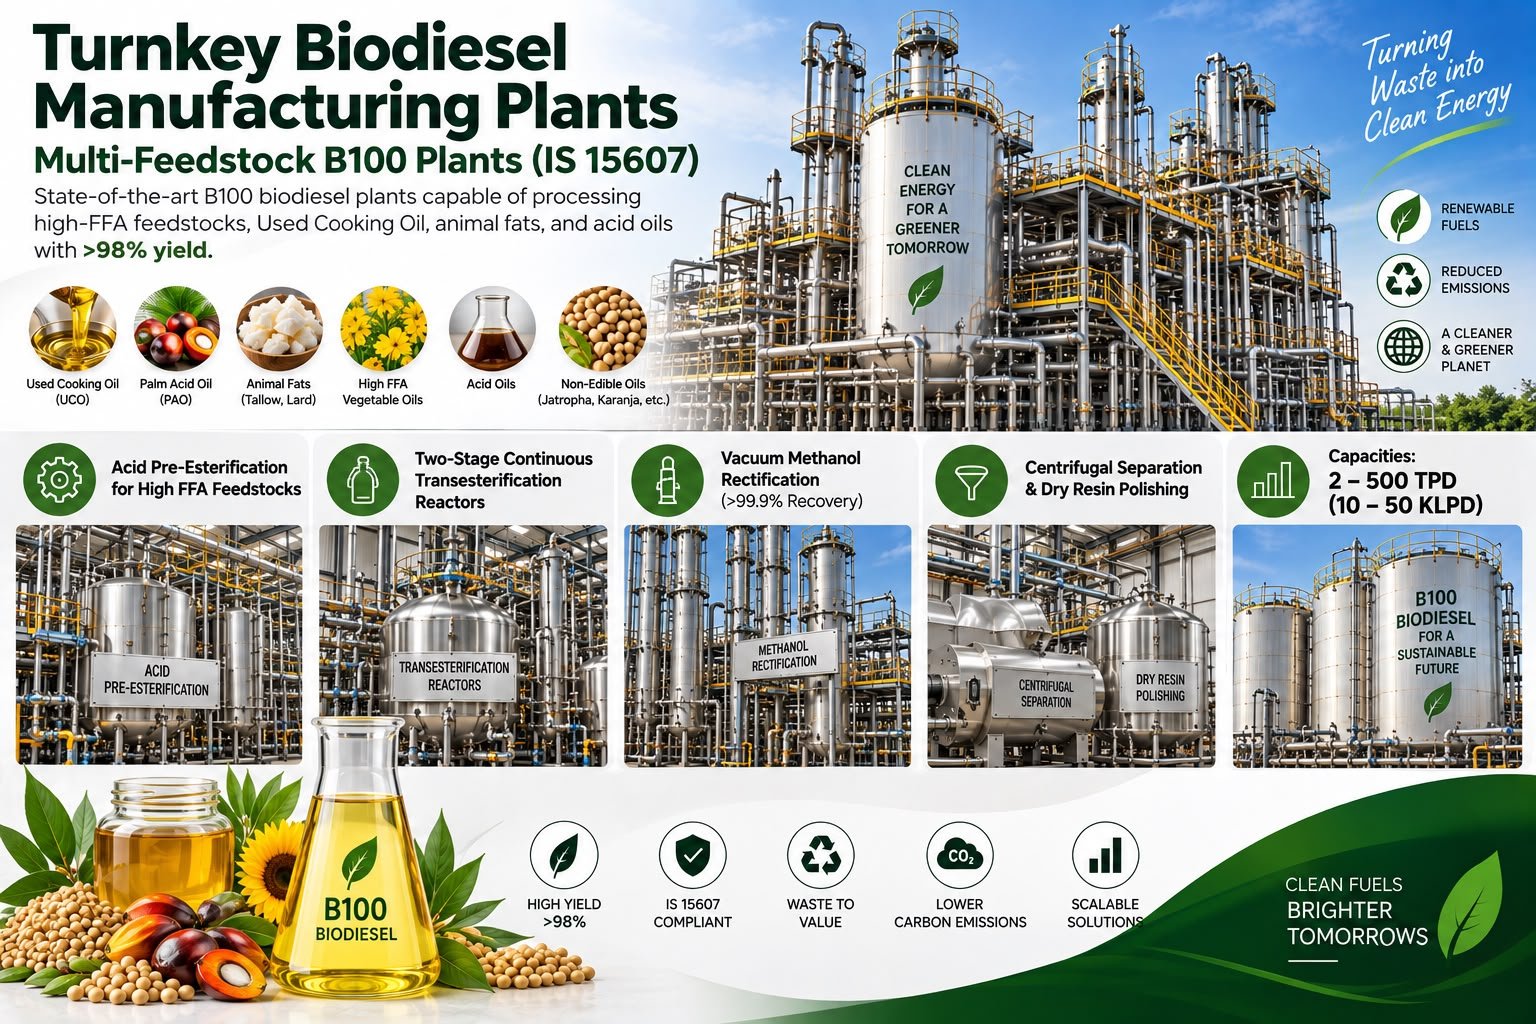
Turnkey Biodiesel Manufacturing Plants
State-of-the-art B100 biodiesel plants capable of processing high-FFA feedstocks, Used Cooking Oil, animal fats, and acid oils with >98% yield.
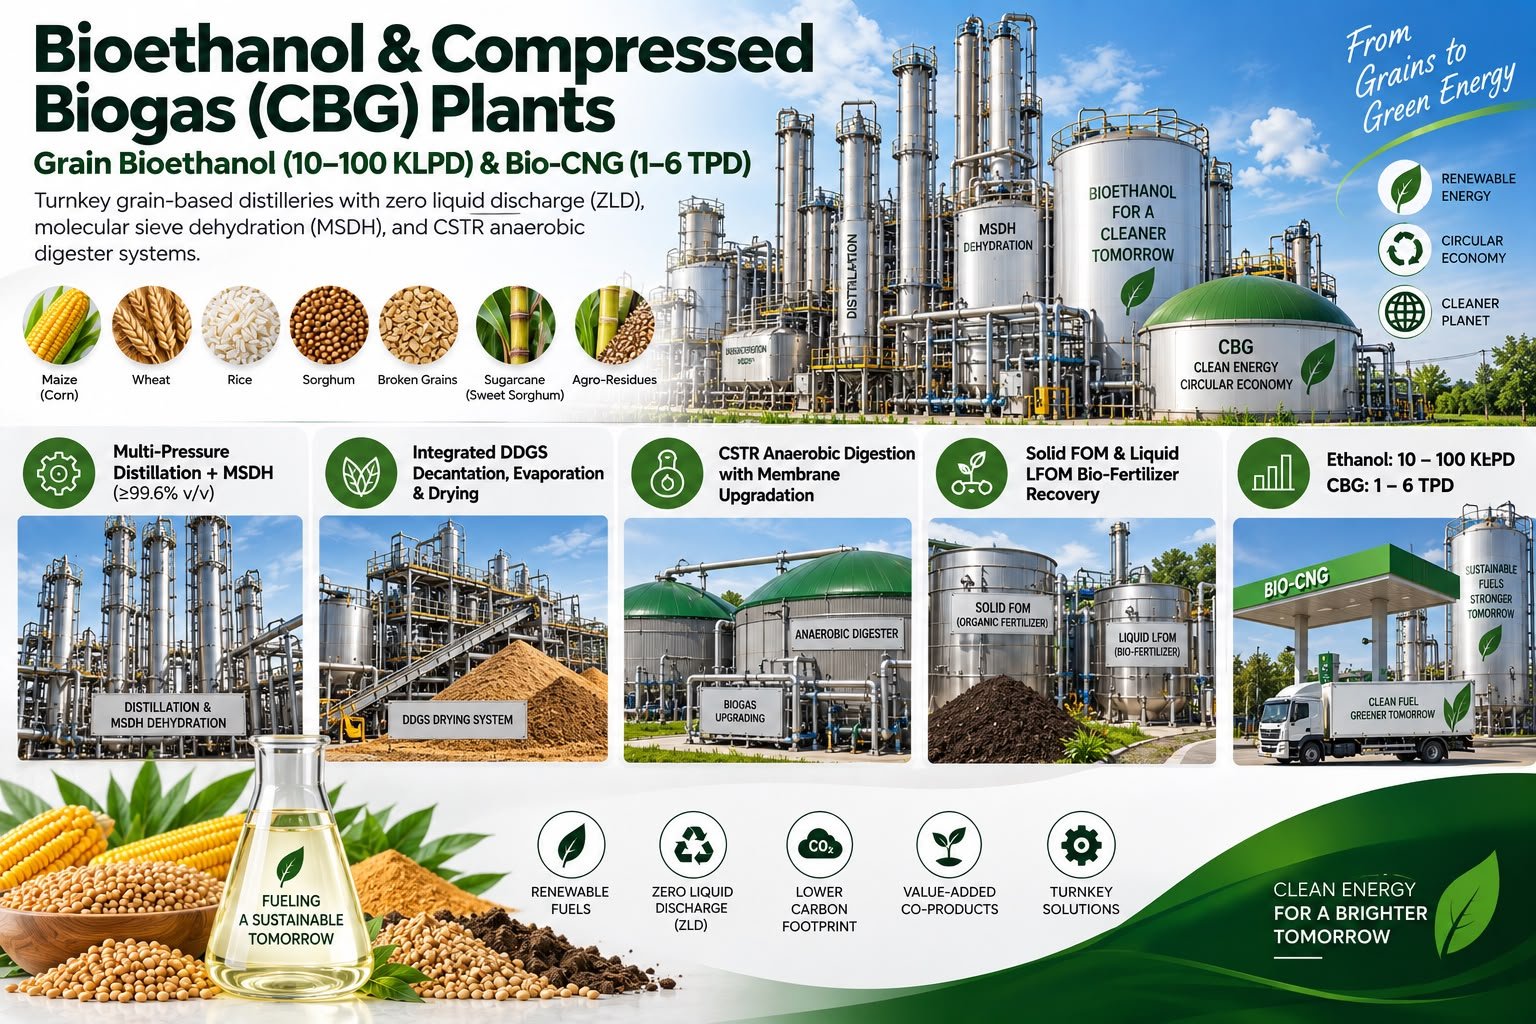
Bioethanol & Compressed Biogas (CBG) Plants
Turnkey grain-based distilleries with zero liquid discharge (ZLD), molecular sieve dehydration (MSDH), and CSTR anaerobic digester systems.
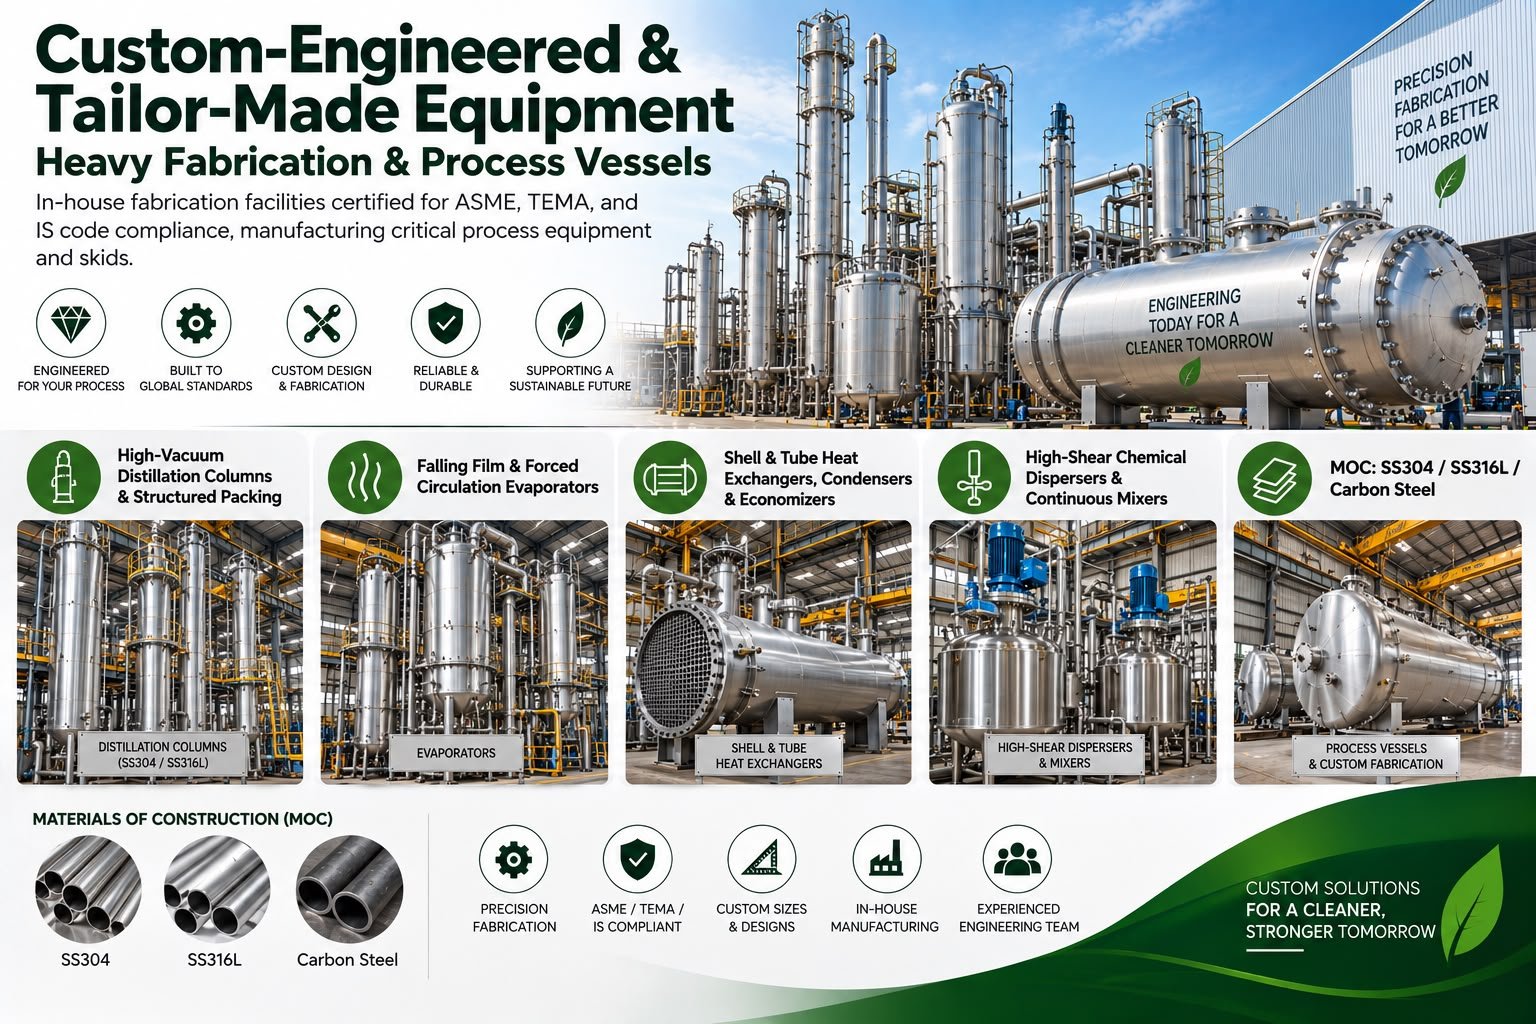
Custom-Engineered & Tailor-Made Equipment
In-house fabrication facilities certified for ASME, TEMA, and IS code compliance, manufacturing critical process equipment and skids.
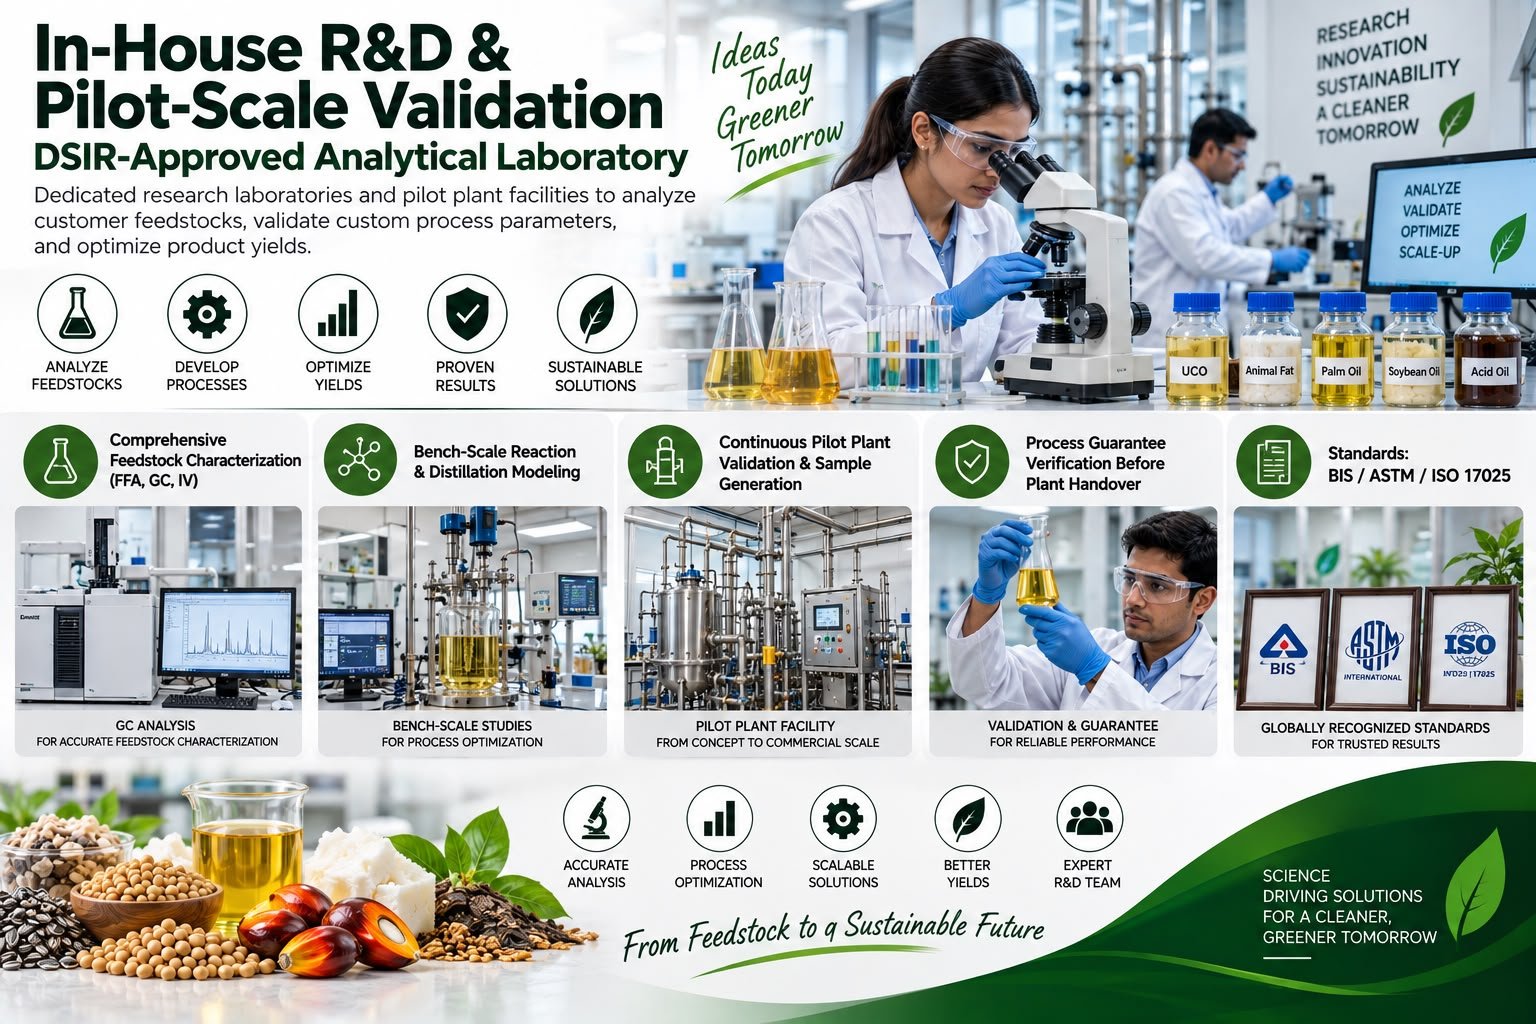
In-House R&D & Pilot-Scale Validation
Dedicated research laboratories and pilot plant facilities to analyze customer feedstocks, validate custom process parameters, and optimize product yields.