Process & Technology Infographic
Full technical schematic, unit operations, and process architecture.
Comprehensive Plant Engineering & Technology Architecture
MAHIJA delivers high-efficiency continuous solvent extraction plants engineered for diverse oilseeds and agro-biomass including Soybean, Rapeseed/Mustard, Rice Bran, Sunflower, Cottonseed, and Palm Kernel Cake. Our extraction systems combine robust heavy-duty prep machinery with state-of-the-art multi-stage counter-current extractors, low-temperature DTDC desolventization, and closed-loop vent recovery systems to guarantee residual oil levels below 0.5% and hexane losses under 1.2 kg/ton of processed material.
Key Process Stages & Methodology
Integrated continuous engineering flow from raw feedstock preparation to final finished product output.
Seed Preparatory & Conditioning
High-capacity magnetic separation, destoning, cracking, conditioning, and hydraulic flaking rolls for uniform seed cell rupture.
Counter-Current Hexane Extraction
Continuous chain-type loop or stationary screen Rotocel extractors with multi-stage miscella spraying and deep bed washing.
DTDC (Desolventizing, Toasting, Drying & Cooling)
Integrated multi-tray DTDC vessel with indirect/direct steam injection to recover hexane and preserve meal protein solubility.
Miscella Distillation & Vacuum Stripping
Energy-conserving multi-effect evaporators utilizing DTDC flash vapor, finished in high-vacuum packed stripping columns.
Mineral Oil Vent Absorption (MOS)
Closed-cycle mineral oil scrubbing system capturing 99.8% of vent gases before ambient discharge.
Engineered System Capabilities
Design Specifications & Performance Guarantees
| Parameter / Metric | Engineering Benchmark & Value |
|---|---|
| Capacity Range | 50 to 2,000 TPD (Single / Multi-Seed) |
| Residual Oil in Meal | < 0.5% to 0.8% (Feedstock dependent) |
| Hexane Consumption | 1.0 – 1.8 Liters per ton of processed seed |
| Steam Consumption | 180 – 240 kg per ton of seed |
| Power Consumption | 22 – 28 kWh per ton of seed |
| Contact Metallurgy (MOC) | IS 2062 Grade B / SS304 / SS316L for critical zones |
| Automation & Control | PLC / SCADA with fail-safe interlocks & vapor detectors |
Compatible Feedstocks & Industrial Outputs
Inquire Sizing & Feasibility
Get custom mass-energy balance, civil layout, and DPR estimates.
Explore All 9 Turnkey Engineering Facilities
Solvent Extraction Systems & Technology
Complete turnkey solvent extraction plants engineered for maximum oil recovery with minimum solvent loss and lowest utility consumption.
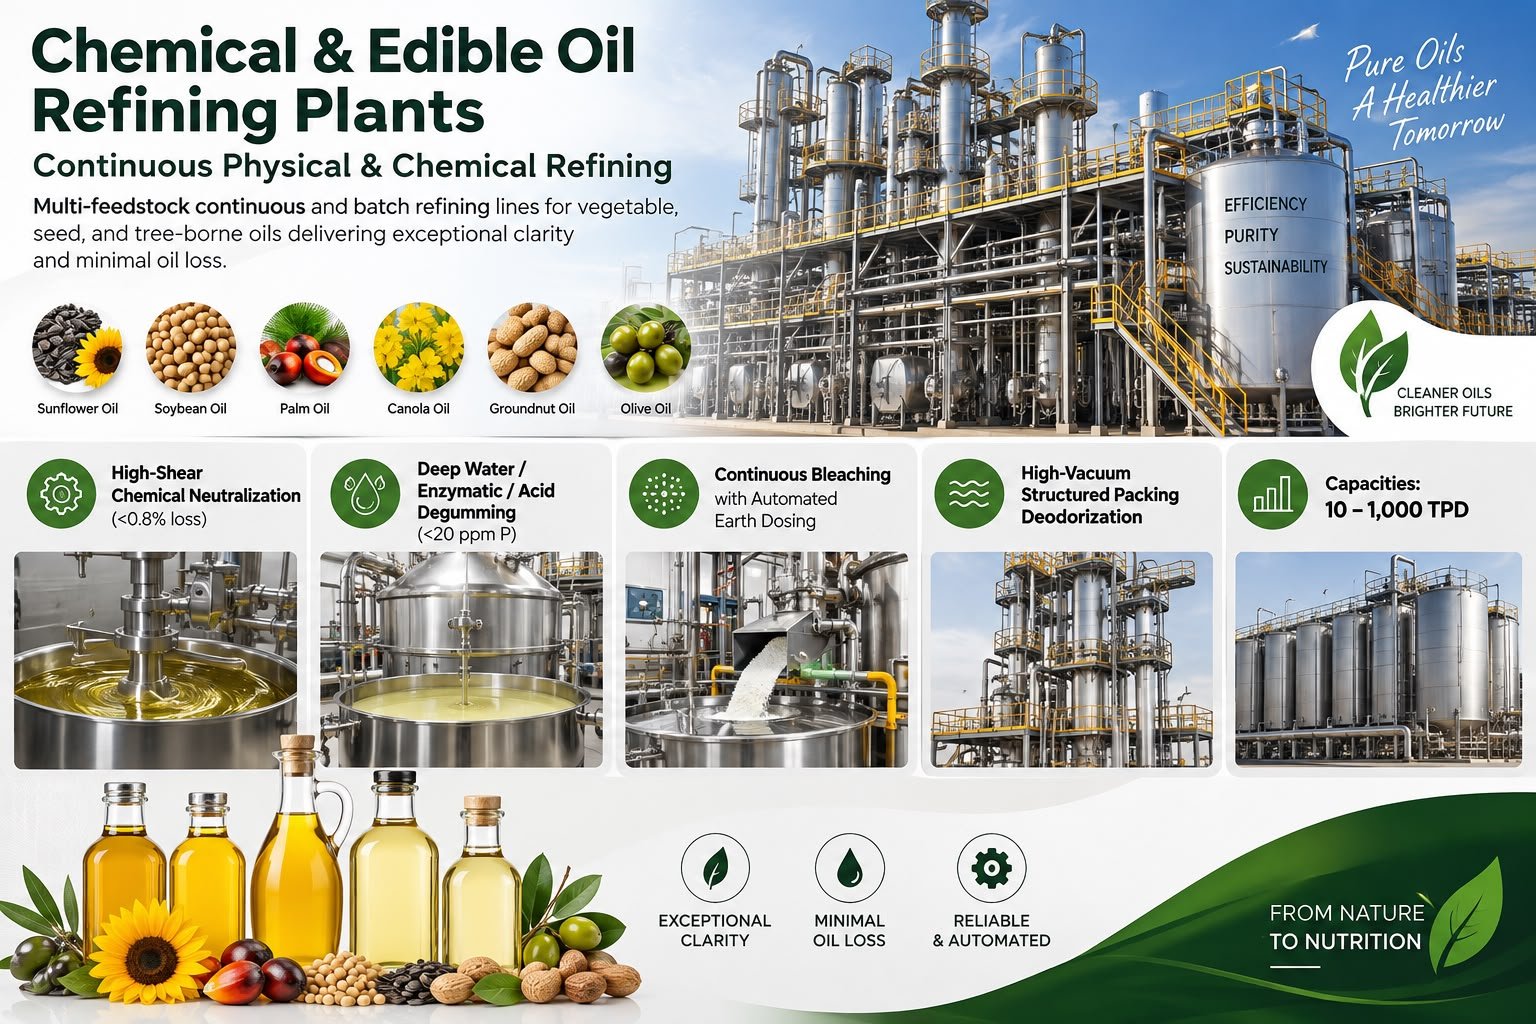
Chemical & Edible Oil Refining Plants
Multi-feedstock continuous and batch refining lines for vegetable, seed, and tree-borne oils delivering exceptional clarity and minimal oil loss.
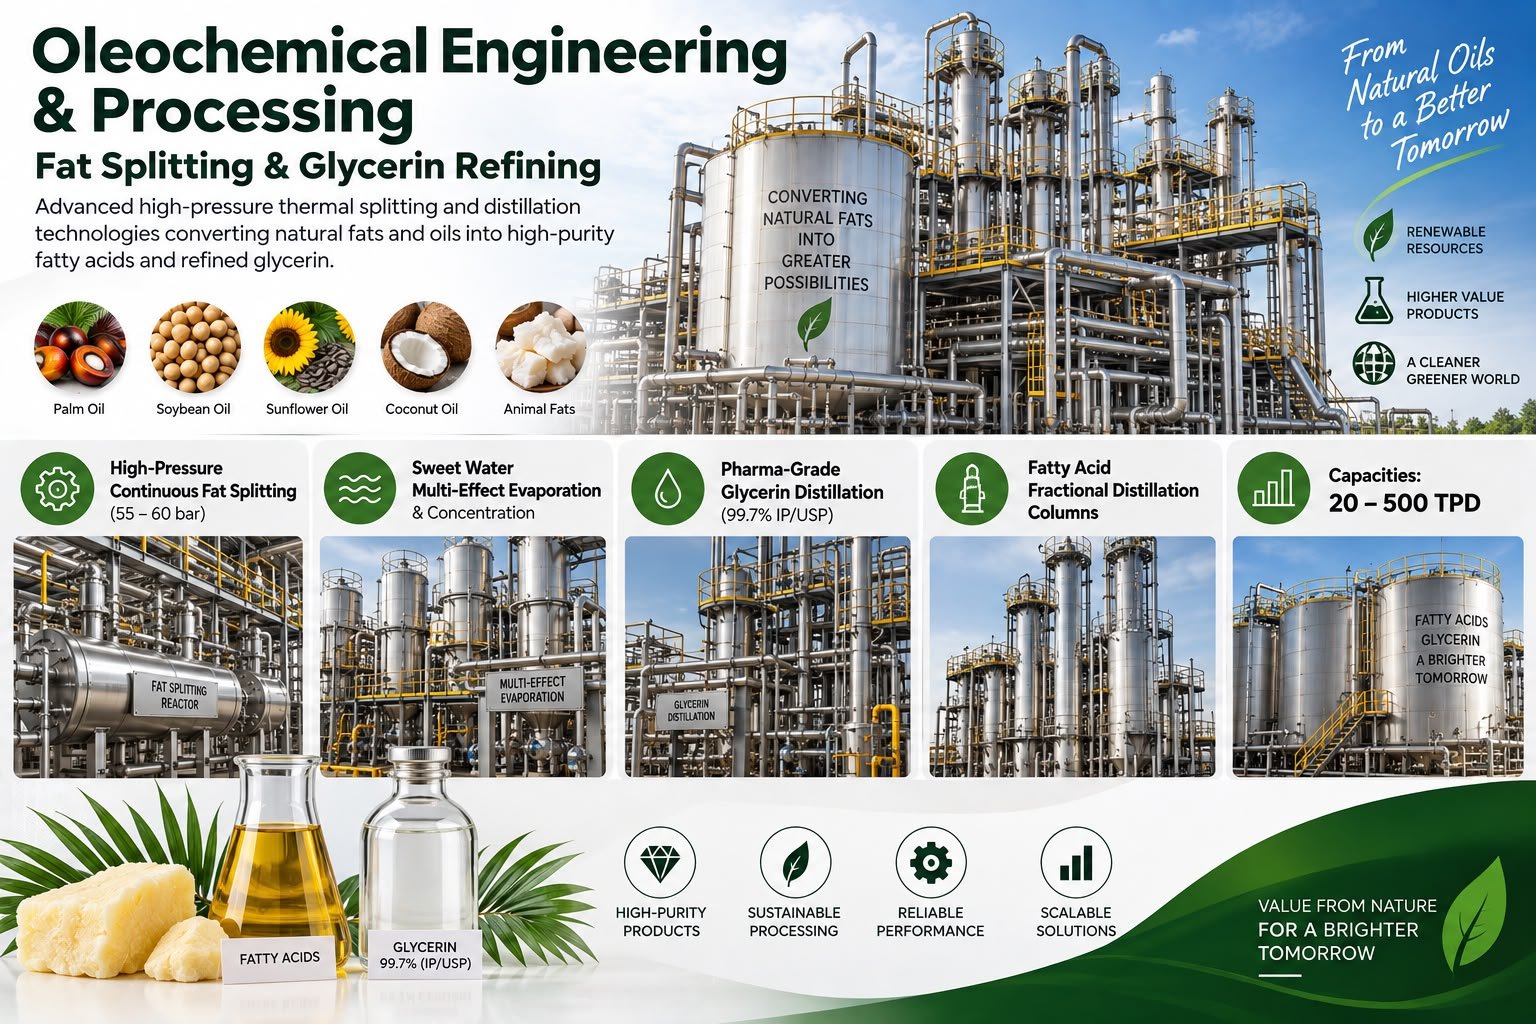
Oleochemical Engineering & Processing
Advanced high-pressure thermal splitting and distillation technologies converting natural fats and oils into high-purity fatty acids and refined glycerin.
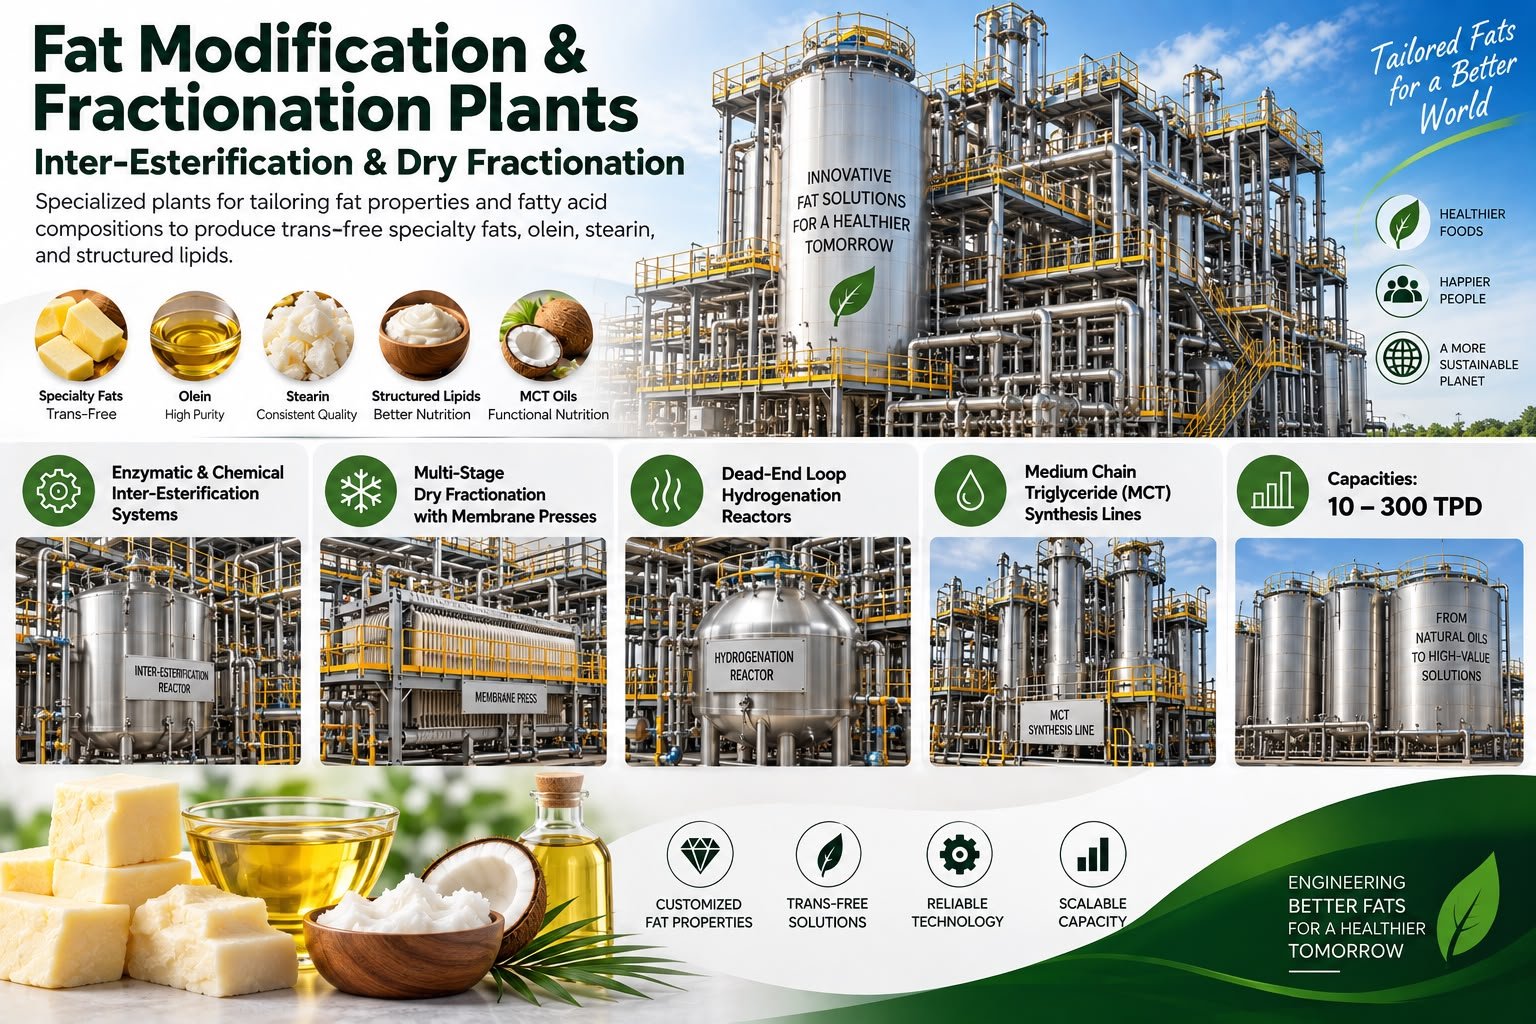
Fat Modification & Fractionation Plants
Specialized plants for tailoring fat properties and fatty acid compositions to produce trans-free specialty fats, olein, stearin, and structured lipids.
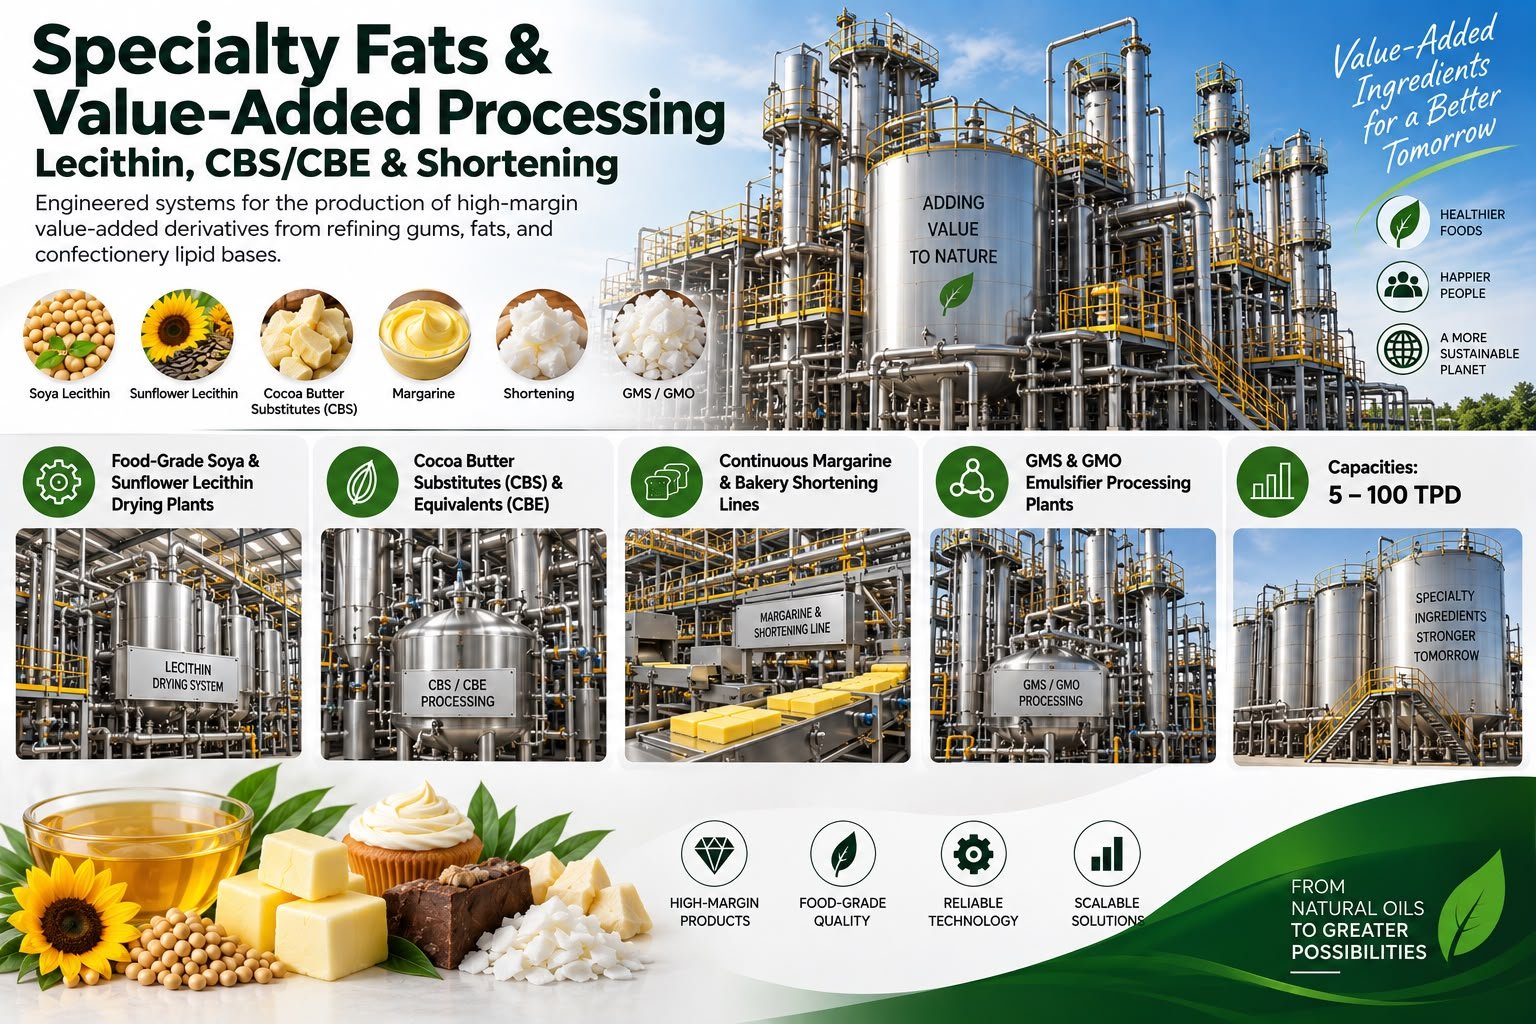
Specialty Fats & Value-Added Processing
Engineered systems for the production of high-margin value-added derivatives from refining gums, fats, and confectionery lipid bases.
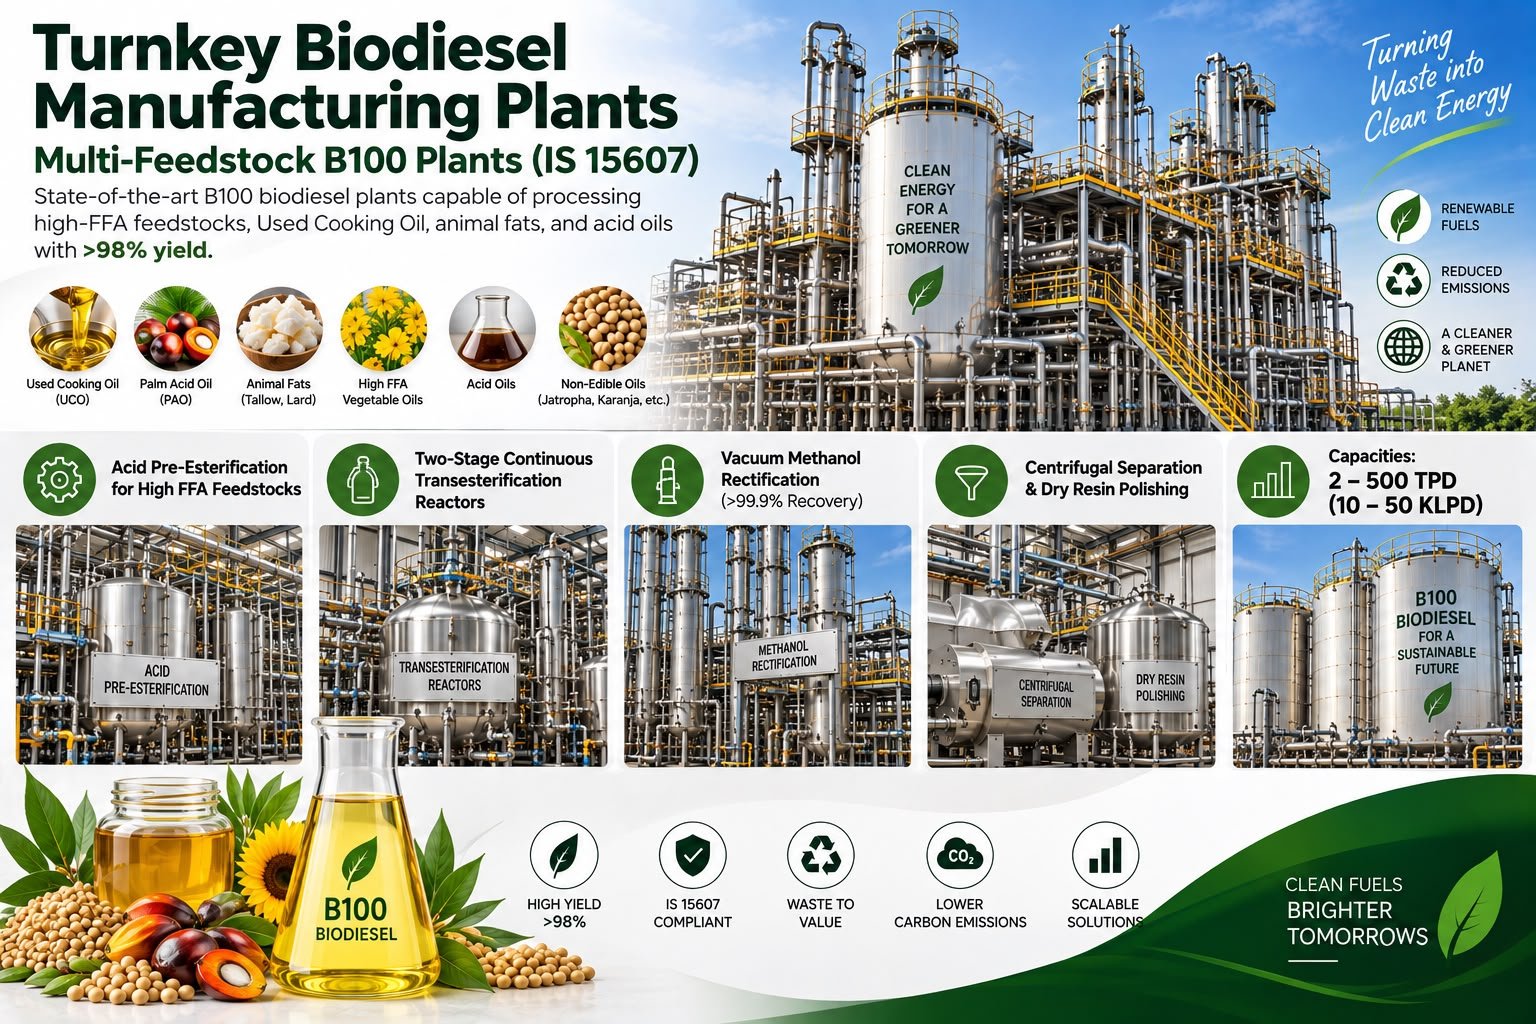
Turnkey Biodiesel Manufacturing Plants
State-of-the-art B100 biodiesel plants capable of processing high-FFA feedstocks, Used Cooking Oil, animal fats, and acid oils with >98% yield.
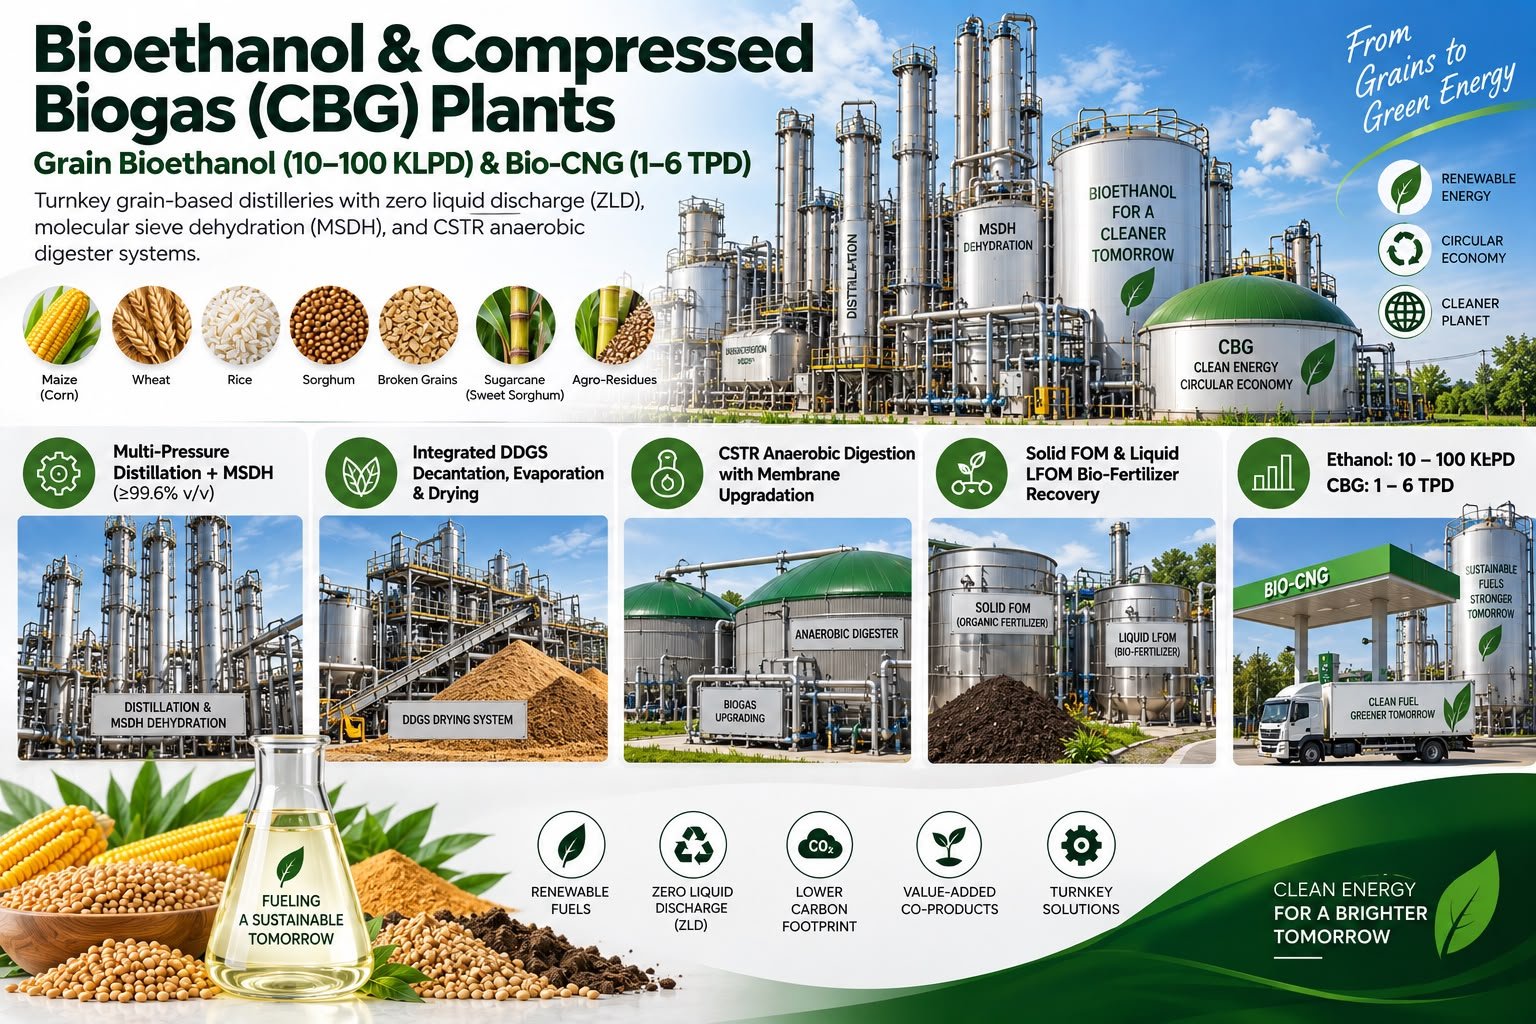
Bioethanol & Compressed Biogas (CBG) Plants
Turnkey grain-based distilleries with zero liquid discharge (ZLD), molecular sieve dehydration (MSDH), and CSTR anaerobic digester systems.
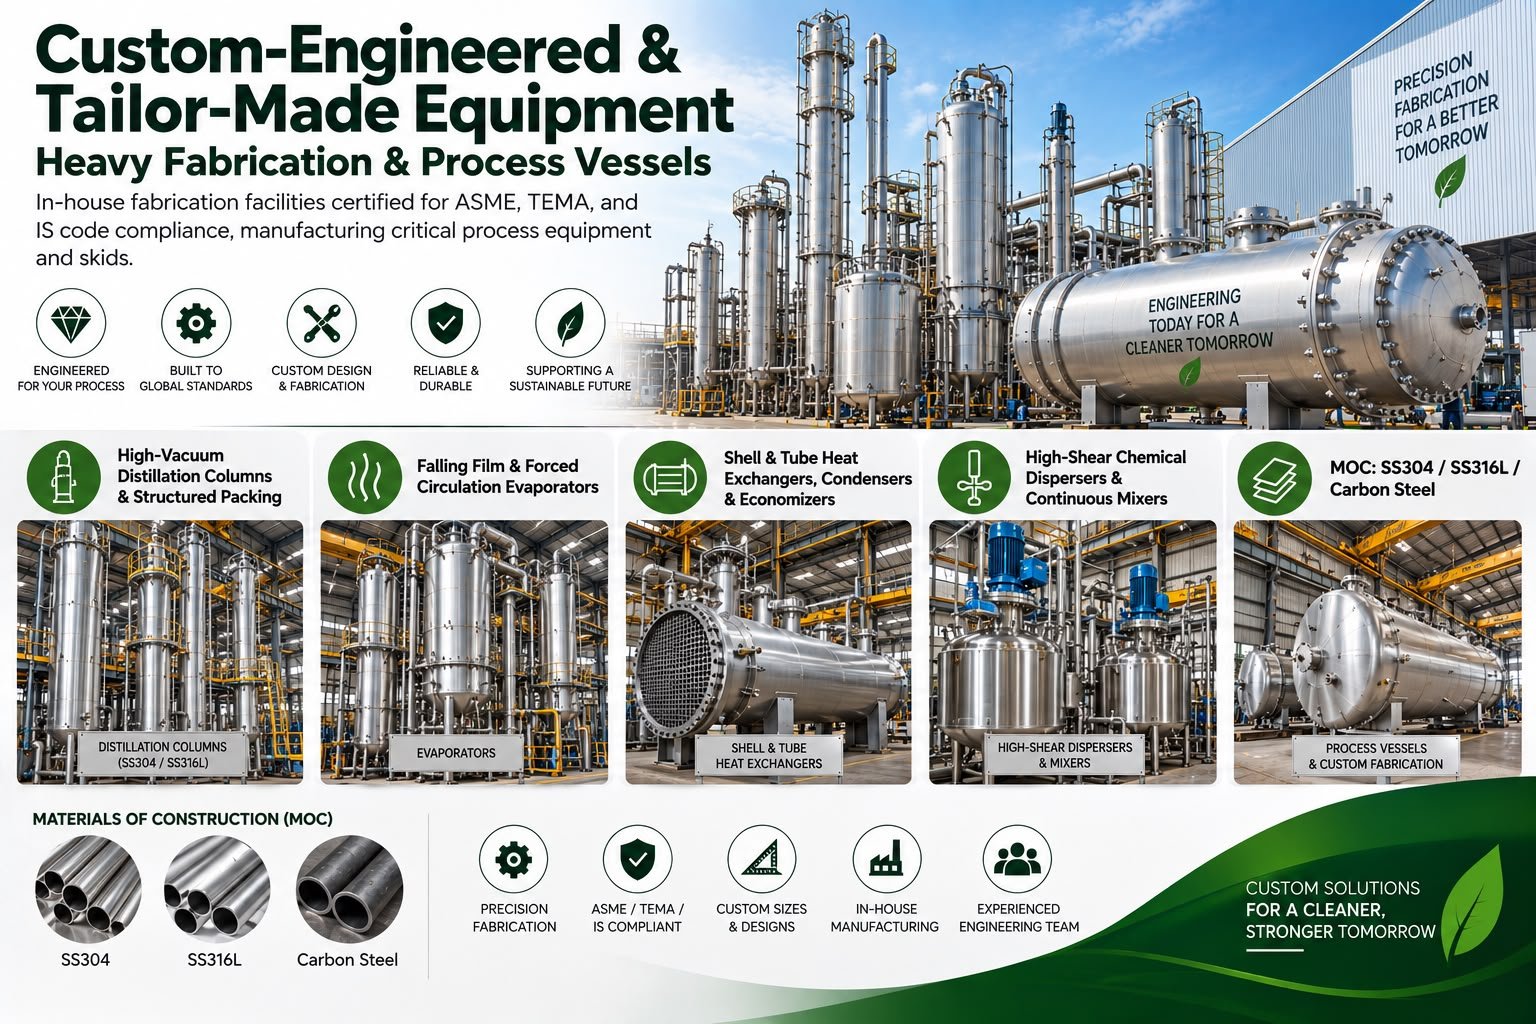
Custom-Engineered & Tailor-Made Equipment
In-house fabrication facilities certified for ASME, TEMA, and IS code compliance, manufacturing critical process equipment and skids.
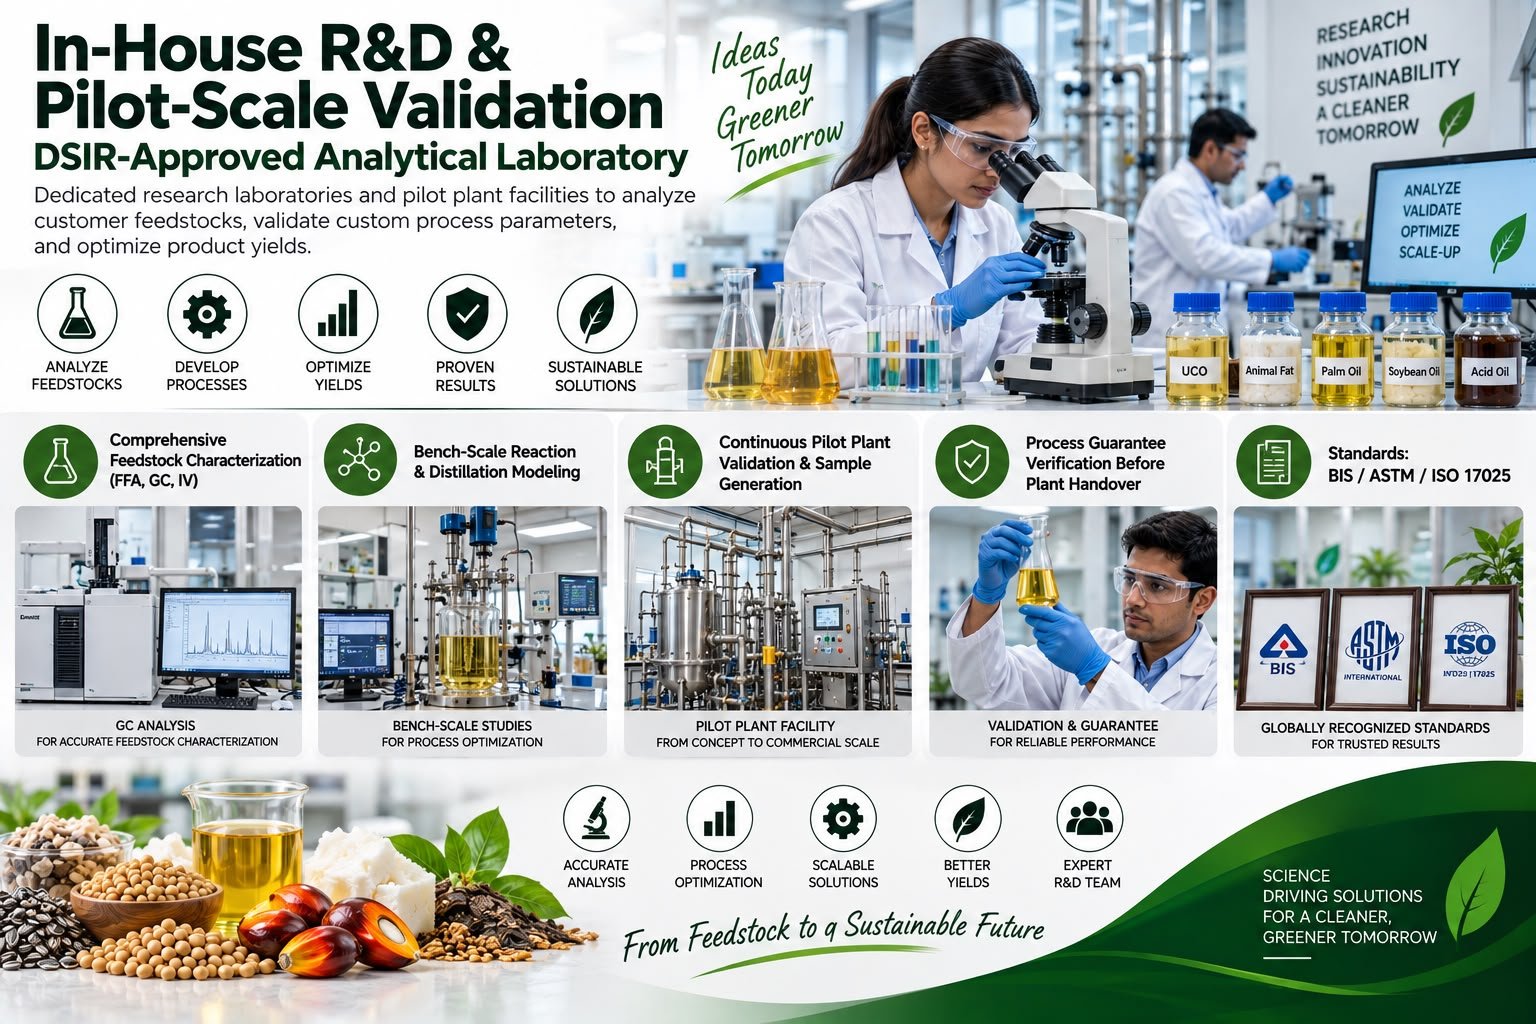
In-House R&D & Pilot-Scale Validation
Dedicated research laboratories and pilot plant facilities to analyze customer feedstocks, validate custom process parameters, and optimize product yields.